Общий каталог SGS 2018 - страница 113
Навигация
 Каталог SGS шестизубые фрезы T-carb
 Каталог SGS микро инструмент 2021
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2015 на русском
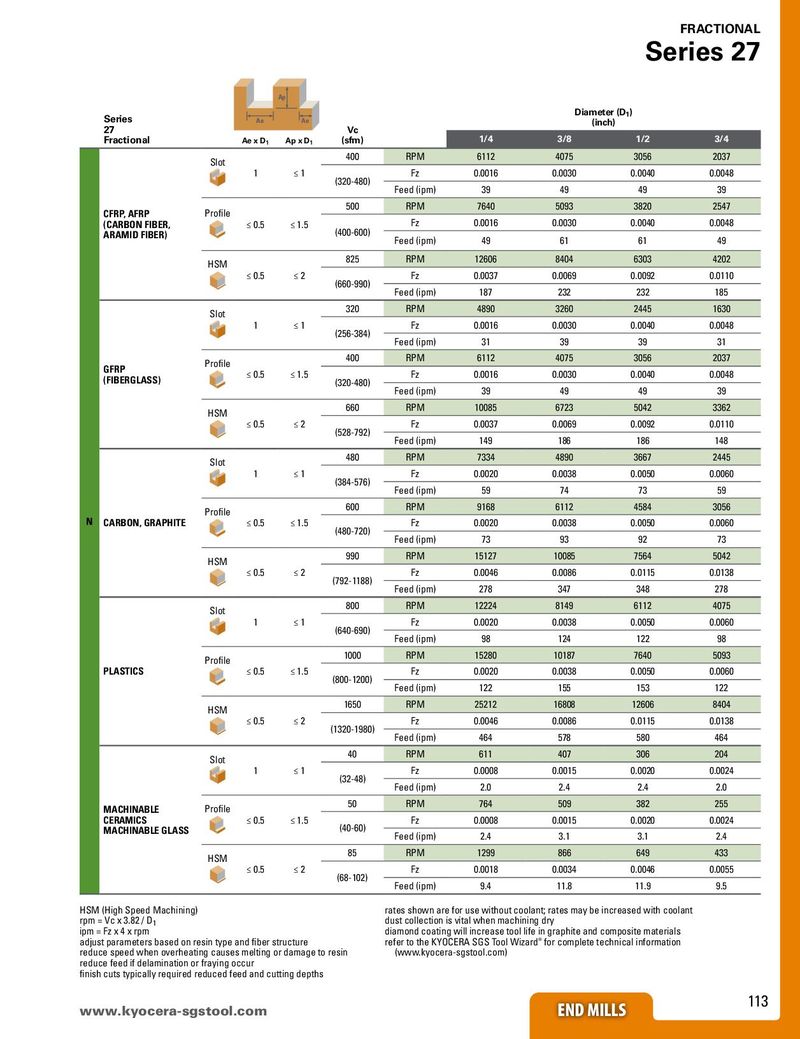
| Series 27 | Ae | Ap Ae | Vc | Diame (in | ter (D1) ch) | ||||
| Fractional | Ae x D1 | Ap x D1 | (sfm) | 1/4 | 3/8 | 1/2 | 3/4 | ||
| Slot | 400 | RPM | 6112 | 4075 | 3056 | 2037 | |||
| 1 | ≤ 1 | Fz | 0.0016 | 0.0030 | 0.0040 | 0.0048 | |||
| (320-480) | Feed (ipm) | 39 | 49 | 49 | 39 | ||||
| CFRP AFRP | Profile | 500 | RPM | 7640 | 5093 | 3820 | 2547 | ||
| , (CARBON FIBER, | ≤ 0.5 | ≤ 1.5 | Fz | 0.0016 | 0.0030 | 0.0040 | 0.0048 | ||
| ARAMID FIBER) | (400-600) | Feed (ipm) | 49 | 61 | 61 | 49 | |||
| HSM | 825 | RPM | 12606 | 8404 | 6303 | 4202 | |||
| ≤ 0.5 | ≤ 2 | (660-990) | Fz | 0.0037 | 0.0069 | 0.0092 | 0.0110 | ||
| Feed (ipm) | 187 | 232 | 232 | 185 | |||||
| Slot | 320 | RPM | 4890 | 3260 | 2445 | 1630 | |||
| 1 | ≤ 1 | Fz | 0.0016 | 0.0030 | 0.0040 | 0.0048 | |||
| (256-384) | Feed (ipm) | 31 | 39 | 39 | 31 | ||||
| Profile | 400 | RPM | 6112 | 4075 | 3056 | 2037 | |||
| GFRP (FIBERGLASS) | ≤ 0.5 | ≤ 1.5 | (320-480) | Fz | 0.0016 | 0.0030 | 0.0040 | 0.0048 | |
| Feed (ipm) | 39 | 49 | 49 | 39 | |||||
| HSM | 660 | RPM | 10085 | 6723 | 5042 | 3362 | |||
| ≤ 0.5 | ≤ 2 | Fz | 0.0037 | 0.0069 | 0.0092 | 0.0110 | |||
| (528-792) | Feed (ipm) | 149 | 186 | 186 | 148 | ||||
| Slot | 480 | RPM | 7334 | 4890 | 3667 | 2445 | |||
| 1 | ≤ 1 | (384576) | Fz | 0.0020 | 0.0038 | 0.0050 | 0.0060 | ||
| - | Feed (ipm) | 59 | 74 | 73 | 59 | ||||
| Profile | 600 | RPM | 9168 | 6112 | 4584 | 3056 | |||
| N CARBON, GRAPHITE | ≤ 0.5 | ≤ 1.5 | (480720) | Fz | 0.0020 | 0.0038 | 0.0050 | 0.0060 | |
| - | Feed (ipm) | 73 | 93 | 92 | 73 | ||||
| HSM | 990 | RPM | 15127 | 10085 | 7564 | 5042 | |||
| ≤ 0.5 | ≤ 2 | (792-1188) | Fz | 0.0046 | 0.0086 | 0.0115 | 0.0138 | ||
| Feed (ipm) | 278 | 347 | 348 | 278 | |||||
| Slot | 800 | RPM | 12224 | 8149 | 6112 | 4075 | |||
| 1 | ≤ 1 | (640-690) | Fz | 0.0020 | 0.0038 | 0.0050 | 0.0060 | ||
| Feed (ipm) | 98 | 124 | 122 | 98 | |||||
| Profile | 1000 | RPM | 15280 | 10187 | 7640 | 5093 | |||
| PLASTICS | ≤ 0.5 | ≤ 1.5 | 8001200 | Fz | 0.0020 | 0.0038 | 0.0050 | 0.0060 | |
| (-) | Feed (ipm) | 122 | 155 | 153 | 122 | ||||
| HSM | 1650 | RPM | 25212 | 16808 | 12606 | 8404 | |||
| ≤ 0.5 | ≤ 2 | Fz | 0.0046 | 0.0086 | 0.0115 | 0.0138 | |||
| (1320-1980) | Feed (ipm) | 464 | 578 | 580 | 464 | ||||
| Slot | 40 | RPM | 611 | 407 | 306 | 204 | |||
| 1 | ≤ 1 | Fz | 0.0008 | 0.0015 | 0.0020 | 0.0024 | |||
| (32-48) | Feed (ipm) | 2.0 | 2.4 | 2.4 | 2.0 | ||||
| MACHINABLE | Profile | 50 | RPM | 764 | 509 | 382 | 255 | ||
| CERAMICS | ≤ 0.5 | ≤ 1.5 | Fz | 0.0008 | 0.0015 | 0.0020 | 0.0024 | ||
| MACHINABLE GLASS | (40-60) | Feed (ipm) | 2.4 | 3.1 | 3.1 | 2.4 | |||
| HSM | 85 | RPM | 1299 | 866 | 649 | 433 | |||
| ≤ 0.5 | ≤ 2 | Fz | 0.0018 | 0.0034 | 0.0046 | 0.0055 | |||
| (68-102) | Feed (ipm) | 9.4 | 11.8 | 11.9 | 9.5 |
| HSM (High Speed Machining) | rates shown are for use without coolant; rates may be increased with coolant |
| rpm = Vc x 3.82 / D | dust collection is vital when machining dry |
| 1 | |
| ipm = Fz x 4 x rpm | diamond coating will increase tool life in graphite and composite materials |
| adjust parameters based on resin type and fiber structure | refer to the KYOCERA SGS Tool Wizard® for complete technical information |
| reduce speed when overheating causes melting or damage to resin | (www.kyocera-sgstool.com) |
reduce feed if delamination or fraying occur finish cuts typically required reduced feed and cutting depths