Каталог SGS микро инструмент 2021 - страница 5
Навигация
 Каталог SGS фрезы для алюминия S-carb
 Каталог SGS монолитный инструмент из композитных материалов
 Каталог SGS инструмент для обработки алюминия
 Общий каталог SGS 2018
 Общий каталог SGS 2021
 Каталог SGS фрезы для труднообрабатываемых материалов Series 33
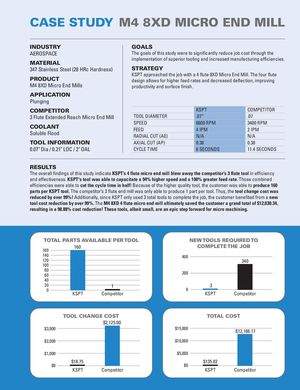
CASE STUDY M4 8XD MICRO END MILL
| INDUSTRY | GOALS |
| AEROSPACE | The goals of this study were to significantly reduce job cost through the |
| implementation of superior tooling and increased manufacturing efficiencies. | |
| MATERIAL | |
| 347 Stainless Steel (28 HRc Hardness) | STRATEGY |
| KSPT approached the job with a 4 flute 8XD Micro End Mill. The four flute | |
| PRODUCT | design allows for higher feed rates and decreased deflection, improving |
| M4 8XD Micro End Mills | productivity and surface finish. |
APPLICATION Plunging
| KSPT | COMPETITOR | |
| TOOL DIAMETER | .07” | .07 |
| SPEED | 6600 RPM | 3400 RPM |
| FEED | 4 IPM | 2 IPM |
| RADIAL CUT(AE) | N/A | N/A |
| AXIAL CUT(AP) | 0.38 | 0.38 |
| CYCLE TIME | 6 SECONDS | 11.4 SECONDS |
COOLANT Soluble Flood
RESULTS The overall findings of this study indicate KSPT’s 4 flute micro end mill blew away the competitor’s 3 flute tool in efficiency and effectiveness. KSPT's tool was able to capacitate a 94% higher speed and a 100% greater feed rate. Those combined efficiencies were able to cut the cycle time in half! Because of the higher quality tool, the customer was able to produce 160 parts per KSPT tool. The competitor’s 3 flute end mill was only able to produce 1 part per tool. Thus, the tool change cost was reduced by over 99%! Additionally, since KSPT only used 3 total tools to complete the job, the customer benefited from a new tool cost reduction by over 99%. The M4 8XD 4 flute micro end mill ultimately saved the customer a grand total of $12,030.34, resulting in a 98.88% cost reduction! These tools, albeit small, are an epic step forward for micro machining.
TOTAL PARTS AVAILABLE PER TOOL NEW TOOLS REQUIRED TO 160 COMPLETE THE JOB 160 140 400 120 340 100 80 60 200 40
| 20 | 1 | 3 | |
| 0 | 0 |
KSPT Competitor KSPT Competitor
TOOL CHANGE COST TOTAL COST $2,125.00
| $3,000 | $15,000 | $12,166.17 | ||||
| $2,000 | $10,000 | |||||
| $1,000 | $5,000 | |||||
| $18.75 | $135.82 | |||||
| $0 | $0 |
KSPT Competitor KSPT Competitor