Каталог SGS инструмент для обработки алюминия - страница 52
Навигация
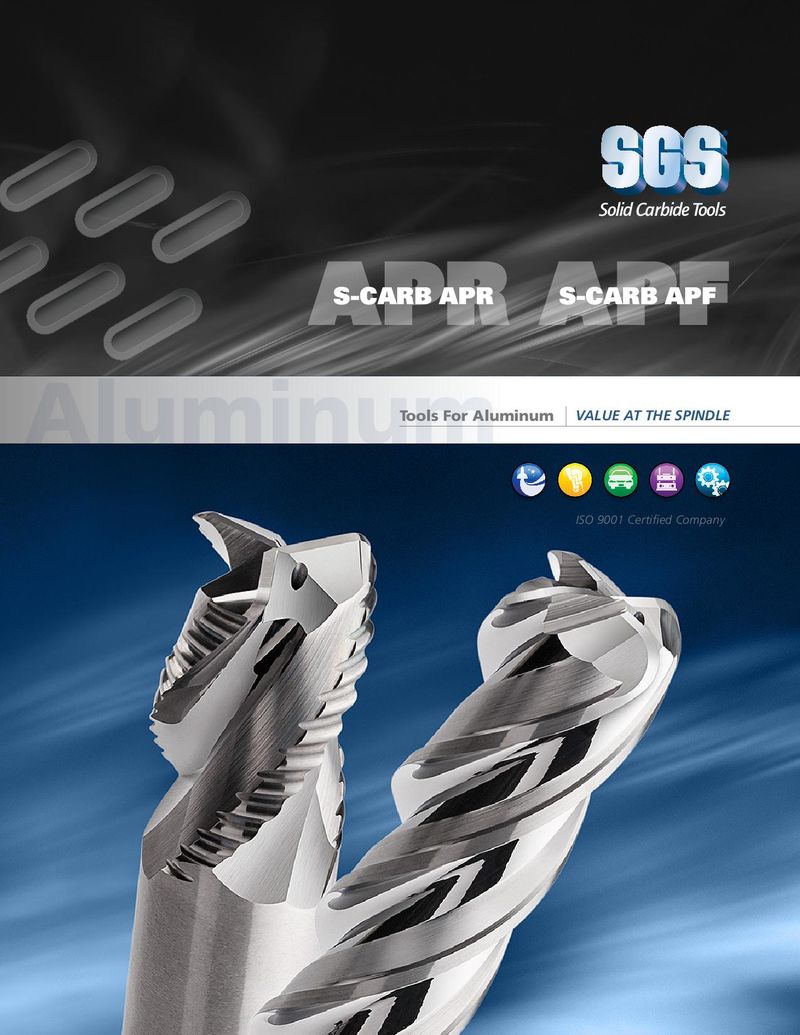 Каталог SGS фрезы для алюминия S-carb
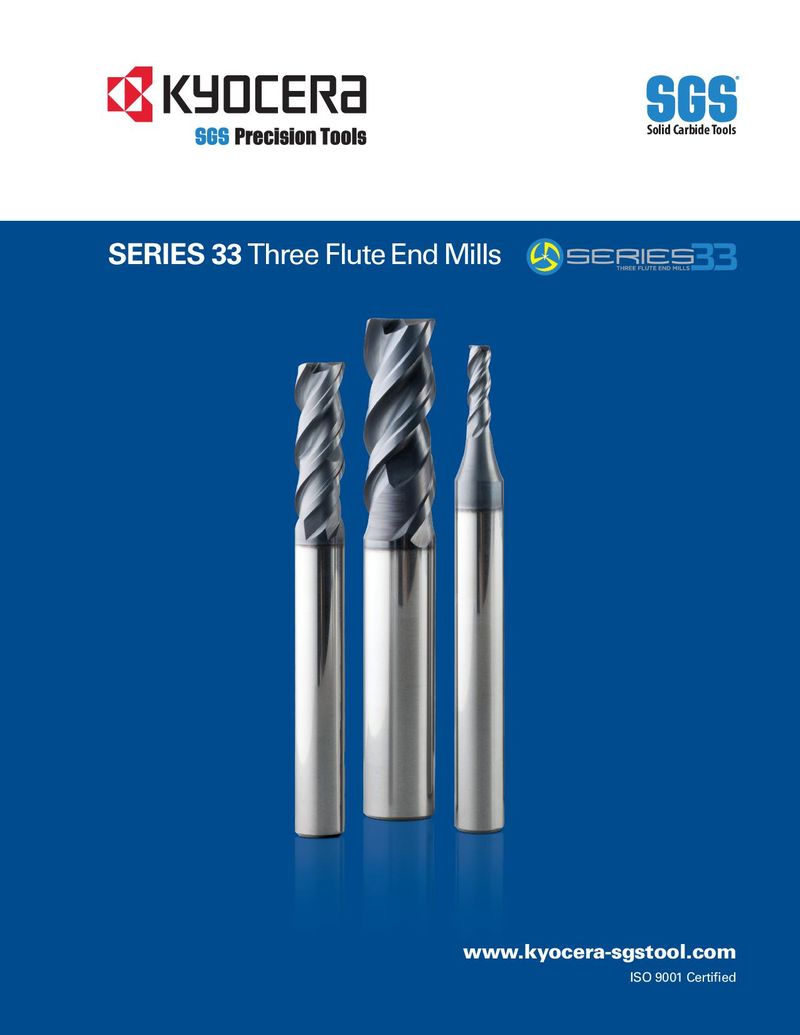 Каталог SGS фрезы для труднообрабатываемых материалов Series 33
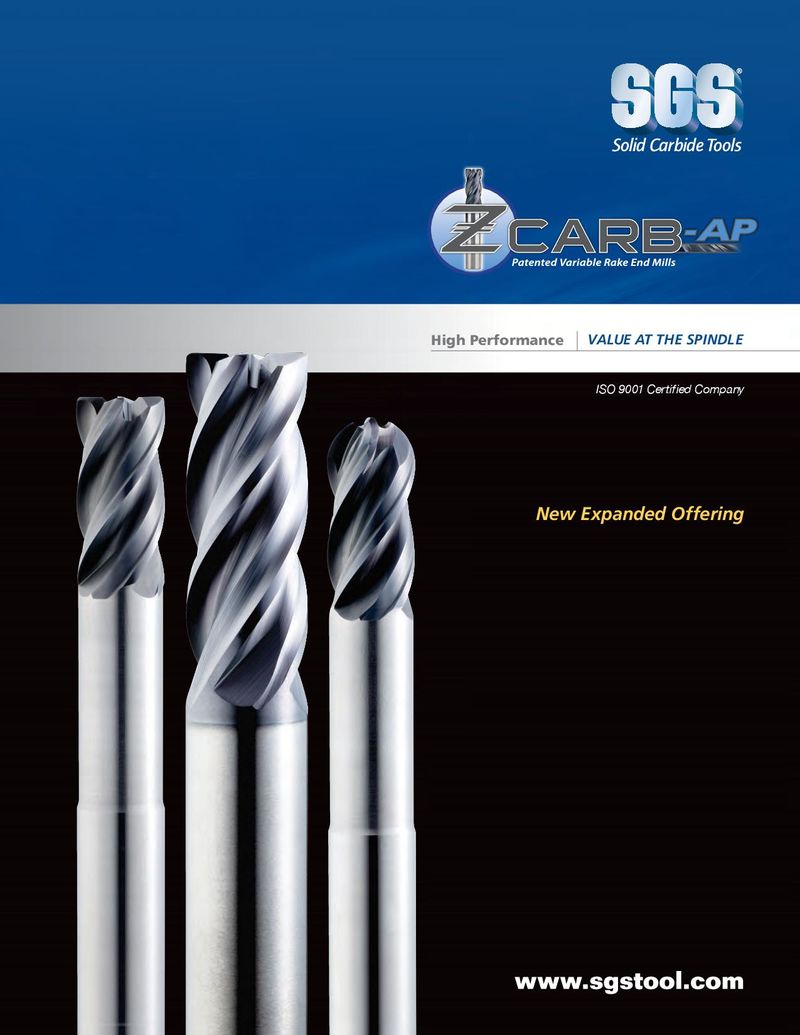 Каталог SGS фрезы с переменным углом спирали Z-carb
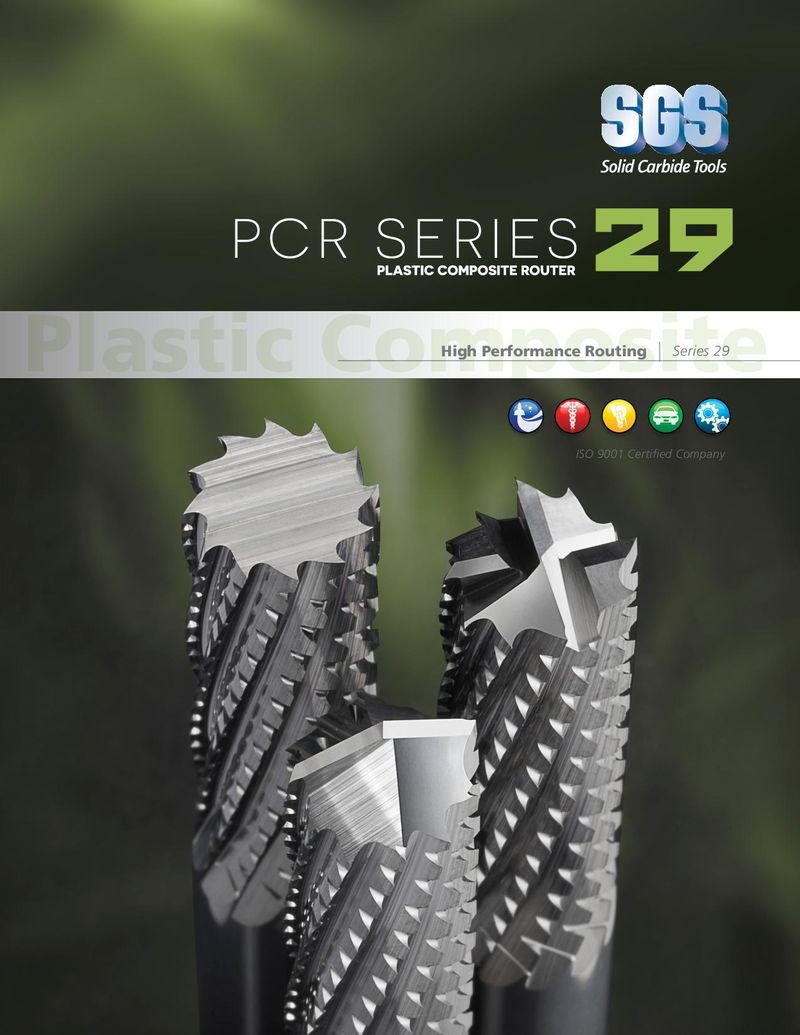 Каталог SGS фрезы для обработки пластика PCR series
 Каталог SGS микро инструмент 2021
 Каталог SGS шестизубые фрезы T-carb
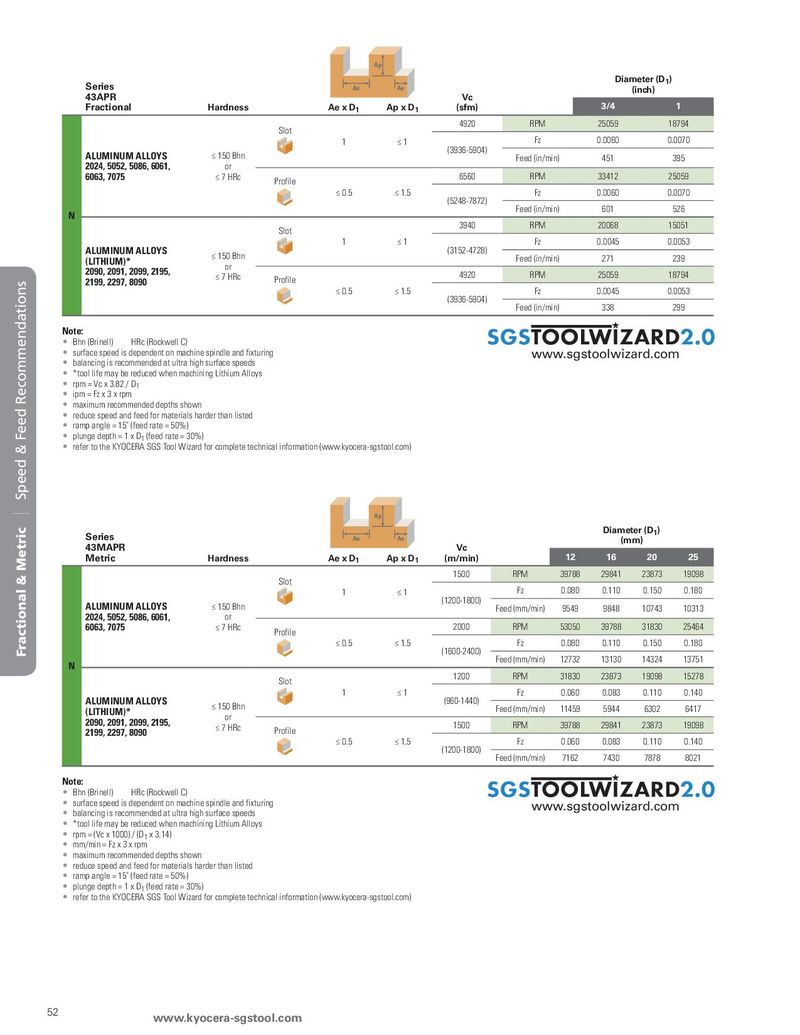
| Series 43APR | Ae | Ap Ae | Vc | Diame (in | ter (D1) ch) | |||
| Fractional | Hardness | Ae x D1 | Ap x D1 | (sfm) | 3/4 | 1 | ||
| Slot | 4920 | RPM | 25059 | 18794 | ||||
| 1 | ≤ 1 | (3936-5904) | Fz | 0.0060 | 0.0070 | |||
| ALUMINUM ALLOYS 2024 5052 5086 6061 | ≤ 150 Bhn or | Feed (in/min) | 451 | 395 | ||||
| , , , , 6063, 7075 | ≤ 7 HRc | Profile | 6560 | RPM | 33412 | 25059 | ||
| ≤ 0.5 | ≤ 1.5 | (5248-7872) | Fz | 0.0060 | 0.0070 | |||
| N | Feed (in/min) | 601 | 526 | |||||
| Slot | 3940 | RPM | 20068 | 15051 | ||||
| ALUMINUM ALLOYS | 1 | ≤ 1 | (3152-4728) | Fz | 0.0045 | 0.0053 | ||
| (LITHIUM) | ≤ 150 Bhn | Feed (in/min) | 271 | 239 | ||||
| 2090, 2091, 2099, 2195, 2199 2297 8090 | or ≤ 7 HRc | Profile | 4920 | RPM | 25059 | 18794 | ||
| , , | ≤ 0.5 | ≤ 1.5 | 39365904 | Fz | 0.0045 | 0.0053 | ||
| (-) | Feed (in/min) | 338 | 299 |
Note:
- Bhn (Brinell) HRc (Rockwell C)
- surface speed is dependent on machine spindle and fixturing www.sgstoolwizard.com
- balancing is recommended at ultra high surface speeds
- *tool life may be reduced when machining Lithium Alloys
- rpm = Vc x 3.82 / D
1
- ipm = Fz x 3 x rpm
- maximum recommended depths shown
- reduce speed and feed for materials harder than listed
- ramp angle = 15˚ (feed rate = 50%)
- plunge depth = 1 x D (feed rate = 30%)
1
- refer to the KYOCERA SGS Tool Wizard for complete technical information (www.kyocera-sgstool.com)
| Series 43MAPR | Ae | Ap Ae | Vc | Diame (m | ter (D1) m) | |||||
| Metric | Hardness | Ae x D1 | Ap x D1 | (m/min) | 12 | 16 | 20 | 25 | ||
| Slot | 1500 | RPM | 39788 | 29841 | 23873 | 19098 | ||||
| 1 | ≤ 1 | Fz | 0.080 | 0.110 | 0.150 | 0.180 | ||||
| ALUMINUM ALLOYS 2024 5052 5086 6061 | ≤ 150 Bhn | (1200-1800) | Feed (mm/min) | 9549 | 9848 | 10743 | 10313 | |||
| , , , , 6063, 7075 | or ≤ 7 HRc | Profile | 2000 | RPM | 53050 | 39788 | 31830 | 25464 | ||
| ≤ 0.5 | ≤ 1.5 | (16002400) | Fz | 0.080 | 0.110 | 0.150 | 0.180 | |||
| N | - | Feed (mm/min) | 12732 | 13130 | 14324 | 13751 | ||||
| Slot | 1200 | RPM | 31830 | 23873 | 19098 | 15278 | ||||
| 1 | ≤ 1 | Fz | 0.060 | 0.083 | 0.110 | 0.140 | ||||
| ALUMINUM ALLOYS (LITHIUM) | ≤ 150 Bhn | (960-1440) | Feed (mm/min) | 11459 | 5944 | 6302 | 6417 | |||
| 2090, 2091, 2099, 2195, 2199 2297 8090 | or ≤ 7 HRc | Profile | 1500 | RPM | 39788 | 29841 | 23873 | 19098 | ||
| , , | ≤ 0.5 | ≤ 1.5 | 12001800 | Fz | 0.060 | 0.083 | 0.110 | 0.140 | ||
| (-) | Feed (mm/min) | 7162 | 7430 | 7878 | 8021 |
Note:
- Bhn (Brinell) HRc (Rockwell C)
- surface speed is dependent on machine spindle and fixturing www.sgstoolwizard.com
- balancing is recommended at ultra high surface speeds
- *tool life may be reduced when machining Lithium Alloys
- rpm = (Vc x 1000) / (D x 3.14)
1
- mm/min = Fz x 3 x rpm
- maximum recommended depths shown
- reduce speed and feed for materials harder than listed
- ramp angle = 15˚ (feed rate = 50%)
- plunge depth = 1 x D (feed rate = 30%)
1
- refer to the KYOCERA SGS Tool Wizard for complete technical information (www.kyocera-sgstool.com)