Общий каталог PRECITOOL - страница 413
Навигация
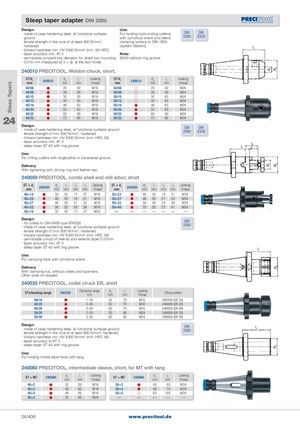
| - made of case-hardening steel, all functional surfaces | For holding tools (milling cutters) | DIN | DIN |
| ground | with cylindrical shank and lateral | 2080 | 6359 |
| - tensile strength in the core of at least 800 N/mm², | clamping surface to DIN 1835 | ||
| hardened | (system Weldon). | ||
| - Vickers hardness min. HV 6300 N/mm² (min. 56 HRC) | |||
| - taper accuracy min. AT 3 | Note: | ||
| - permissible concentricity deviation for direct tool mounting | SK50 without ring groove. | ||
| 0.015 mm (measured at 3 × d), at the tool holder | |||
| 240010 PRECITOOL, Weldon chuck, short, |
| ST/d | d | l | Locking | ST/d | d | l | Locking | ||
| 1 240010 | 3 | 1 | 1 240010 | 3 | 1 | ||||
| mm | mm | mm | thread | mm | mm | mm | thread | ||
| 40/06 | | 25 | 50 | M16 | 50/06 | | 25 | 50 | M24 |
| 40/08 | | 28 | 50 | M16 | 50/08 | | 28 | 50 | M24 |
| 40/10 | | 35 | 50 | M16 | 50/10 | | 35 | 63 | M24 |
| 40/12 | | 42 | 50 | M16 | 50/12 | | 42 | 63 | M24 |
| 40/16 | | 48 | 63 | M16 | 50/16 | | 48 | 63 | M24 |
| 40/20 | | 52 | 63 | M16 | 50/20 | | 52 | 63 | M24 |
| 24 40/25 | | 65 | 90 | M16 | 50/25 | | 65 | 80 | M24 |
| 40/32 | | 72 | 90 | M16 | 50/32 | | 72 | 85 | M24 |
Design: DIN DIN - made of case-hardening steel, all functional surfaces ground 2080 6358
- tensile strength of min. 800 N/mm², hardened - Vickers hardness min. HV 6300 N/mm² (min. HRC 56) - taper accuracy min. AT 3 - steep taper ST 40 with ring groove
Use: For milling cutters with longitudinal or transversal groove.
Delivery: With tightening bolt, driving ring and feather key.
240050 PRECITOOL, combi shell end mill arbor, short
| ST × d | d | l | l | l | Locking | ST × d | d | l | l | l | Locking | ||
| 1 240050 | 3 | 1 | 2 | 3 | 1 240050 | 3 | 1 | 2 | 3 | ||||
| mm | mm | mm | mm | mm | thread | mm | mm | mm | mm | mm | thread | ||
| 40×16 | | 32 | 52 | 17 | 27 | M16 | 50×22 | | 40 | 55 | 19 | 31 | M24 |
| 40×22 | | 40 | 52 | 19 | 31 | M16 | 50×27 | | 48 | 55 | 21 | 33 | M24 |
| 40×27 | | 48 | 52 | 21 | 33 | M16 | 50×32 | | 58 | 55 | 24 | 38 | M24 |
| 40×32 | | 58 | 52 | 24 | 38 | M16 | 50×40 | | 70 | 55 | 27 | 41 | M24 |
| 50×16 | | 32 | 55 | 17 | 27 | M24 | — | — | — | — | — | — | — |
Design: DIN - for collets to DIN 6499 type ER/ESX 2080
- made of case-hardening steel, all functional surfaces ground - tensile strength of min. 800 N/mm², hardened - Vickers hardness min. HV 6300 N/mm² (min. HRC 56) - permissible runout of internal and external taper 0.01mm - taper accuracy min. AT 3 - steep taper ST 40 with ring groove
Use: For clamping tools with cylindrical shank.
Delivery: With clamping nut, without collets and spanners. Other sizes on request.
240030 PRECITOOL, collet chuck ER, short
| ST/chucking range | 240030 | Clamping range mm | d3 mm | l1 mm | Locking thread | Fitting collets |
| 40/16 | | 1-16 | 42 | 70 | M16 | 248559 (ER 25) |
| 40/20 | | 2-20 | 50 | 70 | M16 | 248609 (ER 32) |
| 40/26 | | 3-30 | 63 | 70 | M16 | 248659 (ER 40) |
| 50/20 | | 2-20 | 50 | 80 | M24 | 248609 (ER 32) |
| 50/26 | | 3-30 | 63 | 80 | M24 | 248659 (ER 40) |
| Design: - made of case-harde | ning steel, a | ll functional surfac | es ground | DIN 2080 |
- tensile strength in the core of at least 800 N/mm², hardened - Vickers hardness min. HV 6300 N/mm² (min. HRC 56) - taper accuracy to AT 3 - steep taper ST 40 with ring groove
Use: For holding morse taper tools with tang.
240060 PRECITOOL, intermediate sleeve, short, for MT with tang
| ST × MT | 240060 | d3 mm | l1 mm | Locking thread | ST × MT | 240060 | d3 mm | l1 mm | Locking thread |
| 40×2 | | 32 | 50 | M16 | 50×3 | | 40 | 65 | M24 |
| 40×3 | | 40 | 65 | M16 | 50×4 | | 48 | 70 | M24 |
| 40×4 | | 48 | 95 | M16 | 50×5 | | 63 | 105 | M24 |
| 50×2 | | 32 | 60 | M24 | — | — | — | — | — |