Общий каталог PRECITOOL - страница 270
Навигация
Roughing cutter VHM Universal, with toric cut
P M K Design: Use:
Cat. no. - unequal division - universally applicable Factory Type Teeth Blade form
N/mm2 N/mm2 HB VHM chamfer
| - shank with toric cut | - for roughing | standard | HR | 4 | ||||
| 177410 | < 650 | - cutting edges with | - for large cutting depths | coated | ||||
| < 1200 | < 850 | |||||||
| 177412 | < 850 | a 45° chamfer | - extremely high cutting | UNI | ||||
| vc = m/min. | - AlCrN coated | performance | 6535 HB | |||||
| Shank | ||||||||
| 177410 | - HR ripper cutter profile | - very high running smoothness | Centre cut shank | long | overlong | Solid Carbide End Mills relieved |
110-280 80-110 110-200 - ideal on low-performance 177412 17 machines Note (177412): Cutting data
When used in Weldon chucks, please note the programming length!
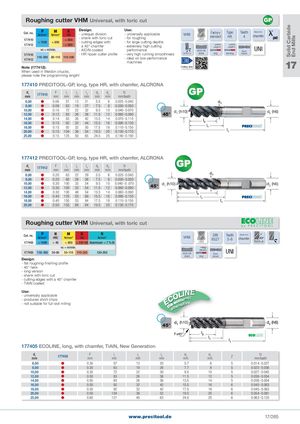
177410 PRECITOOL-GP, long, type HR, with chamfer, ALCRONA
| d | F | l | l | l | d | d | fz | |
| 1 | 177410 | 1 | 2 | 4 | 3 | 2 | ||
| mm | mm | mm | mm | mm | mm | mm | mm/tooth | |
| 6,00 | | 0�06 | 57 | 13 | 21 | 5�5 | 6 | 0�025 - 0�040 |
| 3 | ||||||||
| 8,00 | | 0�08 | 63 | 19 | 27 | 7�5 | 8 | 0�030 - 0�050 |
| 10,00 | | 0�10 | 72 | 22 | 32 | 9�5 | 10 | d (h6) d (h10) 0�040 - 0�070 |
| 12,00 | 0�12 | 83 | 26 | 38 | 11�5 | 12 | 2 1 45° 0�060 - 0�090 | |
| 14,00 | | 0�14 | 83 | 26 | 42 | 13�5 | 14 | 0�070 - 0�110 |
| 16,00 | | 0�15 | 92 | 32 | 44 | 15�5 | 16 | 0�090 - 0�130 |
| 18,00 | | 0�15 | 92 | 32 | 50 | 17�5 | 18 | 4 0�110 - 0�150 |
| 20,00 | | 0�15 | 104 | 38 | 54 | 19�5 | 20 | 0�130 - 0�170 |
| 25,00 | | 0�15 | 125 | 50 | 65 | 24�5 | 25 | 0�140 - 0�190 |
177412 PRECITOOL-GP, long, type HR, with chamfer, ALCRONA
| d | F | l | l | l | d | d | fz | |
| 1 | 177412 | 1 | 2 4 | 3 2 | ||||
| mm | mm | mm | mm | mm | mm | mm | mm/tooth | |
| 6,00 | | 0�20 | 63 | 22 | 29 | 5�5 | 6 | 3 0�025 - 0�040 |
| 8,00 | | 0�20 | 80 | 28 | 36 | 7�5 | 8 | 0�030 - 0�050 |
| 10,00 | | 0�30 | 100 | 33 | 54 | 9�5 | 10 | d (h6) d (h10) 45° 0�040 - 0 �070 |
| 12,00 | 0�30 | 100 | 33 | 54 | 11�5 | 12 | 2 1 0�060 - 0�090 | |
| 14,00 | | 0�30 | 100 | 48 | 54 | 13�5 | 14 | 0�060 - 0�090 |
| 16,00 | | 0�40 | 125 | 53 | 69 | 15�5 | 16 | 0�090 - 0�130 |
| 18,00 | 0�40 | 150 | 53 | 84 | 17�5 | 18 | 4 0�110 - 0�150 | |
| 20,00 | | 0�50 | 150 | 68 | 84 | 19�5 | 20 | 0�130 - 0�170 |
| Roughing cutter VHM Universal, with toric cut | ||||||||
| P | H | M | K | N | Teeth DIN |
Cat. no. VHM Blade form
| N/mm2 | HRC | N/mm2 | HB N/mm2 | 6527 | 45° chamfer 5-6 | |||
| 177405 | < 1400 | < 48 | < 850 > 250 HB Aluminium < 7 % Si | Twist | ||||
| coated | ||||||||
| vc = m/min. | UNI | |||||||
| 177405 110-160 | 50-80 | 55-110 110-230 | 130-250 | 6535 HB | ||||
| Shank | ||||||||
| shank | long | relieved |
Design: - flat roughing-finishing profile - 45° helix - long version
- shank with toric cut - cutting edges with a 45° chamfer - TiAlN coated
Use: E - universally applicable OLIN
| - produces short chips | EC | mic | ||
| ono | ||||
| - not suitable for full-slot milling | ec | ative |
the ern alt (h10) 45°
4
177405 ECOLINE, long, with chamfer, TiAlN, New Generation
| d1 mm | 177405 | F mm | l1 mm | l2 mm | l4 mm | d3 mm | d2 mm | Z | fz mm/tooth |
| 6,00 | | 0�30 | 57 | 13 | 20 | 5�7 | 6 | 5 | 0�014 - 0�027 |
| 8,00 | | 0�30 | 63 | 19 | 26 | 7�7 | 8 | 5 | 0�022 - 0�036 |
| 10,00 | | 0�30 | 72 | 22 | 30 | 9�5 | 10 | 5 | 0�027 - 0�045 |
| 12,00 | | 0�50 | 83 | 26 | 36 | 11�5 | 12 | 5 | 0�036 - 0�054 |
| 14,00 | | 0�50 | 83 | 26 | 36 | 13�5 | 14 | 5 | 0�036 - 0�054 |
| 16,00 | | 0�50 | 92 | 32 | 42 | 15�5 | 16 | 6 | 0�045 - 0�063 |
| 18,00 | | 0�50 | 92 | 32 | 42 | 17�5 | 18 | 6 | 0�045 - 0�063 |
| 20,00 | | 0�50 | 104 | 38 | 52 | 19�5 | 20 | 6 | 0�054 - 0�081 |
| 25,00 | | 0�60 | 121 | 45 | 63 | 24�0 | 25 | 6 | 0�063 - 0�120 |