Общий каталог PRECITOOL - страница 220
Навигация
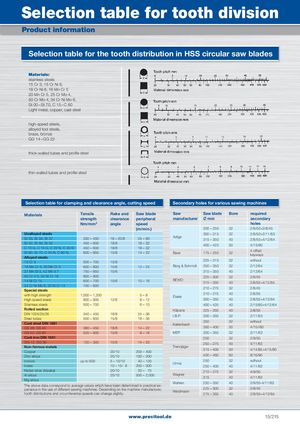
Selection table for tooth division
Selection table for the tooth distribution in HSS circular saw blades
Materials:
stainless steels
15 Cr 3, 15 Cr Ni 6,
18 Cr Ni 8, 16 Mn Cr 5
20 Mn Cr 5, 25 Cr Mo 4, 50 Cr Mo 4, 34 Cr Ni Mo 6,
St 00 – St 70, C 15 – C 60
Light metal, copper, cast steel
high-speed steels, alloyed tool steels,
brass, bronze
GG 14 – GG 22
thick-walled tubes and profile steel
thin-walled tubes and profile steel
| Selection table for cla | mping and cleara | nce angle, cu | tting speed | Secondary ho | les for vario | us sawin | g machines |
| Materials | Tensile strength Nm/mm2 | Rake and clearance angle | Saw blade peripheral speed | Saw manufacturer | Saw blade Xmm | Bore | required secondary holes |
| (m/min.) | 200 – 250 | 32 | 2/9/50+2/8/45 | ||||
| Unalloyed steels | Adi | 300 – 315 | 32 | 2/9/50+2/11/63 | |||
| St 33,St 34,St 37 | 330 – 450 | 18 – 20/8 | 24 – 60 | ge | 315 – 350 | 40 | 2/8/55+4/12/64 |
| St 42,St 50,St 52 C 10 G,C 15 G,C 22 N,C 35 | 450 – 600 N 450 – 600 | 18/8 18/8 | 18 – 32 18 – 32 | 400 – 425 | 50 | 4/15/80 | |
| St 60,St 70,C 45 N,C 60 N, | 600 – 850 | 15/8 | 14 – 22 | Baier | 175 – 250 | 32 | 4 offset keyways |
| Alloyed steels | |||||||
| 15 Cr 3 | 500 – 700 | 15/8 | 225 – 315 | 32 | without | ||
| 16 Mn Cr 5,20 Mn Cr 5 | 600 – 800 | 15/6 | 12 – 24 | Berg & Schmidt | 250 – 350 | 32 | 2/12/64 |
| 37 Mn St 5,42 Mn V 7 | 750 – 850 | 15/6 | 315 – 350 | 40 | 2/12/64 | ||
| 50 Cr V 3,35 Ni Cr 18 | 800 – 900 | 225 – 300 | 32 | 2/8/45 | |||
| 14 Ni Cr 14 | 600 – 700 | 15/6 | 10 – 16 | BEWO | 315 – 350 | 40 | 2/8/55+4/12/64 |
| 34 Cr Ni Mo 6,22 Ni Cr 14 Special steels | 700 – 800 | 210 – 275 | 32 | 2/8/45 | |||
| with high strength | 1,000 – 1,200 | 5 – 8 | Eisele | 210 – 275 | 40 | 2/8/55 | |
| High speed steels | 800 – 900 | 12/6 | 8 – 12 | 300 – 350 | 40 | 2/8/55+4/12/64 | |
| Stainless steels | 500 – 700 | 6 – 10 | 400 – 425 | 40 | 2/15/80+4/12/64 | ||
| Rolled section | Häberle | 225 – 350 | 40 | 2/8/55 | |||
| DIN 1024/25/26 | 340 – 450 | 18/8 | 24 – 36 | IBP | 200 – 350 | 32 | 2/11/63 |
| Steel tubes | 500 – 600 | 15/8 | 18 – 36 | ... | |||
| Cast steel DIN 1681 | Kaltenbach | 250 | 32 | without | |||
| GS 38,GS 45 | 380 – 450 | 18/8 | 14 – 22 | 350 – 400 | 50 | 4/15//80 | |
| GS 52,GS 60 | 520 – 600 | 15/8 | 8 – 16 | MEP | 200 – 355 | 32 | 2/11/63 |
| Cast iron DIN 1691 | 250 | 32 | 2/9/50 | ||||
| GG 12,GG 30 | 120 – 300 | 15/6 | 14 – 25 | 250 – 275 | 40 | 4/11/63 | |
| Non-ferrous metals | Trennjäger | 315 – 400 | 50 | 4/14/85+4/15/80 | |||
| Copper | 20/10 | 200 – 400 | |||||
| Zinc alloys | 25/10 | 100 – 200 | 400 – 460 | 60 | 8/16/90 | ||
| bronze | upto 600 | 5 – 10/10 | 40 – 120 | Uli | 250 | 32 | without |
| brass | 10 – 15/ 8 | 200 – 300 | ma | 250 – 400 | 40 | 4/11/63 | |
| Nickel silver(Alpaka) | 20/10 | 20 – 75 | 210 – 275 | 32 | 4/9/50 | ||
| Al alloys | 25/10 | 500 – 2,000 | Wagner | 315 | 40 | 4/11/63 | |
| Mgalloys The above data correspond to | average values which h | ave been determ | ined in practical ex- | Wahlen | 250 – 350 | 40 | 2/8/55-4/11/63 |
| perience in the use of different | sawing machines. Dep | ending on the ma | chine manufacturer, | 225 – 300 | 32 | 2/8/45 | |
| tooth distributions and circum | ferential speeds can cha | nge slightly. | Weidmann | 275 – 350 | 40 | 2/8/55+4/12/64 |