Общий каталог PRECITOOL - страница 217
Навигация
Thread rolling die HSS
P M Metric DIN 13
Cat. no. HSS 60°
N/mm2 6g Metric 140560 thread < 850
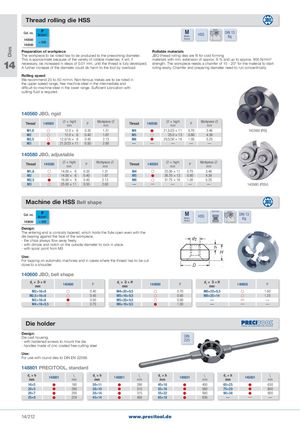
140580 Preparation of workpiece Rollable materials The workpiece to be rolled has to be produced to the preworking diameter. JBO thread rolling dies are fit for cold forming
14 This is approximate because of the variety of rollable materials; it will, if materials with min. extension of approx. 8 % and up to approx. 900 N/mm²
necessary, be increased in steps of 0.01 mm, until the thread is fully developed. strength. The workpiece needs a chamfer of 15 - 20° for the material to start A further increase of the diameter could do harm to the tool by overload. rolling easily. Chamfer and preparing diameter need to run concentrically. Rolling speed We recommend 20 to 50 m/min. Non-ferrous metals are to be rolled in
the upper speed range, free machine steel in the intermediate and difficult-to-machine steel in the lower range. Sufficient lubrication with cutting fluid is required.
140560 JBO, rigid
| Thread | 140560 | x× hight mm | P | Workpiecex mm | Thread | 140560 | x× hight mm | P | Workpiecex mm | |
| M1,6 | | 12�0 × 6 | 0�35 | 1�31 | M4 | | 21,5/23 × 11 | 0�70 | 3�46 | 140560 (RS) |
| M2 | | 12�0 × 6 | 0�40 | 1�67 | M5 | | 25�0 × 13 | 0�80 | 4�39 | |
| M2,5 | | 12�0/16 × 8 | 0�45 | 2�13 | M6 | | 29,5/30 × 16 | 1�00 | 5�25 | |
| M3 | | 21,5/23 × 11 | 0�50 | 2�60 | — | — | — | — | — |
140580 JBO, adjustable
| Thread | 140580 | x× hight mm | P | Workpiecex mm | Thread | 140580 | x× hight mm | P | Workpiecex mm |
| M1,6 | | 14�00 × 6 | 0�35 | 1�31 | M4 | | 25�00 × 11 | 0�70 | 3�46 |
| M2 | | 14�00 × 6 | 0�40 | 1�67 | M5 | | 26�70 × 13 | 0�80 | 4�39 |
| M2,5 | | 16�00 × 8 | 0�45 | 2�13 | M6 | | 31�75 × 16 | 1�00 | 5�25 |
| M3 | | 25�00 × 11 | 0�50 | 2�60 | — | — | — | — | — |
Machine die HSS Bell shape
P M Spiral point Metric DIN 13
| Cat. no. | HSS | 60° | |||
| N/mm2 | 6g | ||||
| Metric |
140600 < 850 thread
Design: The entering end is conically tapered, which holds the flute open even with the die bearing against the face of the workpiece. - the chips always flow away freely.
- with dimple and notch on the outside diameter to lock in place. - with spiral point from M3
Use: For tapping on automatic machines and in cases where the thread has to be cut close to a shoulder.
140600 JBO, bell shape
| d1× D × H mm | 140600 | P | d1× D × H mm | 140600 | P | d1× D × H mm | 140600 | P |
| M2×16×8 | | 0�40 | M4×20×9,5 | | 0�70 | M6×20×9,5 | | 1�00 |
| M2,5×16×8 | | 0�45 | M5×16×9,5 | | 0�80 | M8×25×14 | | 1�25 |
| M3×16×8 | | 0�50 | M5×20×9,5 | | 0�80 | — | — | — |
| M4×16×9,5 | | 0�70 | M6×16×9,5 | | 1�00 | — | — | — |
Die holder
Design: Die cast housing. DIN - with hardened screws to mount the die 225 - handles made of zinc coated free-cutting steel
Use: For use with round dies to DIN EN 22568.
148801 PRECITOOL, standard
| d1× h mm | 148801 | l1 mm | d1× h mm | 148801 | l1 mm | d1× h mm | 148801 | l1 mm | d1× h mm | 148801 | l1 mm |
| 16×5 | | 160 | 30×11 | | 280 | 45×18 | | 450 | 65×25 | | 630 |
| 20×5 | | 200 | 38×10 | | 315 | 55×16 | | 560 | 75×20 | | 800 |
| 20×7 | | 200 | 38×14 | | 315 | 55×22 | | 560 | 90×36 | | 900 |
| 25×9 | | 224 | 45×14 | | 450 | 65×18 | | 630 | — | — | — |