Общий каталог Osawa 2018 - страница 439
Навигация
 Общий каталог Osawa 2021
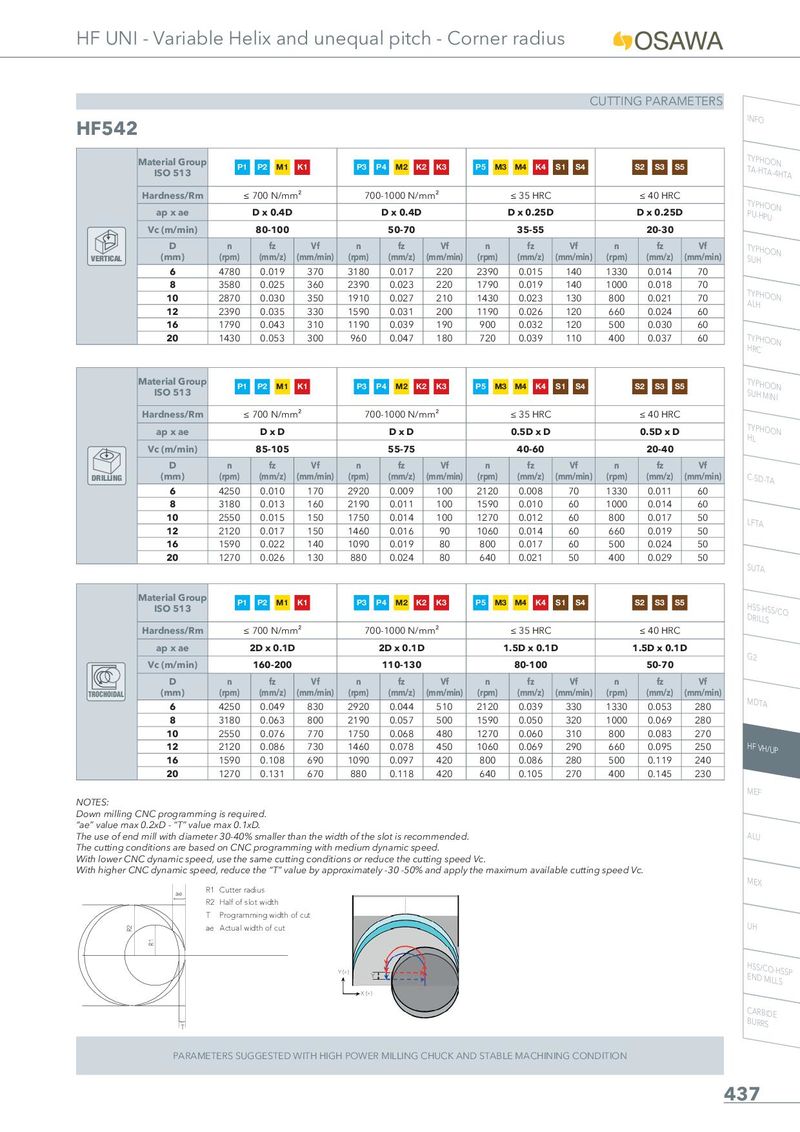
CUTTING PARAMETERS
HF542 INFO
| Material Group ISO 513 | P1 | P2 M1 | K1 | P3 | P4 M2 K2 | K3 | P5 M3 | M4 K4 | S1 S4 | S2 S3 S5 | |||
| Hardness/Rm | ≤ | 700 N/mm | ² | 70 | 0-1000 N/m | m² | ≤ 35 HRC | ≤ 40 HRC | |||||
| ap x ae | D x 0.4D | D x 0.4D | D x 0.25D | D x 0.25D | |||||||||
| Vc (m/min) | 80-100 | 50-70 | 35-55 | 20-30 | |||||||||
| D | n | fz | Vf | n | fz | Vf | n | fz | Vf | n | fz | Vf | |
| VERTICAL | (mm) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) |
| 6 | 4780 | 0.019 | 370 | 3180 | 0.017 | 220 | 2390 | 0.015 | 140 | 1330 | 0.014 | 70 | |
| 8 | 3580 | 0.025 | 360 | 2390 | 0.023 | 220 | 1790 | 0.019 | 140 | 1000 | 0.018 | 70 | |
| 10 | 2870 | 0.030 | 350 | 1910 | 0.027 | 210 | 1430 | 0.023 | 130 | 800 | 0.021 | 70 | |
| 12 | 2390 | 0.035 | 330 | 1590 | 0.031 | 200 | 1190 | 0.026 | 120 | 660 | 0.024 | 60 | |
| 16 | 1790 | 0.043 | 310 | 1190 | 0.039 | 190 | 900 | 0.032 | 120 | 500 | 0.030 | 60 | |
| 20 | 1430 | 0.053 | 300 | 960 | 0.047 | 180 | 720 | 0.039 | 110 | 400 | 0.037 | 60 | |
| Material Group ISO 513 | P1 | P2 M1 | K1 | P3 | P4 M2 K2 | K3 | P5 M3 | M4 K4 | S1 S4 | S2 S3 S5 | |||
| Hardness/Rm | ≤ | 700 N/mm | ² | 70 | 0-1000 N/m | m² | ≤ 35 HRC | ≤ 40 HRC | |||||
| ap x ae | DxD | DxD | 0.5D x D | 0.5D x D | |||||||||
| Vc (m/min) | 85-105 | 55-75 | 40-60 | 20-40 | |||||||||
| D | n | fz | Vf | n | fz | Vf | n | fz | Vf | n | fz | Vf | |
| DRILLING | (mm) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) | (rpm) | (mm/z) | (mm/min) |
| 6 | 4250 | 0.010 | 170 | 2920 | 0.009 | 100 | 2120 | 0.008 | 70 | 1330 | 0.011 | 60 | |
| 8 | 3180 | 0.013 | 160 | 2190 | 0.011 | 100 | 1590 | 0.010 | 60 | 1000 | 0.014 | 60 | |
| 10 | 2550 | 0.015 | 150 | 1750 | 0.014 | 100 | 1270 | 0.012 | 60 | 800 | 0.017 | 50 | |
| 12 | 2120 | 0.017 | 150 | 1460 | 0.016 | 90 | 1060 | 0.014 | 60 | 660 | 0.019 | 50 | |
| 16 | 1590 | 0.022 | 140 | 1090 | 0.019 | 80 | 800 | 0.017 | 60 | 500 | 0.024 | 50 | |
| 20 | 1270 | 0.026 | 130 | 880 | 0.024 | 80 | 640 | 0.021 | 50 | 400 | 0.029 | 50 | |
| Material Group ISO 513 | P1 | P2 M1 | K1 | P3 | P4 M2 K2 | K3 | P5 M3 | M4 K4 | S1 S4 | S2 S3 S5 | |||
| Hardness/Rm | ≤ | 700 N/mm | ² | 70 | 0-1000 N/m | m² | ≤ 35 HRC | ≤ 40 HRC | |||||
| ap x ae | 2D x 0.1D | 2D x 0.1D | 1 | .5D x 0.1 | D | 1.5D x 0.1 | D | ||||||
| Vc (m/min) | 160-200 | 110-130 | 80-100 | 50-70 | |||||||||
| TROCHOIDAL | D (mm) | n (rpm) | fz (mm/z) | Vf (mm/min) | n (rpm) | fz (mm/z) | Vf (mm/min) | n (rpm) | fz (mm/z) | Vf (mm/min) | n (rpm) | fz (mm/z) | Vf (mm/min) |
| 6 | 4250 | 0.049 | 830 | 2920 | 0.044 | 510 | 2120 | 0.039 | 330 | 1330 | 0.053 | 280 | |
| 8 | 3180 | 0.063 | 800 | 2190 | 0.057 | 500 | 1590 | 0.050 | 320 | 1000 | 0.069 | 280 | |
| 10 | 2550 | 0.076 | 770 | 1750 | 0.068 | 480 | 1270 | 0.060 | 310 | 800 | 0.083 | 270 | |
| 12 | 2120 | 0.086 | 730 | 1460 | 0.078 | 450 | 1060 | 0.069 | 290 | 660 | 0.095 | 250 | |
| 16 | 1590 | 0.108 | 690 | 1090 | 0.097 | 420 | 800 | 0.086 | 280 | 500 | 0.119 | 240 | |
| 20 | 1270 | 0.131 | 670 | 880 | 0.118 | 420 | 640 | 0.105 | 270 | 400 | 0.145 | 230 |
TYPHOON
TYPHOON ALH
HRC
TYPHOON HL
LFTA
SUTA
DRILLS
G2
MDTA
MEF NOTES: Down milling CNC programming is required. “ae” value max 0.2xD - “T” value max 0.1xD. The use of end mill with diameter 30-40% smaller than the width of the slot is recommended. ALU The cutting conditions are based on CNC programming with medium dynamic speed. With lower CNC dynamic speed, use the same cutting conditions or reduce the cutting speed Vc. With higher CNC dynamic speed, reduce the “T” value by approximately -30 -50% and apply the maximum available cutting speed Vc. MEX R1 Cutter radius ae R2 Half of slot width T Programming width of cut ae Actual width of cut UH
Y (+) Y X (+)
T
HSS/CO-HSSP END MILLS
CARBIDE BURRS