Общий каталог Osawa 2018 - страница 419
Навигация
 Общий каталог Osawa 2021
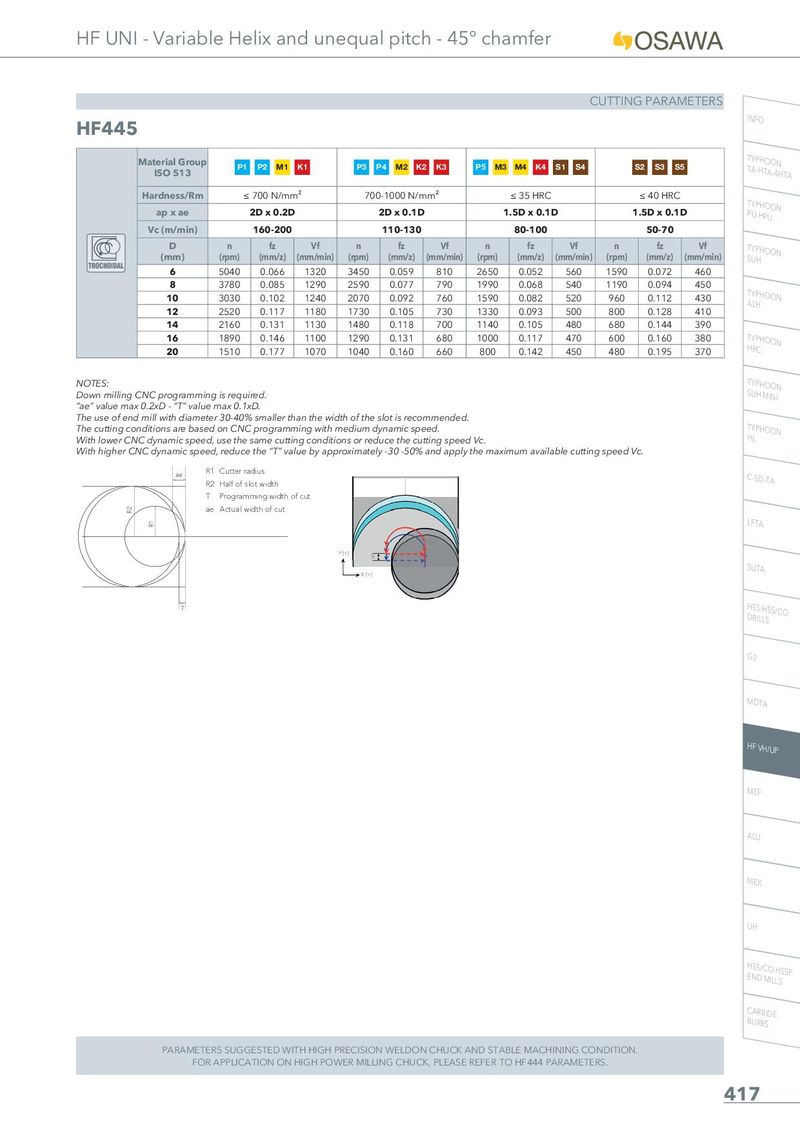
CUTTING PARAMETERS
HF445 INFO
| Material Group ISO 513 | P1 | P2 M1 | K1 | P3 | P4 M2 K2 | K3 | P5 M3 | M4 K4 | S1 S4 | S2 S3 S5 | ||
| Hardness/Rm | ≤ | 700 N/mm | ² | 70 | 0-1000 N/m | m² | ≤ 35 HRC | ≤ 40 HRC | ||||
| ap x ae | 2D x 0.2D | 2D x 0.1D | 1.5D x 0.1D | 1.5D x 0.1 | D | |||||||
| Vc (m/min) | 160-200 | 110-130 | 80-100 | 50-70 | ||||||||
| D (mm) | n (rpm) | fz (mm/z) | Vf (mm/min) | n (rpm) | fz (mm/z) | Vf (mm/min) | n (rpm) | fz (mm/z) | Vf (mm/min) | n (rpm) | fz (mm/z) | Vf (mm/min) |
| TROCHOIDAL 6 | 5040 | 0.066 | 1320 | 3450 | 0.059 | 810 | 2650 | 0.052 | 560 | 1590 | 0.072 | 460 |
| 8 | 3780 | 0.085 | 1290 | 2590 | 0.077 | 790 | 1990 | 0.068 | 540 | 1190 | 0.094 | 450 |
| 10 | 3030 | 0.102 | 1240 | 2070 | 0.092 | 760 | 1590 | 0.082 | 520 | 960 | 0.112 | 430 |
| 12 | 2520 | 0.117 | 1180 | 1730 | 0.105 | 730 | 1330 | 0.093 | 500 | 800 | 0.128 | 410 |
| 14 | 2160 | 0.131 | 1130 | 1480 | 0.118 | 700 | 1140 | 0.105 | 480 | 680 | 0.144 | 390 |
| 16 | 1890 | 0.146 | 1100 | 1290 | 0.131 | 680 | 1000 | 0.117 | 470 | 600 | 0.160 | 380 |
| 20 | 1510 | 0.177 | 1070 | 1040 | 0.160 | 660 | 800 | 0.142 | 450 | 480 | 0.195 | 370 |
TYPHOON
TYPHOON ALH
| NOTES: | TYPHOON |
| Down milling CNC programming is required. | SUH MINI |
| “ae” value max 0.2xD - “T” value max 0.1xD. | |
| The use of end mill with diameter 30-40% smaller than the width of the slot is recommended. | |
| The cutting conditions are based on CNC programming with medium dynamic speed. | TYPHOON |
| With lower CNC dynamic speed, use the same cutting conditions or reduce the cutting speed Vc. | HL |
| With higher CNC dynamic speed, reduce the “T” value by approximately -30 -50% and apply the maximum available cutting speed Vc. | |
| R1 Cutter radius | |
| ae C-SD-TA |
R2 Half of slot width T Programming width of cut ae Actual width of cut LFTA
Y (+) Y SUTA X (+)
T HSS-HSS/CO DRILLS
G2
MDTA
HF VH/UP
MEF
ALU
MEX
UH
HSS/CO-HSSP END MILLS
CARBIDE BURRS