Общий каталог Lamina Technologies 2019 - 2020 - страница 188
Навигация
 Общий каталог Lamina Technologies 2017 - 2018
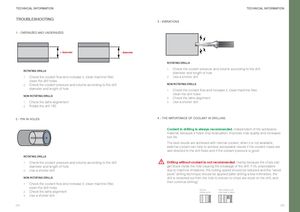
TROUBLESHOOTING
3 - VIBRATIONS
1 - OVERSIZED AND UNDERSIZED
+ diameter - diameter
ROTATING DRILLS 1. Check the coolant pressure and volume according to the drill ROTATING DRILLS diameter and length of hole
| 1. | Check the coolant flow and increase it, clean machine filter, | 2. | Use a shorter drill |
| clean the drill holes | |||
| 2. | Check the coolant pressure and volume according to the drill | NON ROTATING DRILLS |
diameter and lenght of hole Check the coolant flow and increase it, clean machine filter, 1. clean the drill holes NON ROTATING DRILLS Check the lathe alignment
2.
1. Check the lathe alignement 3. Use a shorter drill
2. Rotate the drill 180
2 - PIN IN HOLES 4 - THE IMPORTANCE OF COOLANT IN DRILLING Coolant in drilling is always recommended, independent of the workpiece material, because it helps chip evacuation, improves hole quality and increases tool life. The best results are achieved with internal coolant, when it is not available, external coolant can help to achieve acceptable results if the coolant noses are well directed to the drill flutes and if the coolant pressure is good. ROTATING DRILLS
| 1. | Check the coolant pressure and volume according to the drill | Drilling without coolant is not recommended, mainly because the chips can |
| diameter and length of hole | get stuck inside the hole causing the breakage of the drill. If it’s unavoidable | |
| 2. | Use a shorter drill | due to machine limitations, the cutting speed should be reduced and the “wood |
peck“ drilling technique should be applied (after drilling a few millimeters, the NON ROTATING DRILLS drill is retracted out from the hole to ensure no chips are stuck on the drill, and then continue drilling). 1. Check the coolant flow and increase it, clean machine filter,
clean the drill holes
| Check the lathe alignment | Normal | Peck drilling cycle | |
| 2. | drilling cycle | Hole made in steps |
3. Use a shorter drill