Общий каталог Lamina Technologies 2019 - 2020 - страница 182
Навигация
 Общий каталог Lamina Technologies 2017 - 2018
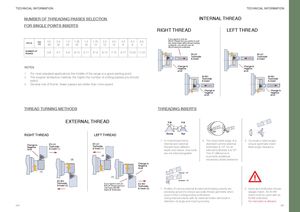
NUMBER OF THREADING PASSES SELECTION INTERNAL THREAD
FOR SINGLE POINTS INSERTS
RIGHT THREAD LEFT THREAD
| PITCH mm TPI | 0.5 48 | 0.8 32 1.0 24 | 1.25 20 1.5 16 | 1.75 14 | 2.0 12 | 2.5 10 | 3.0 8 | 4.0 6 6.0 4 | If you want to turn an IN-LH Thread but you prefer to pull the metal chips while thread turning outwards, you should use an IN-LH insert & toolholder | |
| NUMBER OF PASSES | 3-6 | 4-7 4-9 | 6-10 5-1 | 1 9-12 | 6-13 | 7-15 | 8-17 | 10-20 11-22 | IN-LH Toolholder & Insert | IN-LH Toolholder & Insert |
| NOTES | Change to negative anvil | Change to negative anvil | ||||||||
| . For most s . The tough select. . General ru | tandard er work le of thu | applications t piece material, mb: fewer pas | he middle of the higher t ses are bett | the range he numbe er than m | is a go r of cutti ore spee | od sta ng pas d. | rting poi ses you | nt. should | IN-RH Toolholder & Insert | IN-RH Toolholder & Insert |
| Change to negative anvil | Change to negative anvil |
Screw Nut
THREAD TURNING METHODS THREADING INSERTS
EXTERNAL THREAD
P/8 P/4
P/8 P/4 Internal - 15°
H h 15° 10°
H h 15° 10° External - 10°
| RIGHT THREAD | LEFT THREADP/8 | P/4 | Screw | Nut | |
| Screw | Nut |
H h 1. In most thread forms 15°10° 2. The insert relief angle of a 3. Our built-in relief angles
| Change to | EX-LH | EX-LH | internal and external | standard Lamina external | ensure automatic insert |
| Toolholder | Toolholder | Nut Screw | |||
| Negative | threads have different | toolholder is 10°; for an | flank angle clearance. | ||
| Anvil | & Insert (1) | & Insert (1) | |||
| depth and radius, thus tools | internal toolholder it is 15°. | ||||
| are not interchangeable | This 5° difference is | ||||
| (2) | to provide additional | ||||
| (2) | necessary radial clearance. |
Internal - 15° Change to Negative Internal - 15° Anvil
External - 10° (1) External - 10° Internal - 15° (1) EX-RH External - 10°
| Toolholder | If you want to turn an | EX-RH | ||
| & Insert (2) | EX-LH Thread and you | Toolholder | ||
| only have EX-RH | & Insert (2) | 1. Profiles of Lamina internal & external threading inserts are | 2. Insert and toolholder should | |
| Insert & Toolholder | ||||
| precisely ground to ensure accurate thread geometry when | always match. An IN-RH | |||
| used in their corresponding toolholders. | insert must be used with an | |||
| Using internal inserts with an external holder will result in | IN-RH toolholder. | |||
| distortion of angle and insert geometry. | No mismatch is allowed. |