Общий каталог Lamina Technologies 2019 - 2020 - страница 178
Навигация
 Общий каталог Lamina Technologies 2017 - 2018
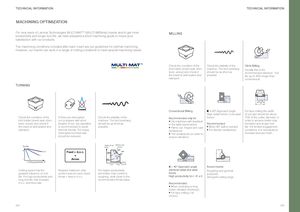
MACHINING OPTIMIZATION
For new users of Lamina Technologies MULTI-MAT TM (MULTI-MATerial) inserts and to get more productivity and longer tool life, we have prepared a short machining guide to insure your satisfaction with our products. The machining conditions included after each insert are our guidelines for optimal machining. However, our inserts can work in a range of cutting conditions to meet special machining needs.
TURNING
MILLING
V f
| Check the condition of the | Check the stability of the | Climb Milling |
| tool holder (insert seat, shim, | machine. The tool overhang | Usually this is the |
| lever, screw) and check if | should be as short as | recommended direction. Tool |
| the insert is well seated and | possible. | life up to 40% longer than |
clamped. conventional.
F h = f v z f z 0.7 x D V D f Coolant К
| Conventional Milling | = 90° Approach angle | For face milling the width | |||
| High radial forces / Low axial | of cut (ae) should be about | ||||
| Check the condition of the | If there are interrupted | Check the stability of the | Recommended only for: | forces. | 70% of the cutter diameter, in |
| tool holder (insert seat, shim, | cut or passes with short | machine. The tool overhang | • Old machines with backlash | order to achieve better chip | |
| lever, screw) and check if | lengths of cut, dry operation | should be as short as | in the table transmission | Recommended: | formation and longer tool |
| the insert is well seated and | is recommended to avoid | possible. | • Flame cut, forged and cast | • When 90° wall is needed | life. For limited engagement |
| clamped. | thermal shocks. For heavy | workpieces | • For slender workpieces | conditions, it is necessary to | |
| interrupted cut feed rate | • Thin workpieces (in order to | increase feed per tooth. | |||
| should be reduced. | reduce vibration) |
| Tool life | Depth of cut | Section max | |||
| [mm] | [mm2 ] | ||||
| + | Feed d.o.c. | ||||
| d.o.c. | x |
fn = 45°
| - | Vc | Amax | |
| f h = 0.71 x f |
| - Cutting parameters + | z | z | |
| Feed |
| f min | f max | [mm/t] | ||
| K = 45° Approach angle | Round Inserts: |
| Cutting speed has the | Respect maximum chip | For higher productivity | identical radial and axial | Roughing and general |
| greatest influence on tool | section area for each insert. | and better chip control in | forces. | purposes. |
| life. For high productivity and | Amax = feed x d.o.c. | roughing, work close to the | High productivity fz=1.41 x h | Strongest cutting edge. |
long tool life, first increase recommended Amax value. d.o.c. and feed rate. Recommended:
- When overhang is long
(lower vibration tendency)
- For face milling (1st
choice)