Основной каталог Kyocera 2016-2017 - страница 143
Навигация
 Каталог Kyocera фрезы MFH для высокоскоростной обработки
 Каталог Kyocera фрезы MEC высокопроизводительные концевые и торцевые фрезы
 Каталог микроинструмента Kyocera 2015-2016
 Каталог Kyocera высокоэффективные сверла со сменными пластинами DRV
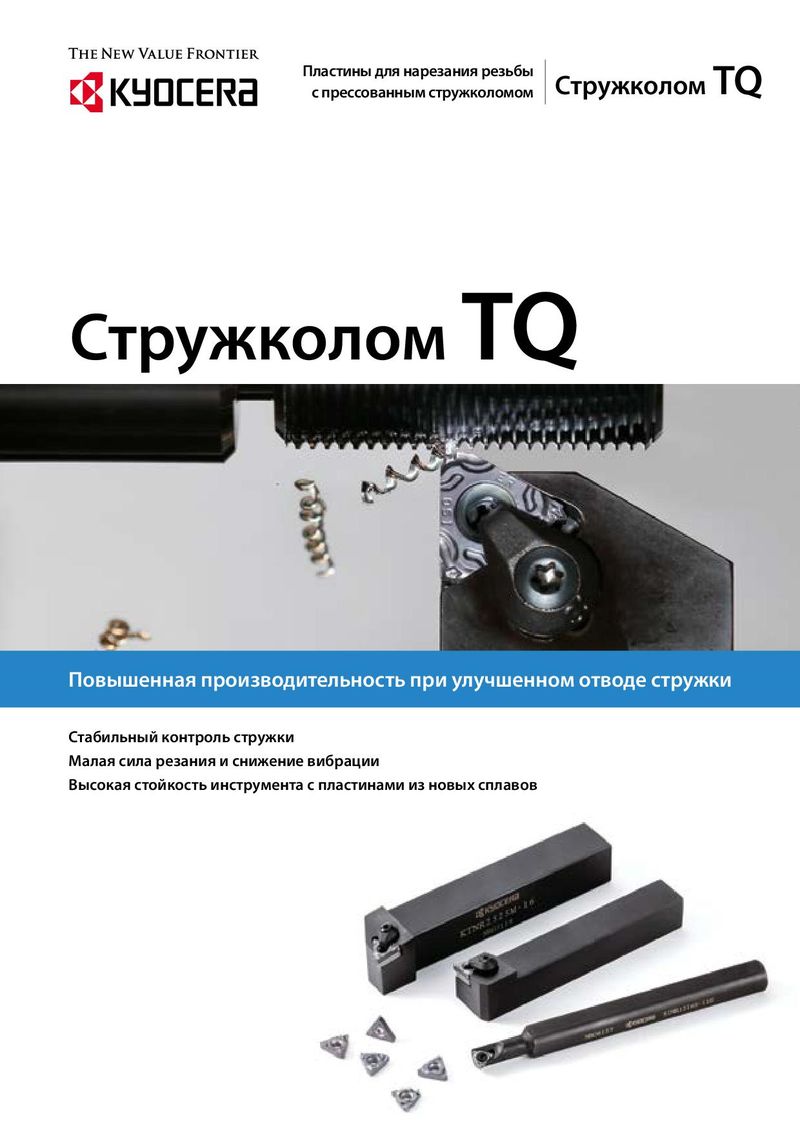 Каталог Kyocera пластины TQ для нарезания резьбы c прессованным стружколомом
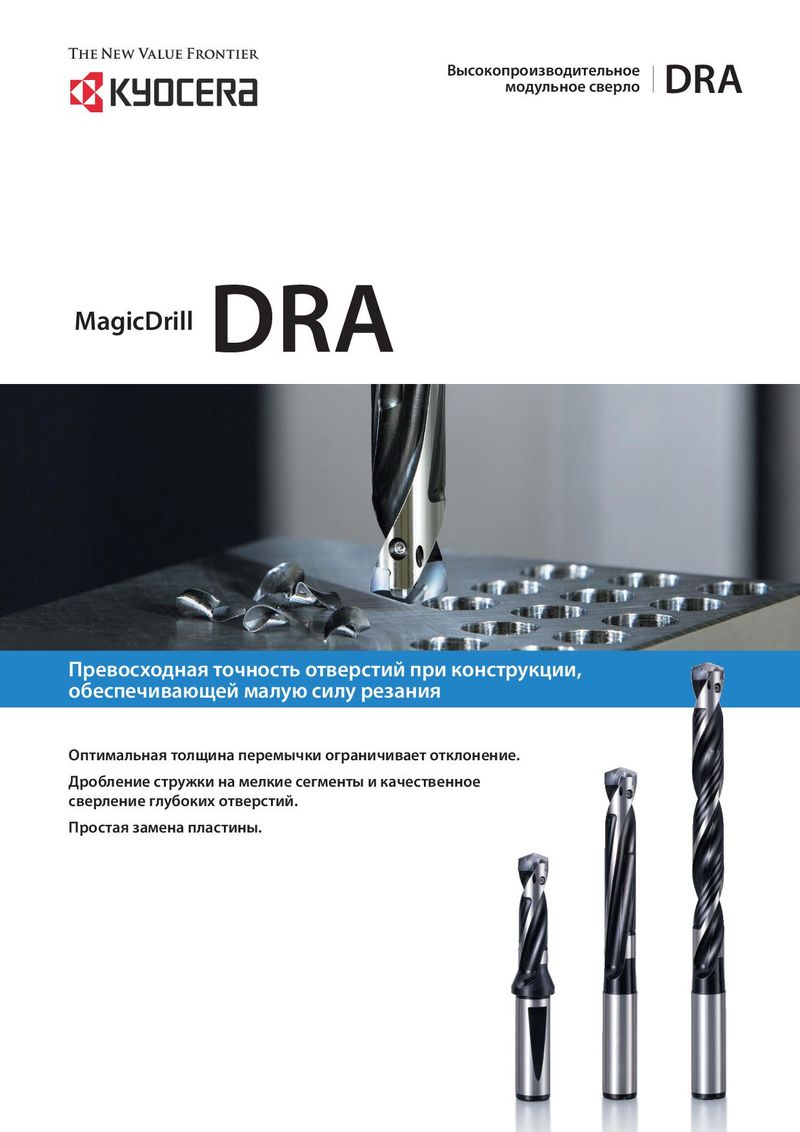 Каталог Kyocera высокопроизводительные модульные сверла DRA
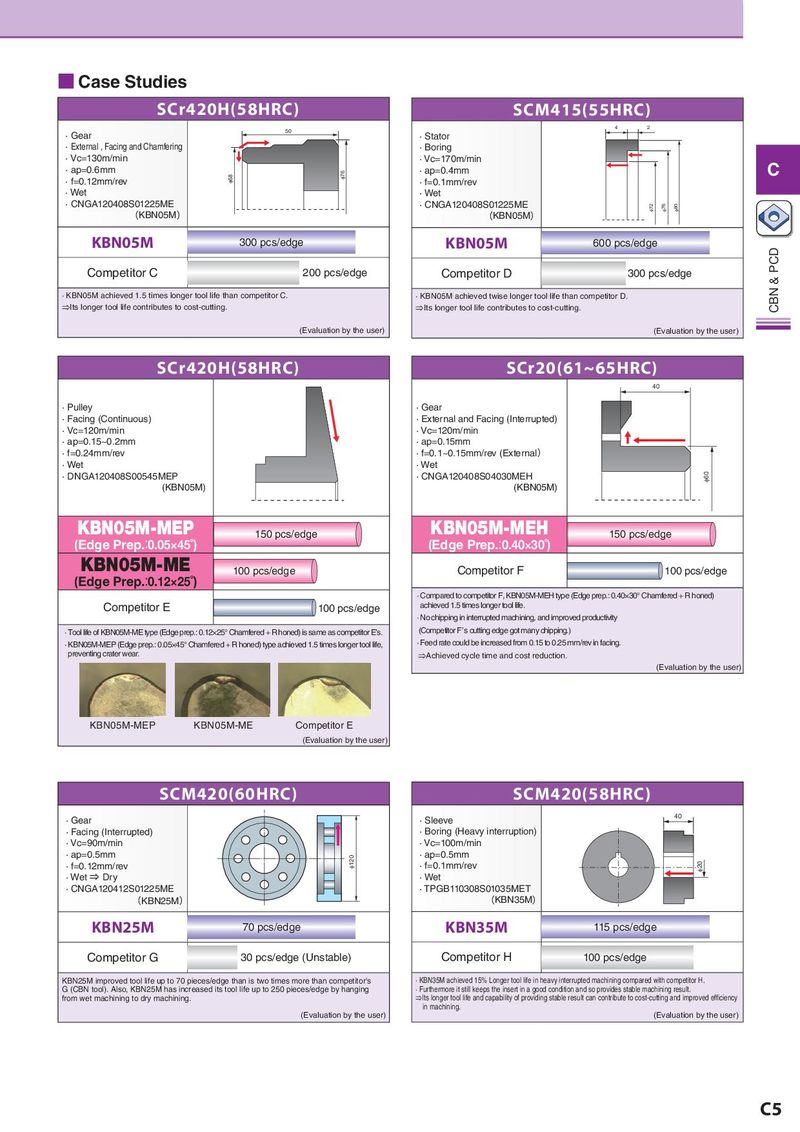
■ Case Studies
SCr420H(58HRC) SCM415(55HRC)
4 2
- Gear 50
- Stator
- External , Facing and Chamfering
- Boring
- Vc=130m/min
- Vc=170m/min C
- ap=0.6mm
- ap=0.4mm
- f=0.12mm/rev
- f=0.1mm/rev
- Wet
- Wet
- CNGA120408S01225ME
- CNGA120408S01225ME
(KBN05M) (KBN05M)
| KBN05M | 300 pcs/edge | KBN05M | 600 pcs/edge | ||
| Competitor C | 200 pcs/edge | Competitor D | 300 pcs/edge |
- KBN05M achieved 1.5 times longer tool life than competitor C.
- KBN05M achieved twise longer tool life than competitor D.
⇒Its longer tool life contributes to cost-cutting. ⇒Its longer tool life contributes to cost-cutting. (Evaluation by the user) (Evaluation by the user)
SCr420H(58HRC) SCr20(61~65HRC)
40
- Pulley
- Gear
- Facing (Continuous)
- External and Facing (Interrupted)
- Vc=120m/min
- Vc=120m/min
- ap=0.15~0.2mm
- ap=0.15mm
- f=0.24mm/rev
- f=0.1~0.15mm/rev (External)
- Wet
- Wet
- DNGA120408S00545MEP
- CNGA120408S04030MEH
(KBN05M) (KBN05M)
KBN05M-MEP KBN05M-MEH
150 pcs/edge 150 pcs/edge
(Edge Prep.:0.05×45˚) (Edge Prep.:0.40×30˚)
KBN05M-ME
100 pcs/edge Competitor F 100 pcs/edge
(Edge Prep.:0.12×25˚)
- Compared to competitor F, KBN05M-MEH type (Edge prep.: 0.40×30° Chamfered + R honed)
Competitor E 100 pcs/edge achieved 1.5 times longer tool life.
- No chipping in interrupted machining, and improved productivity
- Tool life of KBN05M-ME type (Edge prep.: 0.12×25° Chamfered + R honed) is same as competitor E’s. (Competitor F’s cutting edge got many chipping.)
- KBN05M-MEP (Edge prep.: 0.05×45° Chamfered + R honed) type achieved 1.5 times longer tool life,
- Feed rate could be increased from 0.15 to 0.25 mm/rev in facing.
preventing crater wear. ⇒Achieved cycle time and cost reduction. (Evaluation by the user)
KBN05M-MEP KBN05M-ME Competitor E
(Evaluation by the user) SCM420(60HRC) SCM420(58HRC)
- Gear
- Sleeve 40
- Facing (Interrupted)
- Boring (Heavy interruption)
- Vc=90m/min
- Vc=100m/min
- ap=0.5mm
- ap=0.5mm
- f=0.12mm/rev
- f=0.1mm/rev
- Wet ⇒ Dry
- Wet
- CNGA120412S01225ME
- TPGB110308S01035MET
(KBN25M) (KBN35M)
| KBN25M | 70 pcs/edge | KBN35M | 115 pcs/edge | ||
| Competitor G | 30 pcs/edge (Unstable) | Competitor H | 100 pcs/edge | ||
| KBN25M improved tool life up to 70 pieces/edge than is two times more than competitor's | · KBN35M achieved 15% Longer tool life in heavy interrupted machining compared with competitor H. | ||||
| G (CBN tool). Also, KBN25M has increased its tool life up to 250 pieces/edge by hanging | · Furthermore it still keeps the insert in a good condition and so provides stable machining result. | ||||
| from wet machining to dry machining. | ⇒Its longer tool life and capability of providing stable result can contribute to cost-cutting and improved efficiency | ||||
| in machining. | |||||
| (Evaluation by the user) | (Evaluation by the user) |