Каталог Iscar вращающийся инструмент 2017 - страница 258
Навигация
 Каталог Iscar токарные пластины ISO 2022
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar решения для глубокого сверления
 Каталог Iscar полирующие фрезы
 Новые режущие инструменты Iscar 2026
 Каталог Iscar новые продукты 2018
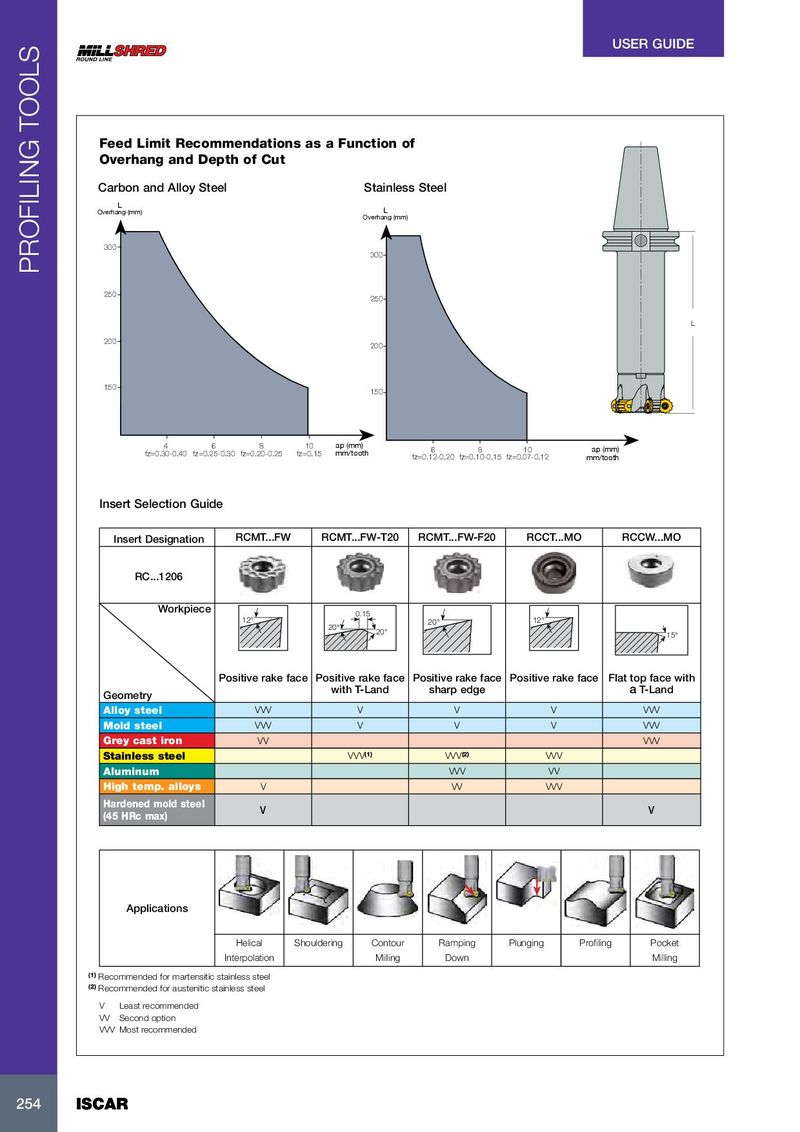
Feed Limit Recommendations as a Function of
Overhang and Depth of Cut
Carbon and Alloy Steel Stainless Steel
L Overhang (mm) L Overhang (mm)
300 300
250 250 L 200 200
150 150
4 6 8 10 ap (mm)
mm/tooth 6 8 10 ap (mm)
fz=0.30-0.40 fz=0.25-0.30 fz=0.20-0.25 fz=0.15 fz=0.12-0.20 fz=0.10-0.15 fz=0.07-0.12 mm/tooth
Insert Selection Guide
Insert Designation RCMT...FW
RC...1206
Workpiece
12°
RCMT...FW-T20 RCMT...FW-F20 RCCT...MO RCCW...MO
0.15 20° 12° 20° 20° 15°
Positive rake face Positive rake face Positive rake face Positive rake face Flat top face with
| with T-Land | sharp edge | a T-Land | |
| Geometry |
| Alloy steel | VVV | V | V | V | VVV |
| Mold steel | VVV | V | V | V | VVV |
| Grey cast iron | VV | VVV | |||
| Stainless steel | VVV(1) | VVV(2) | VVV | ||
| Aluminum | VVV | VV | |||
| High temp. alloys | V | VV | VVV | ||
| Hardened mold steel | V | V |
(45 HRc max)
Applications
| Helical | Shouldering | Contour | Ramping | Plunging | Profiling | ||
| Interpolation | Milling | Down | Milling |
(1) Recommended for martensitic stainless steel (2) Recommended for austenitic stainless steel V Least recommended VV Second option
VVV Most recommended