Каталог Iscar токарный инструмент 2017 - страница 390
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
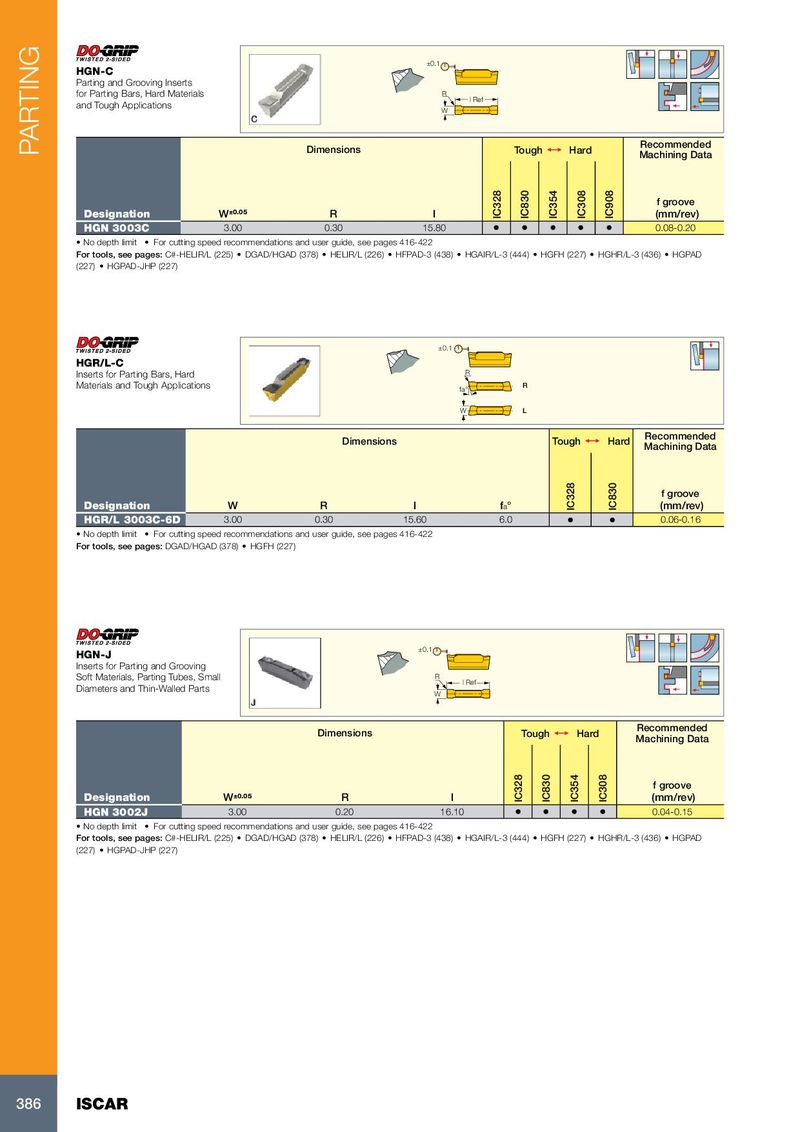
HGN-C ±0.1 Parting and Grooving Inserts for Parting Bars, Hard Materials R and Tough Applications l Ref W
Dimensions
Tough 1 Hard
Recommended Machining Data
f groove
| Designation | W±0.05 | R | l | (mm/rev) | |||||
| HGN 3003C | 3.00 | 0.30 | 15.80 | • | • | • | • | • | 0.08-0.20 |
- No depth limit
- For cutting speed recommendations and user guide, see pages 416-422
For tools, see pages: C#-HELIR/L (225) DGAD/HGAD (378) HELIR/L (226) HFPAD-3 (438) HGAIR/L-3 (444) HGFH (227) HGHR/L-3 (436) HGPAD (227) HGPAD-JHP (227)
±0.1 HGR/L-C Inserts for Parting Bars, Hard R Materials and Tough Applications R fa° W L Dimensions
Tough 1 Hard
Recommended Machining Data
f groove
| Designation | W | R | l | fa° | (mm/rev) | ||
| HGR/L 3003C-6D | 3.00 | 0.30 | 15.60 | 6.0 | • | • | 0.06-0.16 |
- No depth limit
- For cutting speed recommendations and user guide, see pages 416-422
For tools, see pages: DGAD/HGAD (378) HGFH (227)
HGN-J ±0.1 Inserts for Parting and Grooving Soft Materials, Parting Tubes, Small R Diameters and Thin-Walled Parts W
Dimensions
l Ref
Tough 1 Hard
Recommended Machining Data
f groove
| Designation | W±0.05 | R | l | (mm/rev) | ||||
| HGN 3002J | 3.00 | 0.20 | 16.10 | • | • | • | • | 0.04-0.15 |
- No depth limit
- For cutting speed recommendations and user guide, see pages 416-422
For tools, see pages: C#-HELIR/L (225) DGAD/HGAD (378) HELIR/L (226) HFPAD-3 (438) HGAIR/L-3 (444) HGFH (227) HGHR/L-3 (436) HGPAD (227) HGPAD-JHP (227)