Каталог Iscar токарный инструмент 2017 - страница 366
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
GROOVE-TURN
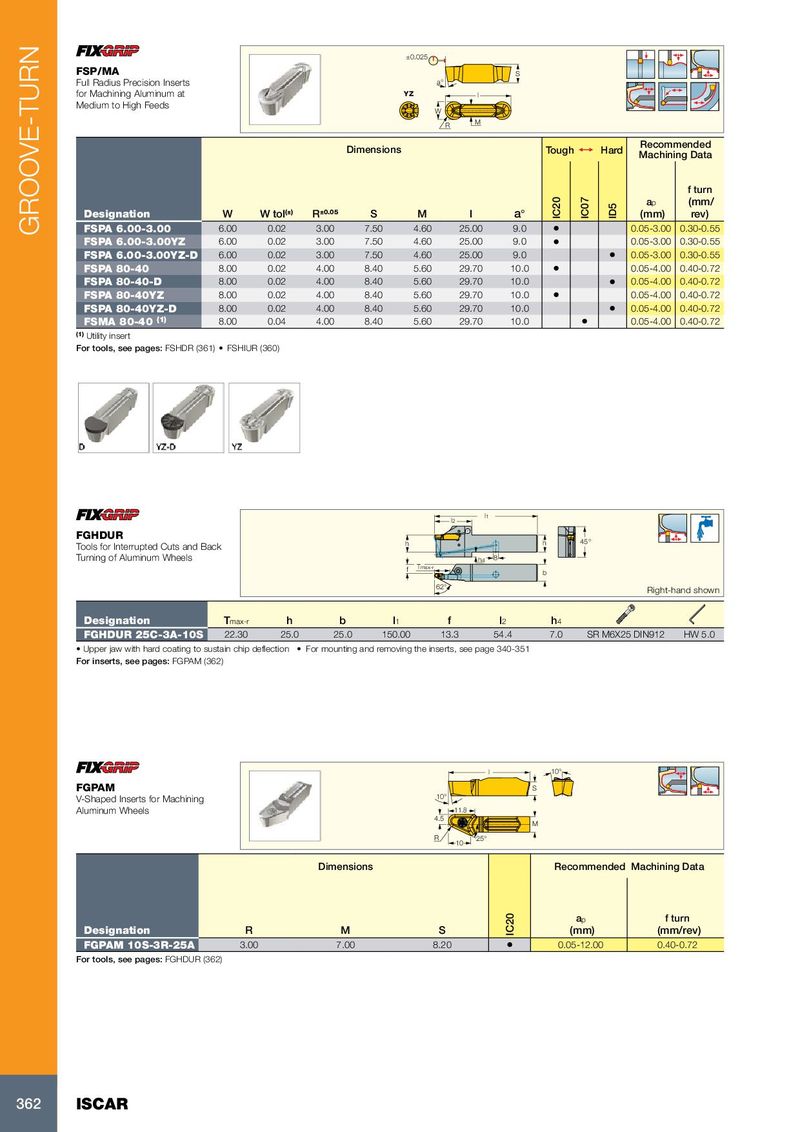
±0.025
FSP/MA S
Full Radius Precision Inserts a°
for Machining Aluminum at YZ l
Medium to High Feeds
W
R M
Recommended
Dimensions Tough 1 Hard
Machining Data
f turn
ap (mm/
IC20
IC07
ID5
Designation W W tol(±) R±0.05 S M l a° (mm) rev)
FSPA 6.00-3.00 6.00 0.02 3.00 7.50 4.60 25.00 9.0 • 0.05-3.00 0.30-0.55
FSPA 6.00-3.00YZ 6.00 0.02 3.00 7.50 4.60 25.00 9.0 • 0.05-3.00 0.30-0.55
FSPA 6.00-3.00YZ-D 6.00 0.02 3.00 7.50 4.60 25.00 9.0 • 0.05-3.00 0.30-0.55
FSPA 80-40 8.00 0.02 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
FSPA 80-40-D 8.00 0.02 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
FSPA 80-40YZ 8.00 0.02 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
FSPA 80-40YZ-D 8.00 0.02 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
FSMA 80-40 (1) 8.00 0.04 4.00 8.40 5.60 29.70 10.0 • 0.05-4.00 0.40-0.72
(1) Utility insert
For tools, see pages: FSHDR (361) • FSHIUR (360)
l1
l2
FGHDUR
h h 45°
Tools for Interrupted Cuts and Back
Turning of Aluminum Wheels h4 8
f Tmax-r
b
62°
Right-hand shown
Designation Tmax-r h b l1 f l2 h4
FGHDUR 25C-3A-10S 22.30 25.0 25.0 150.00 13.3 54.4 7.0 SR M6X25 DIN912 HW 5.0
• Upper jaw with hard coating to sustain chip deflection • For mounting and removing the inserts, see page 340-351
For inserts, see pages: FGPAM (362)
l 10°
FGPAM S
V-Shaped Inserts for Machining 10°
Aluminum Wheels 11.8
4.5
M
R 25°
10
Dimensions Recommended Machining Data
ap f turn
IC20
Designation R M S (mm) (mm/rev)
FGPAM 10S-3R-25A 3.00 7.00 8.20 • 0.05-12.00 0.40-0.72
For tools, see pages: FGHDUR (362)
362 ISCAR