Каталог Iscar токарный инструмент 2017 - страница 362
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
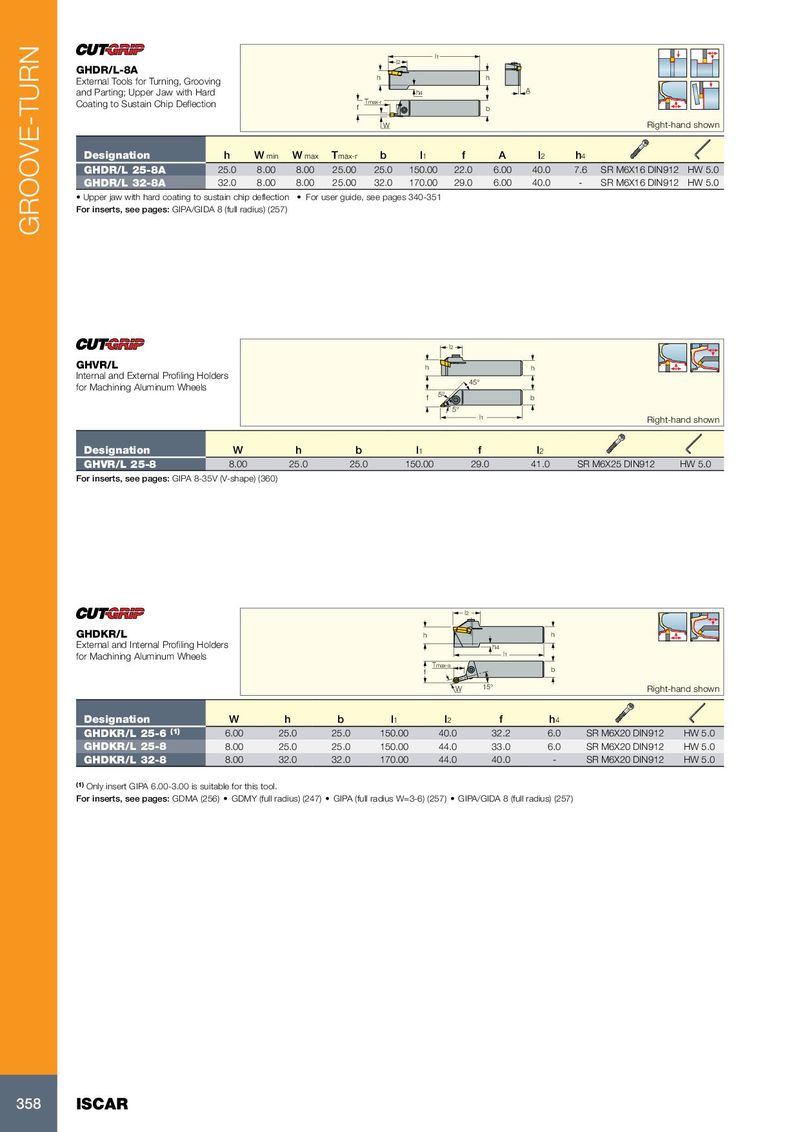
GHDR/L-8A
External Tools for Turning, Grooving h h
| and Parting; Upper Jaw with Hard | h | A | ||||
| Coating to Sustain Chip Deflection | Tmax-r | |||||
| f | b | |||||
| W | Right-hand shown |
| Designation | h | W min | W max | Tmax-r | b | l1 | f | A | l2 | h4 | ||
| GHDR/L 25-8A | 25.0 | 8.00 | 8.00 | 25.00 | 25.0 | 150.00 | 22.0 | 6.00 | 40.0 | 7.6 | SR M6X16 DIN912 HW 5.0 | |
| GHDR/L 32-8A | 32.0 | 8.00 | 8.00 | 25.00 | 32.0 | 170.00 | 29.0 | 6.00 | 40.0 | - | SR M6X16 DIN912 HW 5.0 |
- Upper jaw with hard coating to sustain chip deflection
- For user guide, see pages 340-351
For inserts, see pages: GIPA/GIDA 8 (full radius) (257)
l 2
GHVR/L
h h Internal and External Profiling Holders for Machining Aluminum Wheels 45°
| f | 5° | b | |||
| 5° | |||||
| l1 | Right-hand shown |
| Designation | W | h | b | l1 | f | l2 | ||
| GHVR/L 25-8 | 8.00 | 25.0 | 25.0 | 150.00 | 29.0 | 41.0 | SR M6X25 DIN912 | HW 5.0 |
For inserts, see pages: GIPA 8-35V (V-shape) (360)
| GHDKR/L | l2 h | h | |||||||
| External and Internal Profiling Hol for Machining Aluminum Wheels | ders | f W Tmax-a | l1 h4 15° | b | Right- | hand shown | |||
| Designation | W | h | b | l1 | l2 | f | h4 | ||
| GHDKR/L 25-6(1) | 6.00 | 25.0 | 25.0 | 150.00 | 40.0 | 32.2 | 6.0 | SR M6X20 DIN912 | HW 5.0 |
| GHDKR/L 25-8 | 8.00 | 25.0 | 25.0 | 150.00 | 44.0 | 33.0 | 6.0 | SR M6X20 DIN912 | HW 5.0 |
| GHDKR/L 32-8 | 8.00 | 32.0 | 32.0 | 170.00 | 44.0 | 40.0 | - | SR M6X20 DIN912 | HW 5.0 |
(1) Only insert GIPA 6.00-3.00 is suitable for this tool. For inserts, see pages: GDMA (256) GDMY (full radius) (247) GIPA (full radius W=3-6) (257) GIPA/GIDA 8 (full radius) (257)