Каталог Iscar токарный инструмент 2017 - страница 338
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
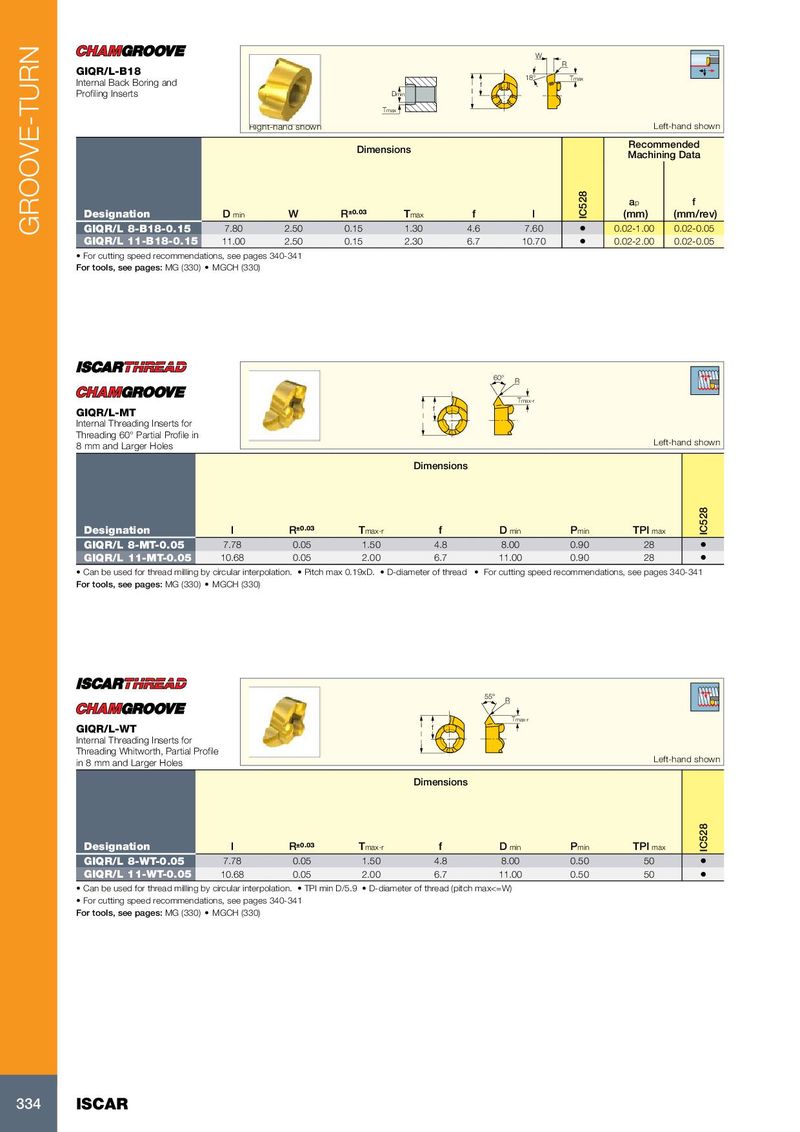
GROOVE-TURN
W
R
GIQR/L-B18 18° Tmax
Internal Back Boring and f
Profiling Inserts Dmin l
Tmax
Right-hand shown Left-hand shown
Recommended
Dimensions
Machining Data
IC528
ap f
Designation D min W R±0.03 Tmax f l (mm) (mm/rev)
GIQR/L 8-B18-0.15 7.80 2.50 0.15 1.30 4.6 7.60 • 0.02-1.00 0.02-0.05
GIQR/L 11-B18-0.15 11.00 2.50 0.15 2.30 6.7 10.70 • 0.02-2.00 0.02-0.05
• For cutting speed recommendations, see pages 340-341
For tools, see pages: MG (330) • MGCH (330)
60°
R
Tmax-r
f
GIQR/L-MT l
Internal Threading Inserts for
Threading 60° Partial Profile in
8 mm and Larger Holes Left-hand shown
Dimensions
IC528
Designation l R±0.03 Tmax-r f D min Pmin TPI max
GIQR/L 8-MT-0.05 7.78 0.05 1.50 4.8 8.00 0.90 28 •
GIQR/L 11-MT-0.05 10.68 0.05 2.00 6.7 11.00 0.90 28 •
• Can be used for thread milling by circular interpolation. • Pitch max 0.19xD. • D-diameter of thread • For cutting speed recommendations, see pages 340-341
For tools, see pages: MG (330) • MGCH (330)
55°
R
Tmax-r
GIQR/L-WT l
f
Internal Threading Inserts for
Threading Whitworth, Partial Profile
in 8 mm and Larger Holes Left-hand shown
Dimensions
IC528
Designation l R±0.03 Tmax-r f D min Pmin TPI max
GIQR/L 8-WT-0.05 7.78 0.05 1.50 4.8 8.00 0.50 50 •
GIQR/L 11-WT-0.05 10.68 0.05 2.00 6.7 11.00 0.50 50 •
• Can be used for thread milling by circular interpolation. • TPI min D/5.9 • D-diameter of thread (pitch max<=W)
• For cutting speed recommendations, see pages 340-341
For tools, see pages: MG (330) • MGCH (330)
334 ISCAR