Каталог Iscar токарный инструмент 2017 - страница 187
Навигация
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмент для обработки алюминиевых колёс
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar расточные системы 2022
 Каталог Iscar высокоточные развертки и метчики 2022
 Токарные инструменты Iscar (часть 2) 2026
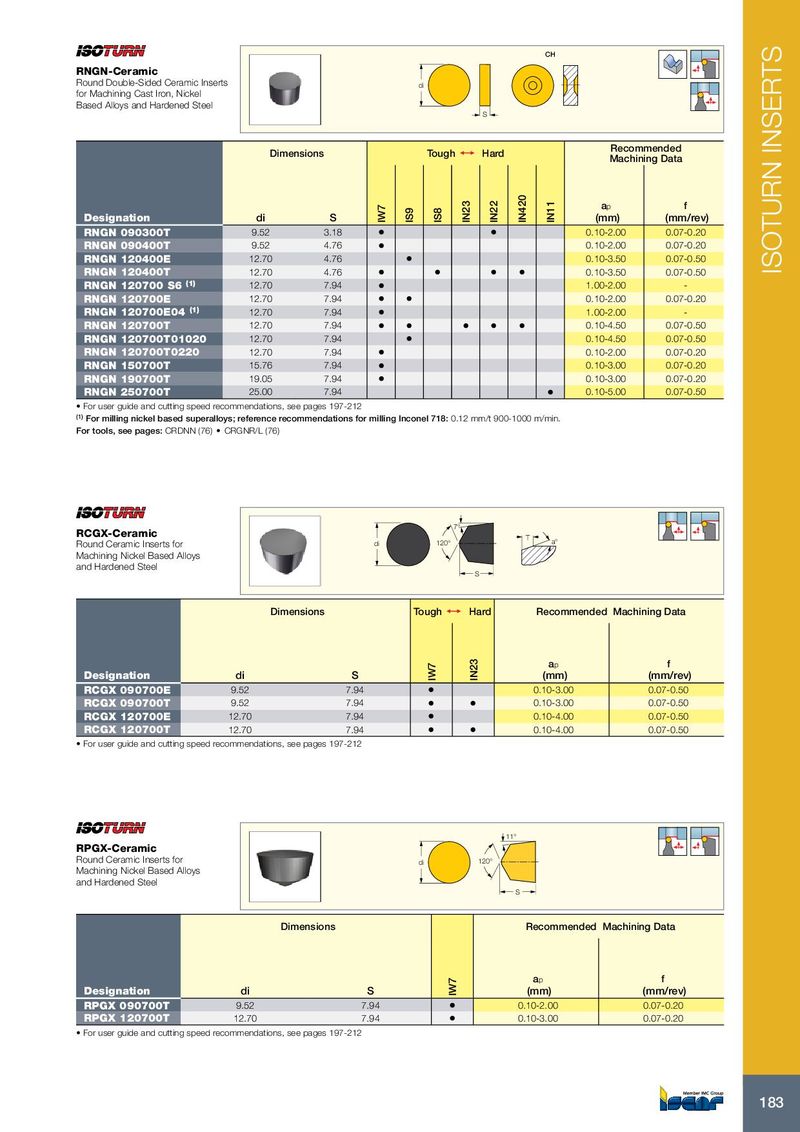
ISOTURN INSERTS
CH
RNGN-Ceramic
Round Double-Sided Ceramic Inserts di
for Machining Cast Iron, Nickel
Based Alloys and Hardened Steel
S
Recommended
Dimensions Tough 1 Hard
Machining Data
IN420
ap f
IN23
IN22
IN11
IW7
IS9
IS8
Designation di S (mm) (mm/rev)
RNGN 090300T 9.52 3.18 • • 0.10-2.00 0.07-0.20
RNGN 090400T 9.52 4.76 • 0.10-2.00 0.07-0.20
RNGN 120400E 12.70 4.76 • 0.10-3.50 0.07-0.50
RNGN 120400T 12.70 4.76 • • • • 0.10-3.50 0.07-0.50
RNGN 120700 S6 (1) 12.70 7.94 • 1.00-2.00 -
RNGN 120700E 12.70 7.94 • • 0.10-2.00 0.07-0.20
RNGN 120700E04 (1) 12.70 7.94 • 1.00-2.00 -
RNGN 120700T 12.70 7.94 • • • • • 0.10-4.50 0.07-0.50
RNGN 120700T01020 12.70 7.94 • 0.10-4.50 0.07-0.50
RNGN 120700T0220 12.70 7.94 • 0.10-2.00 0.07-0.20
RNGN 150700T 15.76 7.94 • 0.10-3.00 0.07-0.20
RNGN 190700T 19.05 7.94 • 0.10-3.00 0.07-0.20
RNGN 250700T 25.00 7.94 • 0.10-5.00 0.07-0.50
• For user guide and cutting speed recommendations, see pages 197-212
(1) For milling nickel based superalloys; reference recommendations for milling Inconel 718: 0.12 mm/t 900-1000 m/min.
For tools, see pages: CRDNN (76) • CRGNR/L (76)
7°
RCGX-Ceramic T
120° a°
Round Ceramic Inserts for di
Machining Nickel Based Alloys
and Hardened Steel
S
Dimensions Tough 1 Hard Recommended Machining Data
ap f
IN23
IW7
Designation di S (mm) (mm/rev)
RCGX 090700E 9.52 7.94 • 0.10-3.00 0.07-0.50
RCGX 090700T 9.52 7.94 • • 0.10-3.00 0.07-0.50
RCGX 120700E 12.70 7.94 • 0.10-4.00 0.07-0.50
RCGX 120700T 12.70 7.94 • • 0.10-4.00 0.07-0.50
• For user guide and cutting speed recommendations, see pages 197-212
11°
RPGX-Ceramic
Round Ceramic Inserts for di 120°
Machining Nickel Based Alloys
and Hardened Steel
S
Dimensions Recommended Machining Data
ap f
IW7
Designation di S (mm) (mm/rev)
RPGX 090700T 9.52 7.94 • 0.10-2.00 0.07-0.20
RPGX 120700T 12.70 7.94 • 0.10-3.00 0.07-0.20
• For user guide and cutting speed recommendations, see pages 197-212
183