Каталог Iscar новые продукты 2018 - страница 72
Навигация
 Каталог Iscar токарные державки ISO 2022
 Каталог Iscar сверла ружейные и для глубокого сверления 2022
 Каталог Iscar монолитные концевые фрезы и система multi-master
 Фрезерные инструменты Iscar 2026
 Каталог Iscar концевые фрезы со сменными пластинами 2022
 Каталог Iscar инструмент для обработки отверстий
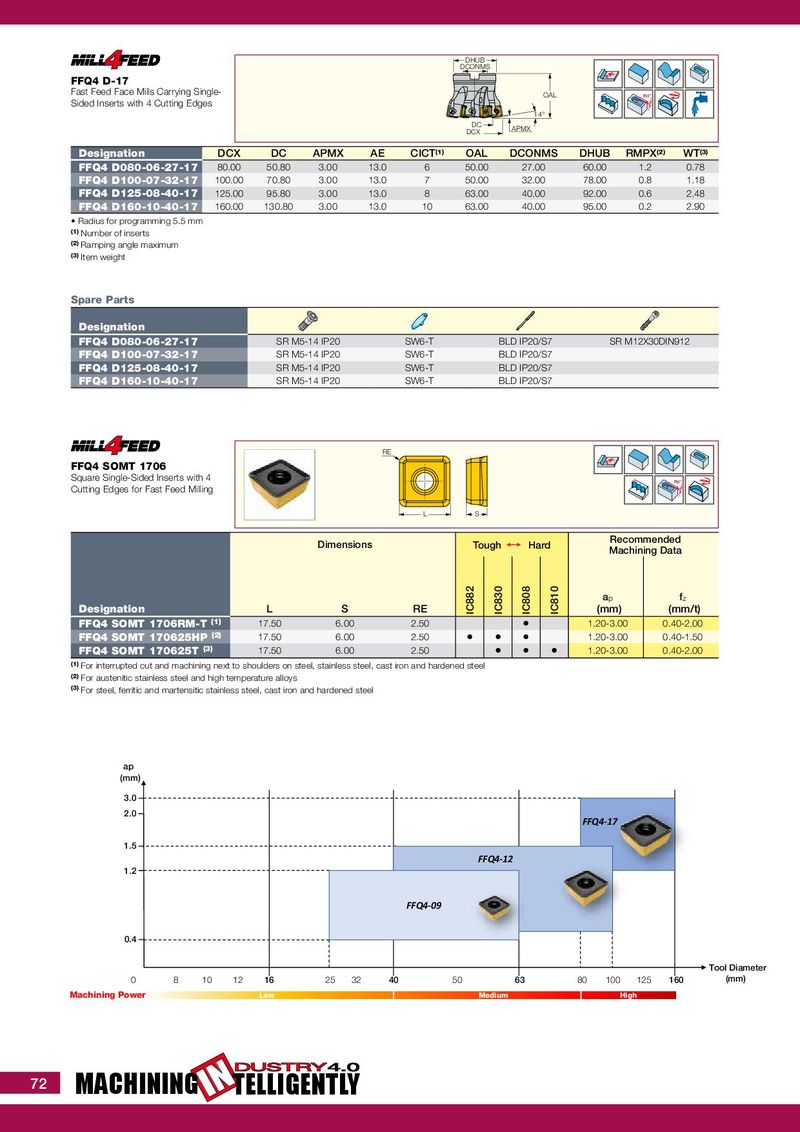
| FFQ4 D-17 | DCONMS DHUB | ||||||||
| Fast Feed Face Mills Carrying Sing Sided Inserts with 4 Cutting Edges | le- | DC DCX | 14° OAL APMX | Rd° | |||||
| Designation | DCX | DC | APMX | AE | CICT(1) OAL | DCONMS | DHUB | RMPX(2) | WT(3) |
| FFQ4 D080-06-27-17 | 80.00 | 50.80 | 3.00 | 13.0 | 6 50.00 | 27.00 | 60.00 | 1.2 | 0.78 |
| FFQ4 D100-07-32-17 | 100.00 | 70.80 | 3.00 | 13.0 | 7 50.00 | 32.00 | 78.00 | 0.8 | 1.18 |
| FFQ4 D125-08-40-17 | 125.00 | 95.80 | 3.00 | 13.0 | 8 63.00 | 40.00 | 92.00 | 0.6 | 2.48 |
| FFQ4 D160-10-40-17 | 160.00 | 130.80 | 3.00 | 13.0 | 10 63.00 | 40.00 | 95.00 | 0.2 | 2.90 |
- Radius for programming 5.5 mm
(1) Number of inserts (2) Ramping angle maximum (3) Item weight
Spare Parts
| Designation | ||||
| FFQ4 D080-06-27-17 | SR M5-14 IP20 | SW6-T | BLD IP20/S7 | SR M12X30DIN912 |
| FFQ4 D100-07-32-17 | SR M5-14 IP20 | SW6-T | BLD IP20/S7 | |
| FFQ4 D125-08-40-17 | SR M5-14 IP20 | SW6-T | BLD IP20/S7 | |
| FFQ4 D160-10-40-17 | SR M5-14 IP20 | SW6-T | BLD IP20/S7 |
FFQ4 SOMT 1706
Square Single-Sided Inserts with 4 Cutting Edges for Fast Feed Milling
RE
Rd°
L S
| Dimensions | To | ugh1 | Ha | rd | Recom Machin | mended ing Data | |||
| Designation | L | S | RE | IC882 | IC830 | IC808 | IC810 | ap (mm) | fz (mm/t) |
| FFQ4 SOMT 1706RM-T(1) | 17.50 | 6.00 | 2.50 | • | 1.20-3.00 | 0.40-2.00 | |||
| FFQ4 SOMT 170625HP(2) | 17.50 | 6.00 | 2.50 | • | • | • | 1.20-3.00 | 0.40-1.50 | |
| FFQ4 SOMT 170625T(3) | 17.50 | 6.00 | 2.50 | • | • | • | 1.20-3.00 | 0.40-2.00 |
(1) For interrupted cut and machining next to shoulders on steel, stainless steel, cast iron and hardened steel (2) For austenitic stainless steel and high temperature alloys (3) For steel, ferritic and martensitic stainless steel, cast iron and hardened steel
ap (mm) 3.0 2.0
1.5 1.2
0.4
0 Machining Power
8
10
12
16 Low
25
32
FFQ4-09
40 50
FFQ4-17
FFQ4-12
Tool Diameter
63 80 100 125 160 (mm)
Medium High