Каталог Iscar новые продукты 2018 - страница 71
Навигация
 Каталог Iscar токарные державки ISO 2022
 Каталог Iscar сверла ружейные и для глубокого сверления 2022
 Каталог Iscar монолитные концевые фрезы и система multi-master
 Фрезерные инструменты Iscar 2026
 Каталог Iscar концевые фрезы со сменными пластинами 2022
 Каталог Iscar инструмент для обработки отверстий
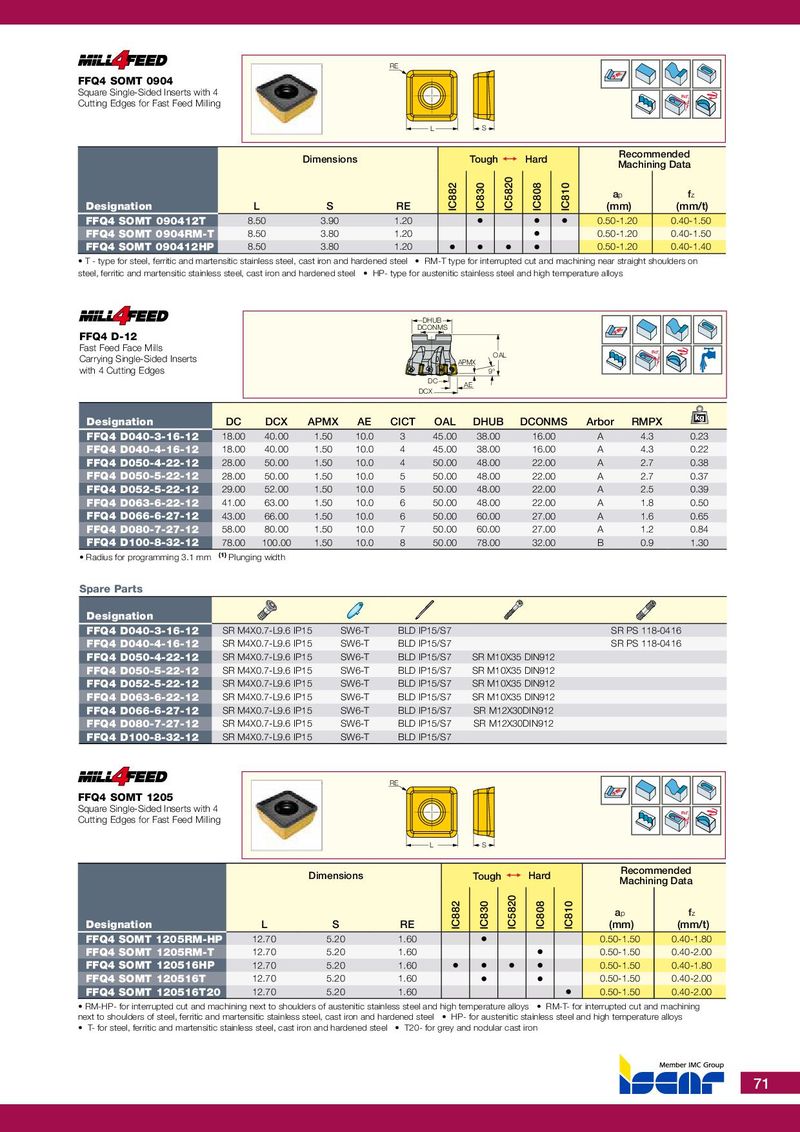
FFQ4 SOMT 0904
Square Single-Sided Inserts with 4 Cutting Edges for Fast Feed Milling Rd°
L S Recommended Dimensions Tough 1 Hard Machining Data ap fz
| Designation | L | S | RE | (mm) | (mm/t) | |||||
| FFQ4 SOMT 090412T | 8.50 | 3.90 | 1.20 | • | • | • | 0.50-1.20 | 0.40-1.50 | ||
| FFQ4 SOMT 0904RM-T | 8.50 | 3.80 | 1.20 | • | 0.50-1.20 | 0.40-1.50 | ||||
| FFQ4 SOMT 090412HP | 8.50 | 3.80 | 1.20 | • | • | • | • | 0.50-1.20 | 0.40-1.40 |
- T - type for steel, ferritic and martensitic stainless steel, cast iron and hardened steel
- RM-T type for interrupted cut and machining near straight shoulders on
steel, ferritic and martensitic stainless steel, cast iron and hardened steel HP- type for austenitic stainless steel and high temperature alloys
| FFQ4 D-12 | DCONMS DHUB | |||||||||
| Fast Feed Face Mills Carrying Single-Sided Inserts with 4 Cutting Edges | DC A AP DCX | E MX 9° OAL | Rd° | |||||||
| Designation | DC | DCX | APMX | AE | CICT OAL | DHUB | DCONMS | Arbor | RMPX | kg |
| FFQ4 D040-3-16-12 | 18.00 | 40.00 | 1.50 | 10.0 | 3 45.00 | 38.00 | 16.00 | A | 4.3 | 0.23 |
| FFQ4 D040-4-16-12 | 18.00 | 40.00 | 1.50 | 10.0 | 4 45.00 | 38.00 | 16.00 | A | 4.3 | 0.22 |
| FFQ4 D050-4-22-12 | 28.00 | 50.00 | 1.50 | 10.0 | 4 50.00 | 48.00 | 22.00 | A | 2.7 | 0.38 |
| FFQ4 D050-5-22-12 | 28.00 | 50.00 | 1.50 | 10.0 | 5 50.00 | 48.00 | 22.00 | A | 2.7 | 0.37 |
| FFQ4 D052-5-22-12 | 29.00 | 52.00 | 1.50 | 10.0 | 5 50.00 | 48.00 | 22.00 | A | 2.5 | 0.39 |
| FFQ4 D063-6-22-12 | 41.00 | 63.00 | 1.50 | 10.0 | 6 50.00 | 48.00 | 22.00 | A | 1.8 | 0.50 |
| FFQ4 D066-6-27-12 | 43.00 | 66.00 | 1.50 | 10.0 | 6 50.00 | 60.00 | 27.00 | A | 1.6 | 0.65 |
| FFQ4 D080-7-27-12 | 58.00 | 80.00 | 1.50 | 10.0 | 7 50.00 | 60.00 | 27.00 | A | 1.2 | 0.84 |
| FFQ4 D100-8-32-12 | 78.00 | 100.00 | 1.50 | 10.0 | 8 50.00 | 78.00 | 32.00 | B | 0.9 | 1.30 |
- Radius for programming 3.1 mm (1) Plunging width
Spare Parts
| Designation | |||||
| FFQ4 D040-3-16-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 | SR PS 118-0416 | |
| FFQ4 D040-4-16-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 | SR PS 118-0416 | |
| FFQ4 D050-4-22-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 | SR M10X35 DIN912 | |
| FFQ4 D050-5-22-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 | SR M10X35 DIN912 | |
| FFQ4 D052-5-22-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 | SR M10X35 DIN912 | |
| FFQ4 D063-6-22-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 | SR M10X35 DIN912 | |
| FFQ4 D066-6-27-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 | SR M12X30DIN912 | |
| FFQ4 D080-7-27-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 | SR M12X30DIN912 | |
| FFQ4 D100-8-32-12 | SR M4X0.7-L9.6 IP15 | SW6-T | BLD IP15/S7 |
| FQ4 SOMT 1205 quare Single-Sided Inserts with 4 utting Edges for Fast Feed Milling | RE | L | S | Rd° | |||||
| Dimensions | Tough | 1 | Hard | Recomm Machinin | ended g Data | ||||
| Designation | L S | RE | IC882 | IC830 | IC5820 | IC808 | IC810 | ap (mm) | fz (mm/t) |
| FFQ4 SOMT 1205RM-HP | 12.70 5.20 | 1.60 | • | 0.50-1.50 | 0.40-1.80 | ||||
| FFQ4 SOMT 1205RM-T | 12.70 5.20 | 1.60 | • | 0.50-1.50 | 0.40-2.00 | ||||
| FFQ4 SOMT 120516HP | 12.70 5.20 | 1.60 | • | • | • | • | 0.50-1.50 | 0.40-1.80 | |
| FFQ4 SOMT 120516T | 12.70 5.20 | 1.60 | • | • | 0.50-1.50 | 0.40-2.00 | |||
| FFQ4 SOMT 120516T20 | 12.70 5.20 | 1.60 | • | 0.50-1.50 | 0.40-2.00 |
- RM-HP- for interrupted cut and machining next to shoulders of austenitic stainless steel and high temperature alloys
- RM-T- for interrupted cut and machining
next to shoulders of steel, ferritic and martensitic stainless steel, cast iron and hardened steel HP- for austenitic stainless steel and high temperature alloys
- T- for steel, ferritic and martensitic stainless steel, cast iron and hardened steel
- T20- for grey and nodular cast iron