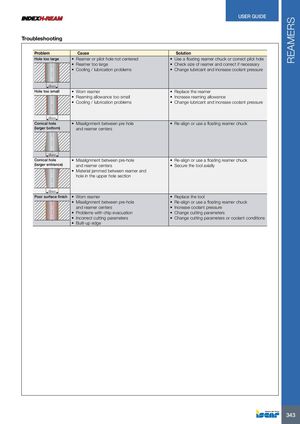
| Problem | Cause | Solution |
| Hole too large | • Reamer or pilot hole not centered | • Use a floating reamer chuck or correct pilot hole |
| dnom | • Reamer too large • Cooling / lubrication problems | • Check size of reamer and correct if necessary • Change lubricant and increase coolant pressure |
| Hole too small | • Worn reamer | • Replace the reamer |
| dnom | • Reaming allowance too small • Cooling / lubrication problems | • Increase reaming allowance • Change lubricant and increase coolant pressure |
| Conical hole (larger bottom) | • Misalignment between pre hole and reamer centers | • Re-align or use a floating reamer chuck |
| dnom | | |
| Conical hole (larger entrance) dnom | • Misalignment between pre-hole and reamer centers • Material jammed between reamer and hole in the upper hole section | • Re-align or use a floating reamer chuck • Secure the tool axially |
| Poor surface finish | • Worn reamer • Misalignment between pre-hole and reamer centers • Problems with chip evacuation • Incorrect cutting parameters • Built-up edge | • Replace the tool • Re-align or use a floating reamer chuck • Increase coolant pressure • Change cutting parameters • Change cutting parameters or coolant conditions |
 Токарные инструменты Iscar (часть 2) 2026
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar крепление инструмента
 Каталог Iscar токарные пластины ISO 2022
 Руководство Iscar режущий инструмент в производстве штампов и пресс-форм