Каталог Iscar высокоточные развертки и метчики 2022 - страница 32
Навигация
 Токарные инструменты Iscar (часть 2) 2026
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar державки и пластины для нарезания резьбы 2022
 Каталог Iscar крепление инструмента
 Каталог Iscar токарные пластины ISO 2022
 Руководство Iscar режущий инструмент в производстве штампов и пресс-форм
H-REAM Cutting Conditions
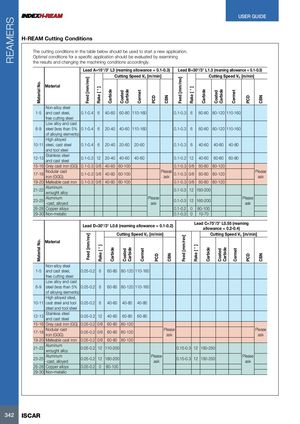
The cutting conditions in the table below should be used to start a new application. Optimal conditions for a specific application should be evaluated by examining the results and changing the machining conditions accordingly.
| Material No. | Material | Lead A Feed [mm/rev] | =15° Rake [ ° ] | /3° L3 (r C Carbide | eaming utting Sp Coated Carbide | allowanc eed Vc [ Cermet | e = 0. m/min] PCD | 1-0.3) CBN | Lead Feed [mm/rev] | B=30 Rake [ ° ] | °/3° L1.3 Cu Carbide | (reamin tting Sp Coated Carbide | g allowan eed Vc Cermet | ce = 0. [m/min PCD | 1-0.3) ] CBN |
| 1-5 | Non-alloy steel and cast steel, free cutting steel | 0.1-0.4 | 6 | 40-60 | 60-80 | 110-160 | 0.1-0.3 | 6 | 60-80 | 80-120 | 110-160 | ||||
| 6-9 | Low alloy and cast steel (less than 5% of alloying elements) | 0.1-0.4 | 6 | 20-40 | 40-60 | 110-160 | 0.1-0.3 | 6 | 60-80 | 80-120 | 110-160 | ||||
| 10-11 | High alloyed steel, cast steel and tool steel | 0.1-0.4 | 6 | 20-40 | 20-60 | 20-60 | 0.1-0.3 | 6 | 40-60 | 40-80 | 40-80 | ||||
| 12-13 | Stainless steel and cast steel | 0.1-0.3 | 12 | 20-40 | 40-60 | 40-60 | 0.1-0.2 | 12 | 40-60 | 60-80 | 60-80 | ||||
| 15-16 | Grey cast iron (GG) | 0.1-0.3 | 0/6 | 40-60 | 60-100 | 0.1-0.3 | 0/6 | 60-80 | 80-120 | ||||||
| 17-18 | Nodular cast iron (GGG) | 0.1-0.3 | 0/6 | 40-60 | 60-100 | Please ask | 0.1-0.3 | 0/6 | 60-80 | 80-120 | Please ask | ||||
| 19-20 | Malleable cast iron | 0.1-0.3 | 0/6 | 40-60 | 60-100 | 0.1-0.3 | 0/6 | 60-80 | 80-120 | ||||||
| 21-22 | Aluminum wrought alloy | 0.1-0.3 | 12 | 160-200 | |||||||||||
| 23-25 | Aluminum -cast alloyed | Please ask | 0.1-0.3 | 12 | 160-200 | Please ask | |||||||||
| 26-28 | , Copper alloys | 01-02 | 0 | 80-100 | |||||||||||
| 29-30 | Non-metallic | .. 0.1-0.3 | 0 | 10-70 | |||||||||||
| Lead D | =30° | /3° L0.6 | (reamin | g allowa | nce = 0 | .1-0.2) | L | ead C=75 allow | °/3° L0. ance = | 55 (rea 0.2-0.4) | ming | ||||
| Material No. | Material | Feed [mm/rev] | Rake [ ° ] | C Carbide | utting S Coated Carbide | peed Vc Cermet | [m/mi PCD | n] CBN | Feed [mm/rev] | Rake [ ° ] | C Carbide | utting S Coated Carbide | peed Vc Cermet | [m/mi PCD | n] CBN |
| 1-5 | Non-alloy steel and cast steel, free cutting steel | 0.05-0.2 | 6 | 60-80 | 80-120 | 110-160 | |||||||||
| 6-9 | Low alloy and cast steel (less than 5% of alloying elements) | 0.05-0.2 | 6 | 60-80 | 80-120 | 110-160 | |||||||||
| 10-11 | High alloyed steel, cast steel and tool steel and tool steel | 0.05-0.2 | 6 | 40-60 | 40-80 | 40-80 | |||||||||
| 12-13 | Stainless steel and cast steel | 0.05-0.2 | 12 | 40-60 | 60-80 | 60-80 | |||||||||
| 15-16 | Grey cast iron (GG) | 0.05-0.2 | 0/6 | 60-80 | 80-120 | ||||||||||
| Nodular cast | Pleas | e | Please | ||||||||||||
| 17-18 | iron (GGG) | 0.05-0.2 | 0/6 | 60-80 | 80-120 | ask | ask | ||||||||
| 19-20 | Malleable cast iron | 0.05-0.2 | 0/6 | 60-80 | 80-120 | ||||||||||
| 21-22 | Aluminum wrought alloy | 0.05-0.2 | 12 | 110-200 | 0.15-0 | .3 1 | 2 150-25 | 0 | |||||||
| 23-25 | Aluminum -cast, alloyed | 0.05-0.2 | 12 | 180-200 | Pleas ask | e | 0.15-0 | .3 1 | 2 150-25 | 0 | Please ask | ||||
| 2628 | C ll | 00502 | 0 | 80100 | |||||||||||
| - 29-30 | opper aoys Non-metallic | .-. | - |