Каталог Iscar сверла со сменной режущей частью 2022 - страница 74
Навигация
 Каталог Iscar монолитные фрезы 2022
 Каталог Iscar токарный инструмент
 Каталог Iscar инструмент для мелкоразмерной обработки
 Каталог Iscar токарный инструмент для нарезания канавок
 Каталог Iscar полирующие фрезы
 Каталог Iscar дисковые фрезы и фрезерные пластины 2022
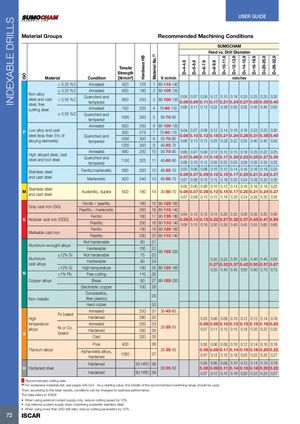
| ISO Mater | ial | Condition | Tensile Strength [N/mm2] | Hardness HB | Material No.(1) | V m/min | D=4-4.9 | D=5-5.9 | D=6-7.9 | S Feed D=8-9.9 | UMO vs. D D=10-11.9 | CHA rill Di D=12-13.9 mm | M amete D=14-15.9 /rev | r D=16-19.9 | D=20-25.9 | D=26-32.9 |
| < 0.25 %C | Annealed | 420 | 125 | 1 8 | 0-110-140 | |||||||||||
| Non-allo | ≥ 0.25 %C | Annealed | 650 | 190 | 2 8 | 0-105-130 | ||||||||||
| y steel and cast tl fr | < 0.55 %C | Quenched and tempered | 850 | 250 | 3 8 | 0-100-120 | 0.04 0.06 | 0.07 0.09 | 0.09 0.11 | 0.12 0.17 | 0.15 0.21 | 0.18 0.24 | 0.20 0.27 | 0.25 0.35 | 0.25 0.35 | 0.30 0.40 |
| see, ee cutting steel | Annealed | 750 | 220 | 4 | 70-90-110 | 0.08 | 0.11 | 0.13 | 0.22 | 0.28 | 0.30 | 0.35 | 0.45 | 0.45 | 0.50 | |
| ≥ 0.55 %C | Quenched and tempered | 1000 | 300 | 5 | 50-70-90 | |||||||||||
| Low alloy and ca | st | Annealed | 600 | 200 | 6 8 | 0-100-120 | 004 | 007 | 009 | 012 | 014 | 016 | 018 | 023 | 025 | 030 |
| P steel (less than 5 alloying elements | % of ) | Quenched and tempered | 930 1000 1200 | 275 300 350 | 7 8 9 | 70-90-110 50-70-90 40-55-70 | . 0.06 0.08 | . 0.10 0.13 | . 0.12 0.15 | . 0.18 0.25 | . 0.21 0.28 | . 0.24 0.32 | . 0.26 0.35 | . 0.31 0.40 | . 0.35 0.45 | . 0.40 0.50 |
| High alloyed stee steel and tool ste | l, cast el | Annealed Quenched and tempered | 680 1100 | 200 325 | 10 11 | 50-70-90 40-60-80 | 0.06 0.07 0.08 | 0.07 0.09 0.10 | 0.09 0.11 0.12 | 0.12 0.16 0.20 | 0.12 0.17 0.22 | 0.15 0.20 0.25 | 0.18 0.23 0.28 | 0.20 0.25 0.30 | 0.22 0.27 0.33 | 0.25 0.30 0.35 |
| Stainless steel | Ferritic/martensitic | 680 | 200 | 12 | 40-55-70 | 0.05 006 | 0.06 007 | 0.08 00 | 0.10 012 | 0.12 01 | 0.14 017 | 0.16 020 | 0.16 021 | 0.18 024 | 0.20 027 | |
| and cast steel | Martensitic | 820 | 240 | 13 | 40-55-70 | . 0.07 | . 0.08 | . 0.10 | . 0.15 | . 0.18 | . 0.20 | . 0.24 | . 0.26 | . 0.30 | . 0.35 | |
| M Stainless steel and cast steel | Austenitic, duplex | 600 | 180 | 14 | 30-50-70 | 0.05 0.06 0.07 | 0.06 0.07 0.08 | 0.08 0.09 0.10 | 0.10 0.12 0.15 | 0.12 0.15 0.18 | 0.14 0.17 0.20 | 0.16 0.20 0.24 | 0.16 0.21 0.26 | 0.18 0.24 0.30 | 0.20 0.27 0.35 | |
| Ferritic /pearlitic | 180 | 159 | 0-125-160 | |||||||||||||
| Gray cast iron (G | G) | |||||||||||||||
| Pearlitic / martensitic | 260 | 16 8 | 0-110-140 | 004 | 010 | 012 | 015 | 020 | 025 | 030 | 035 | 035 | 040 | |||
| Ferritic | 160 | 17 9 | 0-135-180 | . | . | . | . | . | . | . | . | . | . | |||
| K Nodular cast iron | (GGG) | 0.06 | 0.13 | 0.15 | 0.22 | 0.27 | 0.32 | 0.37 | 0.45 | 0.47 | 0.50 | |||||
| Pearlitic | 250 | 18 8 | 0-110-140 | 008 | 01 | 01 | 030 | 03 | 040 | 04 | 0 | 060 | 060 | |||
| Ferritic | 130 | 19 9 | 0-125-160 | . | .5 | . | . | .5 | . | .5 | .55 | . | . | |||
| Malleable cast ir | on | |||||||||||||||
| Pearlitic | 230 | 20 8 | 0-110-140 | |||||||||||||
| Aluminum-wroug | ht alloys | Not hardenable Hardenable | 60 100 | 21 22 | 22 | |||||||||||
| Aluminum- | ≤12% Si | Not hardenable Hardenable | 75 90 | 23 24 | 0-155-0 | 0.20 | 0.25 | 0.30 | 0.35 | 0.40 | 0.45 | 0.50 | ||||
| cast alloys | 027 | 032 | 037 | 042 | 050 | 057 | 067 | |||||||||
| >12% Si | High temperature | 130 | 25 8 | 0-120-160 | . 0.35 | . 0.40 | . 0.45 | . 0.50 | . 0.60 | . 0.70 | . 0.75 | |||||
| N | >1% Pb | Free cuttin | 110 | 26 | ||||||||||||
| Copper alloys | g Brass | 90 | 9 27 | 0-155-220 | ||||||||||||
| Electrolytic copper | 100 | 28 | ||||||||||||||
| Non metallic | Duroplastics, fiberplastics | 29 | ||||||||||||||
| Hard rubber | 30 | |||||||||||||||
| Fe based | Annealed | 200 | 31 | 30-45-60 | ||||||||||||
| Hardened | 280 | 32 | ||||||||||||||
| High | 0.05 | 0.06 | 0.08 | 0.10 | 0.12 | 0.12 | 0.14 | 0.16 | ||||||||
| temperature | Annealed | 250 | 33 | 0.06 | 0.08 | 0.10 | 0.12 | 0.15 | 0.16 | 0.18 | 0.20 | |||||
| alloys | Ni or Co | Hardened | 350 | 34 | 20-35-50 | 0.07 | 0.11 | 0.13 | 0.15 | 0.18 | 0.20 | 0.22 | 0.25 | |||
| S | based | Cast | 320 | 35 | ||||||||||||
| Pure | 400 | 36 | 0.05 | 0.06 | 0.08 | 0.10 | 0.12 | 0.14 | 0.16 | 0.18 | ||||||
| Titanium alloys | Alpha+beta alloys, hardened | 1050 | 37 | 20-35-50 | 0.06 0.07 | 0.09 0.12 | 0.11 0.15 | 0.14 0.18 | 0.16 0.20 | 0.18 0.22 | 0.20 0.25 | 0.22 0.27 | ||||
| HH l | Hardened | 55 HRC | 38 | 2 | 0.05 | 0.06 | 0.08 | 0.10 | 0.12 | 0.14 | 0.16 2 | 0.18 22 | ||||
| ardened stee | Hardened | 60 HRC | 39 | 0-35-50 | 0.0 0.07 | 0.09 0.12 | 0.1 0.15 | 0.1 0.18 | 0.16 0.20 | 0.18 0.22 | 0.0 0.25 | 0. 0.27 |
Recommended cutting data (1) For workpiece materials list, see pages 495-524 . As a starting value, the middle of the recommended machining range should be used. Then, according to the wear results, conditions can be changed to optimize performance. The data refers to IC908
- When using external coolant supply only, reduce cutting speed by 10%
- Use internal coolant supply when machining austenitic stainless steel
- When using more than 5XD drill ratio, reduce cutting parameters by 10%