Каталог Iscar сверла со сменной режущей частью 2022 - страница 128
Навигация
 Каталог Iscar монолитные фрезы 2022
 Каталог Iscar токарный инструмент
 Каталог Iscar инструмент для мелкоразмерной обработки
 Каталог Iscar токарный инструмент для нарезания канавок
 Каталог Iscar полирующие фрезы
 Каталог Iscar дисковые фрезы и фрезерные пластины 2022
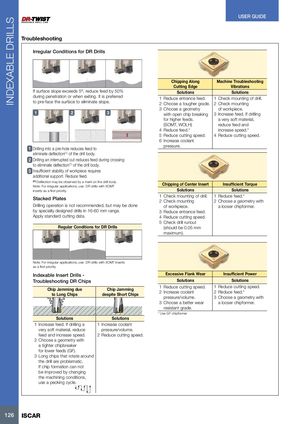
Troubleshooting
Irregular Conditions for DR Drills
Chipping Along Machine Troubleshooting Cutting Edge Vibrations
If surface slope exceeds 5º, reduce feed by 50% Solutions Solutions
| during penetration or when exiting. It is preferred | 1 Reduce entrance feed. | 1 Check mounting of drill. | ||||
| to pre-face the surface to eliminate slope. | 2 Choose a tougher grade. | 2 Check mounting | ||||
| 3 Choose a geometry | of workpiece. | |||||
| 1 | 2 | 3 | with open chip breaking | 3 Increase feed. If drilling |
for higher feeds. a very soft material, (SOMT, WOLH) reduce feed and 4 Reduce feed.* increase speed.* 5 Reduce cutting speed. 4 Reduce cutting speed.
6 Increase coolant pressure. 1 Drilling into a pre-hole reduces feed to eliminate deflection (1) of the drill body. 2 Drilling an interrupted cut reduces feed during crossing to eliminate deflection (1) of the drill body. 3 Insufficient stability of workpiece requires additional support. Reduce feed.
| (1) Deflection may be observed by a mark on the drill body. | Chipping of Center Insert | Insufficient Torque |
| Note: For irregular applications, use DR drills with XOMT |
inserts as a first priority. Solutions Solutions
| Stacked Plates | 1 Check mounting of drill. | 1 Reduce feed.* |
| 2 Check mounting | 2 Choose a geometry with |
Drilling operation is not recommended, but may be done of workpiece. a looser chipformer.
by specially designed drills in 16-60 mm range. 3 Reduce entrance feed. Apply standard cutting data. 4 Reduce cutting speed. 5 Check drill runout Regular Conditions for DR Drills (should be 0.05 mm
maximum).
Note: For irregular applications, use DR drills with XOMT inserts as a first priority.
Indexable Insert Drills -
Troubleshooting DR Chips
Chip Jamming due Chip Jamming to Long Chips despite Short Chips
Solutions Solutions 1 Increase feed. If drilling a 1 Increase coolant very soft material, reduce pressure/volume. feed and increase speed. 2 Reduce cutting speed. 2 Choose a geometry with a tighter chipbreaker for lower feeds (GF). 3 Long chips that rotate around the drill are problematic. If chip formation can not be improved by changing the machining conditions, use a pecking cycle.
Excessive Flank Wear Insufficient Power Solutions Solutions 1 Reduce cutting speed. 1 Reduce cutting speed. 2 Increase coolant 2 Reduce feed.* pressure/volume. 3 Choose a geometry with 3 Choose a better wear a looser chipformer. resistant grade. * Use GF chipformer