Каталог Iscar сверла со сменной режущей частью 2022 - страница 105
Навигация
 Каталог Iscar монолитные фрезы 2022
 Каталог Iscar токарный инструмент
 Каталог Iscar инструмент для мелкоразмерной обработки
 Каталог Iscar токарный инструмент для нарезания канавок
 Каталог Iscar полирующие фрезы
 Каталог Iscar дисковые фрезы и фрезерные пластины 2022
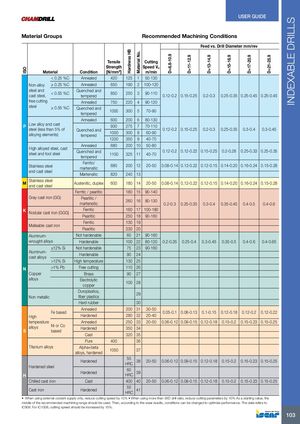
| ISO Material | Condition | Tensile Strength [N/mm2] | Hardness HB | Material No. | Cutting Speed Vc m/min | D=6.8-10.9 | D=11-12.9 | Feed vs. D D=13-14.9 | rill Diamet D=15-16.9 | er mm/rev D=17-20.9 | D=21-25.9 |
| < 0.25 %C | Annealed | 420 | 125 | 1 | 50-130 | ||||||
| Non-alloy ≥ 0.25 %C | Annealed | 650 | 190 | 2 | 100-120 | ||||||
| steel and cast steel, < 0.55 %C | Quenched and tempered | 850 | 250 | 3 | 90-110 | 0.12-0.2 | 0.15-0.25 | 0.2-0.3 | 0.25-0.35 | 0.25-0.45 | 0.25-0.45 |
| free cutting steel ≥ 0.55 %C | Annealed Quenched and tempered | 750 1000 | 220 300 | 4 5 | 90-120 70-90 | ||||||
| Low alloy and cast | Annealed | 600 | 200 | 6 | 80-130 | ||||||
| P steel (less than 5% of alloying elements) | Quenched and tempered | 930 1000 1200 | 275 300 350 | 7 8 9 | 70-110 60-90 40-70 | 0.12-0.2 | 0.15-0.25 | 0.2-0.3 | 0.25-0.35 | 0.3-0.4 | 0.3-0.45 |
| High alloyed steel, cast steel and tool steel | Annealed Quenched and tempered | 680 1100 | 200 325 | 10 11 | 50-80 40-70 | 0.12-0.2 | 0.12-0.22 | 0.15-0.25 | 0.2-0.28 | 0.25-0.33 | 0.25-0.35 |
| Stainless steel | Ferritic/ martensitic | 680 | 200 | 12 | 20-50 | 0.08-0.14 | 0.12-0.22 | 0.12-0.15 | 0.14-0.20 | 0.16-0.24 | 0.15-0.28 |
| and cast steel | Martensitic | 820 | 240 | 13 | |||||||
| M Stainless steel and cast steel | Austenitic, duplex | 600 | 180 | 14 | 20-50 | 0.08-0.14 | 0.12-0.22 | 0.12-0.15 | 0.14-0.20 | 0.16-0.24 | 0.15-0.28 |
| Ferritic /pearlitic | 180 | 15 | 90-140 | ||||||||
| Gray cast iron (GG) | Pearlitic / martensitic | 260 | 16 | 80-130 | 0.2-0.3 | 0.25-0.35 | 0.3-0.4 | 0.35-0.45 | 0.4-0.5 | 0.4-0.6 | |
| K | Ferritic | 160 | 17 | 100-180 | |||||||
| Nodular cast iron (GGG) | Pearlitic | 250 | 18 | 90-160 | |||||||
| Ferritic | 130 | 19 | |||||||||
| Malleable cast iron | Pearlitic | 230 | 20 | ||||||||
| Aluminum- | Not hardenable | 60 | 21 | 90-160 | |||||||
| wrought alloys | Hardenable | 100 | 22 | 80-120 | 0.2-0.35 | 0.25-0.4 | 0.3-0.45 | 0.35-0.5 | 0.4-0.6 | 0.4-0.65 | |
| Aluminum- ≤12% Si | Not hardenable | 75 | 23 | 90-160 | |||||||
| Hardenable | 90 | 24 | |||||||||
| cast alloys | |||||||||||
| >12% Si | High temperature | 130 | 25 | ||||||||
| N >1% Pb | Free cutting | 110 | 26 | ||||||||
| Copper | Brass | 90 | 27 | ||||||||
| alloys | Electrolytic copper | 100 | 28 | ||||||||
| Non metallic | Duroplastics, fiberplastics | 29 | |||||||||
| Hard rubber | 30 | ||||||||||
| Fe based | Annealed | 200 | 31 | 30-50 | 005-01 | 008-013 | 01-015 | 012-018 | 012-02 | 012-022 | |
| High | Hardened | 280 | 32 | 20-40 | .. | .. | .. | .. | .. | .. | |
| temperature | Annealed | 250 | 33 | 20-50 | 0.06-0.12 | 0.09-0.15 | 0.12-0.18 | 0.15-0.2 | 0.15-0.23 | 0.15-0.25 | |
| S alloys Ni or Co | Hardened | 350 | 34 | ||||||||
| based | Cast | 320 | 35 | ||||||||
| Pure | 400 | 36 | |||||||||
| Titanium alloys | Alpha+beta alloys,hardened | 1050 | 37 | ||||||||
| Hardened | 55 HRC | 38 | 20-50 | 0.06-0.12 | 0.09-0.15 | 0.12-0.18 | 0.15-0.2 | 0.15-0.23 | 0.15-0.25 | ||
| H Hardened steel | Hardened | 60 HRC | 39 | ||||||||
| Chilled cast iron | Cast | 400 | 40 | 20-50 | 0.06-0.12 | 0.09-0.15 | 0.12-0.18 | 0.15-0.2 | 0.15-0.23 | 0.15-0.25 | |
| Cast iron | Hardened | 55 HRC | 41 |
- When using external coolant supply only, reduce cutting speed by 10%
- When using more than 5XD drill ratio, reduce cutting parameters by 10% As a starting value, the
middle of the recommended machining range should be used. Then, according to the wear results, conditions can be changed to optimize performance. The data refers to IC908. For IC1008, cutting speed should be increased by 15%.