Каталог Iscar сверла со сменной режущей частью 2022 - страница 104
Навигация
 Каталог Iscar монолитные фрезы 2022
 Каталог Iscar токарный инструмент
 Каталог Iscar инструмент для мелкоразмерной обработки
 Каталог Iscar токарный инструмент для нарезания канавок
 Каталог Iscar полирующие фрезы
 Каталог Iscar дисковые фрезы и фрезерные пластины 2022
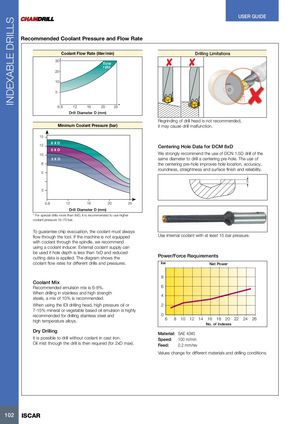
Recommended Coolant Pressure and Flow Rate
Coolant Flow Rate (liter/min) Drilling Limitations 30 flow rate 20 10 5
| 25 20 16 12 6.8 | |
| Drill Diameter D (mm) | |
| Regrinding of drill head is not recommended, | |
| Minimum Coolant Pressure (bar) it may cause drill malfunction. | |
| 15 | |
| 8 X D | |
| 12 | Centering Hole Data for DCM 8xD |
| 5 X D | |
| We strongly recommend the use of DCN 1.5D drill of the | |
| 10 | |
| 3 X D same diameter to drill a centering pre-hole. The use of | |
| 8 | the centering pre-hole improves hole location, accuracy, |
| roundness, straightness and surface finish and reliability. | |
| 5 | |
| 5 | |
| 3 |
6.8 12 16 20 25
Drill Diameter D (mm) * For special drills more than 8xD, it is recommended to use higher coolant pressure 15–70 bar. To guarantee chip evacuation, the coolant must always
flow through the tool. If the machine is not equipped Use internal coolant with at least 15 bar pressure. with coolant through the spindle, we recommend using a coolant inducer. External coolant supply can be used if hole depth is less than 1xD and reduced
Power/Force Requirements
cutting data is applied. The diagram shows the
coolant flow rates for different drills and pressures. kw Net Power
8 Coolant Mix Recommended emulsion mix is 6-8%. 6 When drilling in stainless and high strength
4 steels, a mix of 10% is recommended. When using the IDI drilling head, high pressure oil or 2 7-15% mineral or vegetable based oil emulsion is highly recommended for drilling stainless steel and 0
| high temperature alloys. | 6 | 8 10 12 14 16 18 20 22 24 26 | |||
| No. of Indexes | |||||
| Dry Drilling | |||||
| Material: | SAE 4340 |
It is possible to drill without coolant in cast iron. Speed: 100 m/min
Oil mist through the drill is then required (for 2xD max). 0.2 mm/rev Feed: Values change for different materials and drilling conditions.