Каталог Iscar сверла ружейные и для глубокого сверления 2022 - страница 125
Навигация
 Каталог Iscar новые продукты 2018
 Каталог Iscar полирующие фрезы
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar токарные державки ISO 2022
 Фрезерные инструменты Iscar 2026
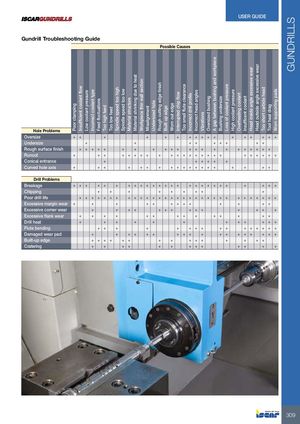
Gundrill Troubleshooting Guide
| Hole Problems | Poor clamping Insufficient coolant flow | Low coolant pressure | Incorrect coolant type | F fli | eed uctuatons | Too high feed | Too low feed | Spindle speed too high | Spindle speed too low | Material structure | Material shrinking due to heat | Workpiece thin wall section | Misalignment | Undersized hole | Po Rough cutting edge finish | ssi Built up edge | ble Ca Worn out edge Interrupted chip flow | us Too small flute clearance | es Incorrect drill rofile | p Incorrect head angles | Vibrations | Oid bhi | versze usng | A gap between bushing and workpiece | Bushing undersize | Loss of coolant pressure | High coolant pressure | Overheating coolant | Insufficent coolant | Head inside angle excessive wear | Hdtidli | ea ouse ange excessve wear | Too short carbide head | Tool heal dra | g Worn supporting pads |
| Oversize | + + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | |||||||||||||||||||
| Undersize | + | + | + | + | + | + | + | + | + | ||||||||||||||||||||||||||
| Rough surface finish | + | + | + | + | + | + | + | + | + | + + | + | + | + | + | + | + | + | + | + | + | + | ||||||||||||||
| Runout | + | + | + | + | + | + | + | + | + | + + | + | + | + | + | + | + | + | + | + | + | + | + | + | ||||||||||||
| Conical entrance | + | + | + | + | + | + | |||||||||||||||||||||||||||||
| Curved hole axis | + | + | + | + | + | + | + | + + | + | + | + | + | + | + | + | + | + | + | |||||||||||||||||
| Drill Problems Breakage | + + | + | + | + | + | + | + | + | + | + | + | + | + + | + | + | + | + | + | + | + | + | + | + | + | |||||||||||
| Chipping | + | + | + | + | + | + | + | + | + | ||||||||||||||||||||||||||
| Poor drill life | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | |||||
| Excessive margin wear | + | + | + | + | + | + + | + | + | + | + | + | + | |||||||||||||||||||||||
| Excessive corner wear | + | + | + | + | + | + | + | + | + | + | + | + | + | + | |||||||||||||||||||||
| Excessive flank wear | + | + | + | + | + | + | + | + | + | + | + | + | + | + | |||||||||||||||||||||
| Drill heat | + | + | + | + | + | + | + | + | + | + | + | + | |||||||||||||||||||||||
| Flute bending | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | |||||||||||||||||||
| Damaged wear pad | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | |||||||||||||||||
| Built-up edge | + | + | + | + | + | + | + | + | + | + | + | + | + | + | + | ||||||||||||||||||||
| Cratering | + | + | + | + | + | + | + | + | + | + | + | + | + |