Каталог Iscar сверла ружейные и для глубокого сверления 2022 - страница 120
Навигация
 Каталог Iscar новые продукты 2018
 Каталог Iscar полирующие фрезы
 Каталог Iscar инструмент для фрезерования
 Каталог Iscar инструмент для нарезания резьбы
 Каталог Iscar токарные державки ISO 2022
 Фрезерные инструменты Iscar 2026
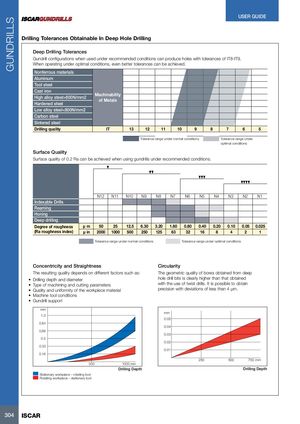
Drilling Tolerances Obtainable In Deep Hole Drilling
Deep Drilling Tolerances
Gundrill configurations when used under recommended conditions can produce holes with tolerances of IT8-IT9. When operating under optimal conditions, even better tolerances can be achieved. Nonferrous materials Aluminum Tool steel Cast iron Machinability High alloy steel>800N/mm2 of Metals Hardened steel Low alloy steel<800N/mm2 Carbon steel Sintered steel
Drilling quality IT 13 12 11 10 9 8 7 6 5
Tolerance range under normal conditions Tolerance range under optimal conditions Surface Quality Surface quality of 0.2 Ra can be achieved when using gundrills under recommended conditions.
| N12 | N11 | N10 | N9 | N8 | N7 | N6 | N5 | N4 | N3 | N2 | N1 | ||
| Indexable Drills | |||||||||||||
| Reaming | |||||||||||||
| Honing | |||||||||||||
| Deep drilling | |||||||||||||
| Degree of roughness | μ m | 50 | 25 | 12.5 | 6.30 | 3.20 | 1.60 | 0.80 | 0.40 | 0.20 | 0.10 | 0.05 | 0.025 |
| (Ra roughness index) | μ in | 2000 | 1000 | 500 | 250 | 125 | 63 | 32 | 16 | 8 | 4 | 2 | 1 |
Tolerance range under normal conditions Tolerance range under optimal conditions
Concentricity and Straightness
The resulting quality depends on different factors such as:
- Drilling depth and diameter
- Type of machining and cutting parameters
- Quality and uniformity of the workpiece material
- Machine tool conditions
- Gundrill support mm 1.0 0.84 0,66 0.5 0.33 0.16
500 1000 mm Drilling Depth Stationary workpiece – rotating tool Rotating workpiece – stationary tool
Circularity
The geometric quality of bores obtained from deep hole drill bits is clearly higher than that obtained with the use of twist drills. It is possible to obtain precision with deviations of less than 4 µm.
mm 0.05 0.04 0.03 0.02 0.01
250 500 750 mm
Drilling Depth