Каталог Iscar отрезка 2022 - страница 74
Навигация
 Токарные инструменты Iscar (часть 1) 2026
 Каталог Iscar монолитные фрезы 2022
 Инструменты для обработки отверстий Iscar 2026
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar расточные системы
 Каталог Iscar токарный инструмент 2017
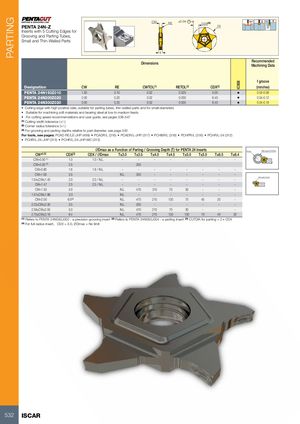
| PENTA 24N-Z Inserts with 5 Cutting Edges for Grooving and Parting Tubes, Small and Thin-Walled Parts | CW R 4 | E 24 CDX(3) ±0.04 | ||||
| Dimensions | Recommended Machining Data | |||||
| Designation | CW | RE | CWTOL(1) | RETOL(2) CDX(3) | IC908 | f groove (mm/rev) |
| PENTA 24N150Z010 | 1.50 | 0.10 | 0.02 | 0.020 5.00 | • | 0.05-0.08 |
| PENTA 24N200Z020 | 2.00 | 0.20 | 0.02 | 0.030 6.40 | • | 0.04-0.12 |
| PENTA 24N300Z020 | 3.00 | 0.20 | 0.02 | 0.000 6.40 | • | 0.04-0.16 |
- Cutting edge with high positive rake, suitable for parting tubes, thin walled parts and for small diameters
- Suitable for machining soft materials and bearing steel at low to medium feeds
- For cutting speed recommendations and user guide, see pages 538-547
(1) Cutting width tolerance (+/-) (2) Corner radius tolerance (+/-) (3) For grooving and parting depths relative to part diameter, see page 532
For tools, see pages: PCAD RE/LE-JHP (499) PCADR/L (316) PCADR/L-JHP (317) PCHBR/L (318) PCHPR/L (316) PCHR/L-24 (312)
- PCHR/L-24-JHP (313)
- PCHR/L-24-JHP-MC (313)
| ØDmax as a | Function o | f Parting/ | GroovingD | epth(T)fo | r PENTA 2 | 4 Inserts | ØDmax(CUTDIA) Tmax | ||||
| CW±0.02 | CDX(3) | CDX /ØDmax | T≤3.0 | T≤3.5 | T≤4.0 | T≤4.5 | T≤5.0 | T≤5.5 | T≤6.5 | T≤6.4 | |
| CW=0.50(1) | 1.0 | 1.0 / N.L. | - | - | - | - | - | - | - | - | |
| CW=0.50(2) | 2.5 | 250 | |||||||||
| CW=0.80 | 1.6 | 1.6 / N.L. | - | - | - | - | - | - | - | - | |
| CW=1.00 | 3.5 | N.L. | 250 | - | - | - | - | - | - | ||
| 1.04≤CW≤1.40 | 2.0 | 2.0 / N.L. | - | - | - | - | - | - | - | - | ØDmax(CUTDIA) |
| CW=1.47 | 2.5 | 2.5 / N.L. | - | - | - | - | - | - | - | - | |
| CW=1.50 | 5.0 | N.L. | 470 | 210 | 70 | 30 | - | - | - | ||
| 1.57≤CW≤1.96 | 3.0 | N.L. | - | - | - | - | - | - | - | ||
| CW=2.00 | 6.0(4) | N.L. | 470 | 210 | 130 | 75 | 45 | 20 | - | ||
| 2.22≤CW≤2.30 | 3.5 | N.L. | 250 | - | - | - | - | - | - | ||
| 2.39≤CW≤2.50 | 5.0 | N.L. | 470 | 210 | 70 | 30 | - | - | - | ||
| 2.70≤CW≤3.18 | 6.4 | N.L. | 470 | 210 | 135 | 100 | 70 | 40 | 20 |
(1) Refers to PENTA 24N050J000 - a precision grooving insert (2) Refers to PENTA 24N050J004 - a parting insert (3) CUTDIA for parting = 2 x CDX (4) For full radius insert, CDX = 3.0, ØDmax = No limit