Каталог Iscar обработка канавок 2022 - страница 96
Навигация
 Каталог Iscar монолитные концевые фрезы и система multi-master
 Фрезерные инструменты Iscar 2026
 Каталог Iscar сверла ружейные и для глубокого сверления 2022
 Каталог Iscar токарные державки ISO 2022
 Каталог Iscar инструмент для обработки алюминиевых колёс
GROOVE-TURN
±0.025
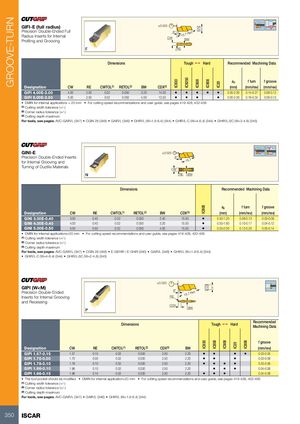
GIFI-E (full radius) 5
Precision Double-Ended Full 8° Ref.
Radius Inserts for Internal 15.7
CW BW
Profiling and Grooving
RE
Dimensions Tough 1 Hard Recommended Machining Data
IC8250
ap f turn f groove
IC830
IC808
IC908
IC20
Designation CW RE CWTOL(1) RETOL(2) BW CDX(3) (mm) (mm/rev) (mm/rev)
GIFI 4.00E-2.00 4.00 2.00 0.02 0.050 3.20 14.00 • • • • • 0.00-2.00 0.14-0.27 0.06-0.12
GIFI 5.00E-2.50 5.00 2.50 0.02 0.050 4.00 13.50 • • • • 0.00-2.50 0.18-0.34 0.08-0.15
• DMIN for internal applications = 20 mm • For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
(3) Cutting depth maximum
For tools, see pages: AVC-GAIR/L (347) • CGIN 26 (348) • GAIR/L (346) • GHIR/L (W=1.9-6.4) (344) • GHIR/L-C (W=4-6.4) (344) • GHIR/L-SC (W=2-4.8) (345)
GINI-E ±0.025
Precision Double-Ended Inserts 8°
for Internal Grooving and 15.7
Turning of Ductile Materials
CW
RE BW
Dimensions Recommended Machining Data
ap f turn f groove
IC808
Designation CW RE CWTOL(1) RETOL(2) BW CDX(3) (mm) (mm/rev) (mm/rev)
GINI 3.00E-0.40 3.00 0.40 0.02 0.050 2.40 15.50 • 0.50-1.20 0.08-0.13 0.03-0.09
GINI 4.00E-0.40 4.00 0.40 0.02 0.050 3.20 15.50 • 0.50-1.60 0.10-0.17 0.04-0.12
GINI 5.00E-0.50 5.00 0.50 0.02 0.050 4.00 15.50 • 0.50-2.00 0.12-0.20 0.05-0.14
• DMIN for internal applications=20 mm • For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
(3) Cutting depth maximum
For tools, see pages: AVC-GAIR/L (347) • CGIN 26 (348) • E-GEHIR / E-GHIR (340) • GAIR/L (346) • GHIR/L (W=1.9-6.4) (344)
• GHIR/L-C (W=4-6.4) (344) • GHIR/L-SC (W=2-4.8) (345)
±0.025
GIPI (W<M) 8°
5
Precision Double-Ended Ref.
RE 15.7
Inserts for Internal Grooving
and Recessing
CDX
BW
Recommended
Dimensions Tough 1 Hard
Machining Data
f groove
IC830
IC808
IC908
IC806
IC20
Designation CW RE CWTOL(1) RETOL(2) CDX(3) BW (mm/rev)
GIPI 1.57-0.15 1.57 0.15 0.02 0.030 2.50 2.20 • • • • 0.03-0.05
GIPI 1.70-0.00 1.70 0.00 0.02 0.030 2.50 2.20 • • • 0.03-0.06
GIPI 1.78-0.10 1.78 0.10 0.02 0.030 2.50 2.20 • • • • 0.03-0.06
GIPI 1.96-0.10 1.96 0.10 0.02 0.030 2.50 2.20 • • • 0.04-0.06
GIPI 1.96-0.15 1.96 0.15 0.02 0.030 2.50 2.20 • • • 0.04-0.06
• The tool pocket should be modified • DMIN for internal application=20 mm • For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
(3) Cutting depth maximum
For tools, see pages: AVC-GAIR/L (347) • GAIR/L (346) • GHIR/L (W=1.9-6.4) (344)
350 ISCAR
±0.025
GIFI-E (full radius) 5
Precision Double-Ended Full 8° Ref.
Radius Inserts for Internal 15.7
CW BW
Profiling and Grooving
RE
Dimensions Tough 1 Hard Recommended Machining Data
IC8250
ap f turn f groove
IC830
IC808
IC908
IC20
Designation CW RE CWTOL(1) RETOL(2) BW CDX(3) (mm) (mm/rev) (mm/rev)
GIFI 4.00E-2.00 4.00 2.00 0.02 0.050 3.20 14.00 • • • • • 0.00-2.00 0.14-0.27 0.06-0.12
GIFI 5.00E-2.50 5.00 2.50 0.02 0.050 4.00 13.50 • • • • 0.00-2.50 0.18-0.34 0.08-0.15
• DMIN for internal applications = 20 mm • For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
(3) Cutting depth maximum
For tools, see pages: AVC-GAIR/L (347) • CGIN 26 (348) • GAIR/L (346) • GHIR/L (W=1.9-6.4) (344) • GHIR/L-C (W=4-6.4) (344) • GHIR/L-SC (W=2-4.8) (345)
GINI-E ±0.025
Precision Double-Ended Inserts 8°
for Internal Grooving and 15.7
Turning of Ductile Materials
CW
RE BW
Dimensions Recommended Machining Data
ap f turn f groove
IC808
Designation CW RE CWTOL(1) RETOL(2) BW CDX(3) (mm) (mm/rev) (mm/rev)
GINI 3.00E-0.40 3.00 0.40 0.02 0.050 2.40 15.50 • 0.50-1.20 0.08-0.13 0.03-0.09
GINI 4.00E-0.40 4.00 0.40 0.02 0.050 3.20 15.50 • 0.50-1.60 0.10-0.17 0.04-0.12
GINI 5.00E-0.50 5.00 0.50 0.02 0.050 4.00 15.50 • 0.50-2.00 0.12-0.20 0.05-0.14
• DMIN for internal applications=20 mm • For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
(3) Cutting depth maximum
For tools, see pages: AVC-GAIR/L (347) • CGIN 26 (348) • E-GEHIR / E-GHIR (340) • GAIR/L (346) • GHIR/L (W=1.9-6.4) (344)
• GHIR/L-C (W=4-6.4) (344) • GHIR/L-SC (W=2-4.8) (345)
±0.025
GIPI (W<M) 8°
5
Precision Double-Ended Ref.
RE 15.7
Inserts for Internal Grooving
and Recessing
CDX
BW
Recommended
Dimensions Tough 1 Hard
Machining Data
f groove
IC830
IC808
IC908
IC806
IC20
Designation CW RE CWTOL(1) RETOL(2) CDX(3) BW (mm/rev)
GIPI 1.57-0.15 1.57 0.15 0.02 0.030 2.50 2.20 • • • • 0.03-0.05
GIPI 1.70-0.00 1.70 0.00 0.02 0.030 2.50 2.20 • • • 0.03-0.06
GIPI 1.78-0.10 1.78 0.10 0.02 0.030 2.50 2.20 • • • • 0.03-0.06
GIPI 1.96-0.10 1.96 0.10 0.02 0.030 2.50 2.20 • • • 0.04-0.06
GIPI 1.96-0.15 1.96 0.15 0.02 0.030 2.50 2.20 • • • 0.04-0.06
• The tool pocket should be modified • DMIN for internal application=20 mm • For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-)
(2) Corner radius tolerance (+/-)
(3) Cutting depth maximum
For tools, see pages: AVC-GAIR/L (347) • GAIR/L (346) • GHIR/L (W=1.9-6.4) (344)
350 ISCAR