Каталог Iscar обработка канавок 2022 - страница 89
Навигация
 Каталог Iscar монолитные концевые фрезы и система multi-master
 Фрезерные инструменты Iscar 2026
 Каталог Iscar сверла ружейные и для глубокого сверления 2022
 Каталог Iscar токарные державки ISO 2022
 Каталог Iscar инструмент для обработки алюминиевых колёс
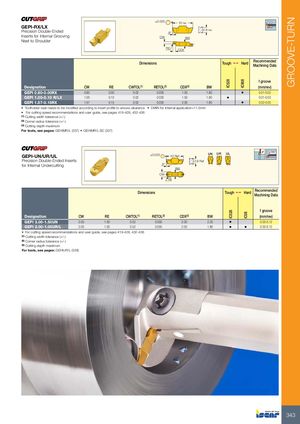
| GEPI-RX/LX Precision Double-Ended Inserts for Internal Grooving Next to Shoulder | RE CW 8° ±0.025 | 10Ref. CDX BW | 2.9Ref. | |||||
| Dime | nsions | Tough1 | Hard | Recommended Machining Data | ||||
| Designation | CW RE | CWTOL(1) | RETOL(2) | CDX(3) | BW | IC528 | IC908 | f groove (mm/rev) |
| GEPI 0.80-0.00RX | 0.80 0.00 | 0.02 | 0.030 | 1.50 | 1.80 | • | 0.01-0.02 | |
| GEPI 1.00-0.10 R/LX | 1.00 0.10 | 0.02 | 0.030 | 1.50 | 1.80 | • | 0.01-0.03 | |
| GEPI 1.57-0.15RX | 1.57 0.15 | 0.02 | 0.030 | 2.00 | 1.80 | • | 0.02-0.05 |
- Toolholder seat needs to be modified according to insert profile to ensure clearance
- DMIN for internal application=11.5mm
- For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-) (2) Corner radius tolerance (+/-) (3) Cutting depth maximum
For tools, see pages: GEHIMR/L (337) GEHIMR/L-SC (337)
| GEPI-UN/UR/UL Precision Double-Ended Inserts for Internal Undercutting | 1 ±0.025 CW 8° RE | 0 Ref. BW | 2.9 Ref. | UN UR | UL | ||||
| Dim | ensions | Tough1 | Hard | Recommended Machining Data | |||||
| Designation CW | RE | CWTOL(1) | RETOL(2) | CDX(3 | ) | BW | IC528 | IC08 | f groove (mm/rev) |
| GEPI 3.00-1.50UN 3.00 | 1.50 | 0.02 | 0.050 | 2.00 | 2.20 | • | 0.03-0.12 | ||
| GEPI 2.00-1.00UR/L 2.00 | 1.00 | 0.02 | 0.050 | 2.00 | 1.80 | • | • | 0.03-0.12 |
- For cutting speed recommendations and user guide, see pages 419-428, 432-436
(1) Cutting width tolerance (+/-) (2) Corner radius tolerance (+/-) (3) Cutting depth maximum
For tools, see pages: GEHIUR/L (339)