Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 210
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
Rd°
RXCW 07/ 08 RXCW 10
RXCW S S
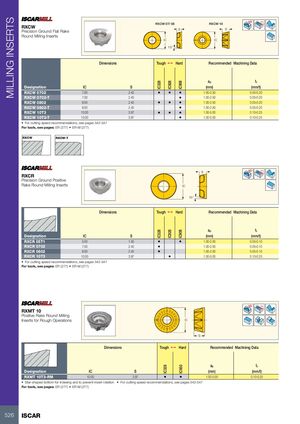
Precision Ground Flat Rake
Round Milling Inserts
IC IC
15°
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC928
IC908
Designation IC S (mm) (mm/t)
RXCW 0702 7.00 2.40 • • • 1.00-2.50 0.05-0.20
RXCW 0702-T 7.00 2.40 • 1.00-2.50 0.05-0.20
RXCW 0802 8.00 2.40 • • • 1.00-2.50 0.05-0.20
RXCW 0802-T 8.00 2.40 • 1.00-2.50 0.05-0.20
RXCW 10T3 10.00 3.97 • • • 1.00-5.00 0.10-0.25
RXCW 10T3-T 10.00 3.97 • 1.00-5.00 0.10-0.25
• For cutting speed recommendations, see pages 542-547
For tools, see pages: ER (277) • ER-M (277)
RXCW RXCW-T
Rd°
S
RXCR
Precision Ground Positive
Rake Round Milling Inserts IC
15°
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC928
IC908
Designation IC S (mm) (mm/t)
RXCR 05T1 5.00 1.50 • • 1.00-2.00 0.05-0.10
RXCR 0702 7.00 2.40 • 1.00-2.00 0.05-0.10
RXCR 0802 8.00 2.40 • 1.00-2.00 0.05-0.10
RXCR 10T3 10.00 3.97 • 1.00-5.00 0.10-0.25
• For cutting speed recommendations, see pages 542-547
For tools, see pages: ER (277) • ER-M (277)
Rd°
RXMT 10
Positive Rake Round Milling
Inserts for Rough Operations IC
S
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC950
Designation IC S (mm) (mm/t)
RXMT 10T3-RM 10.00 3.97 • • 1.00-5.00 0.10-0.25
• Star-shaped bottom for indexing and to prevent insert rotation • For cutting speed recommendations, see pages 542-547
For tools, see pages: ER (277) • ER-M (277)
526 ISCAR
Rd°
RXCW 07/ 08 RXCW 10
RXCW S S
Precision Ground Flat Rake
Round Milling Inserts
IC IC
15°
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC928
IC908
Designation IC S (mm) (mm/t)
RXCW 0702 7.00 2.40 • • • 1.00-2.50 0.05-0.20
RXCW 0702-T 7.00 2.40 • 1.00-2.50 0.05-0.20
RXCW 0802 8.00 2.40 • • • 1.00-2.50 0.05-0.20
RXCW 0802-T 8.00 2.40 • 1.00-2.50 0.05-0.20
RXCW 10T3 10.00 3.97 • • • 1.00-5.00 0.10-0.25
RXCW 10T3-T 10.00 3.97 • 1.00-5.00 0.10-0.25
• For cutting speed recommendations, see pages 542-547
For tools, see pages: ER (277) • ER-M (277)
RXCW RXCW-T
Rd°
S
RXCR
Precision Ground Positive
Rake Round Milling Inserts IC
15°
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC928
IC908
Designation IC S (mm) (mm/t)
RXCR 05T1 5.00 1.50 • • 1.00-2.00 0.05-0.10
RXCR 0702 7.00 2.40 • 1.00-2.00 0.05-0.10
RXCR 0802 8.00 2.40 • 1.00-2.00 0.05-0.10
RXCR 10T3 10.00 3.97 • 1.00-5.00 0.10-0.25
• For cutting speed recommendations, see pages 542-547
For tools, see pages: ER (277) • ER-M (277)
Rd°
RXMT 10
Positive Rake Round Milling
Inserts for Rough Operations IC
S
Dimensions Tough 1 Hard Recommended Machining Data
ap fz
IC328
IC950
Designation IC S (mm) (mm/t)
RXMT 10T3-RM 10.00 3.97 • • 1.00-5.00 0.10-0.25
• Star-shaped bottom for indexing and to prevent insert rotation • For cutting speed recommendations, see pages 542-547
For tools, see pages: ER (277) • ER-M (277)
526 ISCAR