Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 192
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
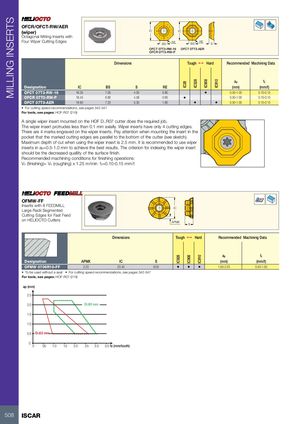
OFCR/OFCT-RW/AER
| (wiper) | IC | IC |
| Octagonal Milling Inserts with |
Four Wiper Cutting Edges RE RE
| BS | BS | S | ||
| OFCT 07T3-RW-16 | OFCT 07T3-AER | |||
| OFCR 07T3-RW-P |
Dimensions Tough 1 Hard Recommended Machining Data
a f
p z
| Designation | IC | BS | S | RE | (mm) | (mm/t) | ||||
| OFCT 07T3-RW-16 | 18.35 | 7.00 | 4.50 | 0.80 | • | 0.50-1.00 | 0.10-0.15 | |||
| OFCR 07T3-RW-P | 18.45 | 6.80 | 4.58 | 0.60 | • | 0.50-1.00 | 0.10-0.15 | |||
| OFCT 07T3-AER | 18.90 | 7.20 | 5.30 | 1.60 | • | • | 0.50-1.00 | 0.10-0.15 |
- For cutting speed recommendations, see pages 542-547
For tools, see pages: HOF-R07 (219) A single wiper insert mounted on the HOF D..R07 cutter does the required job. The wiper insert protrudes less than 0.1 mm axially. Wiper inserts have only 4 cutting edges.
There are 4 marks engraved on the wiper inserts. Pay attention when mounting the insert in the
pocket that the marked cutting edges are parallel to the bottom of the cutter (see sketch).
Maximum depth of cut when using the wiper insert is 2.5 mm. It is recommended to use wiper
inserts in ap=0.5-1.0 mm to achieve the best results. The criterion for indexing the wiper insert
should be the decreased quallity of the surface finish. Recommended machining conditions for finishing operations:
Vc (finishing)= V c (roughing) x 1.25 m/min fz=0.10-0.15 mm/t
OFMW-FF
Inserts with 8 FEEDMILL
Large Radii Segmented
Cutting Edges for Fast Feed
on HELIOCTO Cutters
6 7 8
Dimensions
4 IC 3 2
APMX S
Tough 1 Hard Recommended Machining Data
ap fz
| Designation | APMX | IC | S | (mm) | (mm/t) | |||
| OFMW 0706R10-FF | 2.20 | 20.40 | 8.00 | • | • | • | 1.00-2.20 | 0.40-1.50 |
- To be used without a seat
- For cutting speed recommendations, see pages 542-547
For tools, see pages: HOF-R07 (219) ap (mm) 2.5 2.0 D≥80 mm 1.5 1.0 0.5 D≤63 mm 0
0 0.5 1.0 1.5 2.0 2.5 3.0 3.5 fz (mm/tooth)