Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 152
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
MILLING INSERTS
60°
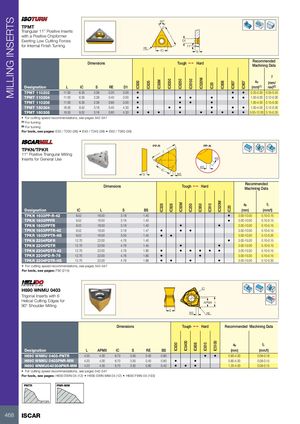
TPMT
Triangular 11° Positive Inserts
with a Positive Chipformer L
Exerting Low Cutting Forces D1
for Internal Finish Turning RE
11°
IC S
Recommended
Dimensions Tough 1 Hard
Machining Data
f
IC520M
ap
IC8350
IC8250
IC8150
IC50M
(mm/
IC830
IC635
IC806
IC807
IC907
IC20
Designation L IC S RE D1 (mm)(1) rev)(2)
TPMT 110202 11.00 6.35 2.38 0.20 3.00 • • • 0.20-2.00 0.05-0.25
TPMT 110204 11.00 6.35 2.38 0.40 3.00 • • • • • • 1.00-3.00 0.12-0.30
TPMT 110208 11.00 6.35 2.38 0.80 3.00 • • • • 1.00-4.00 0.15-0.30
TPMT 160304 16.50 9.52 3.18 0.40 4.30 • • • • • • 1.00-4.00 0.12-0.30
TPMT 160308 16.50 9.52 3.18 0.80 4.30 • • • • • • • • • 5.00-12.00 0.15-0.35
• For cutting speed recommendations, see pages 542-547
(1) For turning
(2) For turning
For tools, see pages: E30 / T230 (36) • E45 / T245 (38) • E60 / T260 (39)
PP-R PP-N
TPKN/TPKR L
11° Positive Triangular Milling
Inserts for General Use BS
BS
IC
S BS
Recommended
Dimensions Tough 1 Hard
Machining Data
IC520M
ap fz
IC50M
IC328
IC928
IC250
IC950
IC910
IC20
Designation IC L S BS (mm) (mm/t)
TPKN 1603PP-R-42 9.52 16.50 3.18 1.40 • 3.00-10.00 0.10-0.15
TPKN 1603PPFR 9.52 16.50 3.18 1.40 • 3.00-10.00 0.10-0.15
TPKN 1603PPTR 9.52 16.50 3.18 1.40 • • 3.00-10.00 0.10-0.15
TPKN 1603PPTR-42 9.52 16.50 3.18 1.47 • • • 3.00-10.00 0.10-0.15
TPKR 1603PPTR-HS 9.52 16.50 3.50 1.45 • • 3.00-10.00 0.12-0.20
TPKN 2204PDFR 12.70 22.00 4.76 1.40 • 3.00-15.00 0.10-0.15
TPKN 2204PDTR 12.70 22.00 4.76 1.45 • • 3.00-15.00 0.10-0.15
TPKN 2204PDTR-42 12.70 22.00 4.76 1.80 • • • • • • 3.00-15.00 0.10-0.15
TPKR 2204PD-R-76 12.70 22.00 4.76 1.80 • • 3.00-15.00 0.10-0.15
TPKR 2204PDTR-HS 12.70 22.00 4.76 1.88 • • • • 3.00-15.00 0.12-0.20
• For cutting speed recommendations, see pages 542-547
For tools, see pages: F90 (214)
IC
H690 WNMU 0403
Trigonal Inserts with 6 Rd°
Helical Cutting Edges for APMX L
90° Shoulder Milling
S
BS RE
Dimensions Tough 1 Hard Recommended Machining Data
IC5400
IC5100
ap fz
IC830
IC808
IC810
Designation L APMX IC S RE BS (mm) (mm/t)
H690 WNMU 0403-PNTR 4.20 4.00 6.70 3.50 0.40 0.80 • • 0.80-4.00 0.08-0.18
H690 WNMU 0403PNR-MM 4.20 4.00 6.70 3.50 0.40 0.80 • • 0.80-4.00 0.08-0.15
H690 WNMU040308PNR-MM 4.20 4.00 6.70 3.50 0.80 0.40 • • • 1.20-4.00 0.08-0.15
• For cutting speed recommendations, see pages 542-547
For tools, see pages: H690 EWN-04 (12) • H690 EWN-MM-04 (12) • H690 FWN-04 (193)
PNTR PNR-MM
468 ISCAR