Каталог Iscar дисковые фрезы и фрезерные пластины 2022 - страница 146
Навигация
 Каталог Iscar крепление инструмента
 Каталог Iscar инструмент для обработки отверстий
 Каталог Iscar резьбонарезные фрезы
 Каталог Iscar инструмента для сверления
 Каталог Iscar решения для глубокого сверления
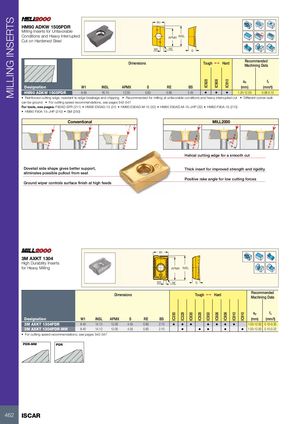
HM90 ADKW 1505PDR Milling Inserts for Unfavorable Conditions and Heavy Interrupted Cut on Hardened Steel
Dimensions
Rd° lNSL APMX
BS RE S Recommended
Tough 1 Hard Machining Data
a f p z
| Designation | W1 | INSL | APMX | S | RE | BS | (mm) | (mm/t) | |||
| HM90 ADKW 1505PDR | 9.59 | 16.15 | 12.00 | 5.83 | 0.80 | 2.45 | • | • | • | 1.20-12.00 | 0.08-0.15 |
- Reinforced cutting edge, resistant to edge breakage and chipping
- Recommended for milling at unfavorable conditions and heavy interrupted cut
- Different corner radii
can be ground For cutting speed recommendations, see pages 542-547
For tools, see pages: F90AD-SFR (211) HM90 E90AD-15 (31) HM90 E90AD-M-15 (32) HM90 E90AD-M-15-JHP (32) HM90 F90A-15 (210)
- HM90 F90A-15-JHP (210)
- SM (250)
Conventional MILL2000
Dovetail side shape gives better support, eliminates possible pullout from seat Ground wiper controls surface finish at high feeds
Helical cutting edge for a smooth cut Thick insert for improved strength and rigidity Positive rake angle for low cutting forces
3M AXKT 1304 High Durability Inserts for Heavy Milling
W1
APMX INSL
| BS | RE | S | |
| Recommended |
Dimensions Tough 1 Hard Machining Data
a f p z
| Designation | W1 | INSL | APMX | S | RE | BS | (mm) | (mm/t) | ||||||
| 3M AXKT 1304PDR | 8.40 | 14.12 | 12.00 | 4.55 | 0.60 | 2.10 | • • • | • • • • | 1.00-12.00 0.15-0.35 | |||||
| 3M AXKT 1304PDR-MM | 8.40 | 14.12 | 12.00 | 4.55 | 0.60 | 2.10 | • | • • | • | • | 1.00-12.00 0.10-0.22 |
- For cutting speed recommendations, see pages 542-547 PDR-MM PDR