Каталог Iscar инструмент для внутренней обработки - страница 97
Навигация
 Каталог Iscar инструментальные блоки
 Фрезерные инструменты Iscar 2026
 Каталог Iscar обработка канавок 2022
 Каталог Iscar инструмент для нарезания резьбы
 Токарные инструменты Iscar (часть 2) 2026
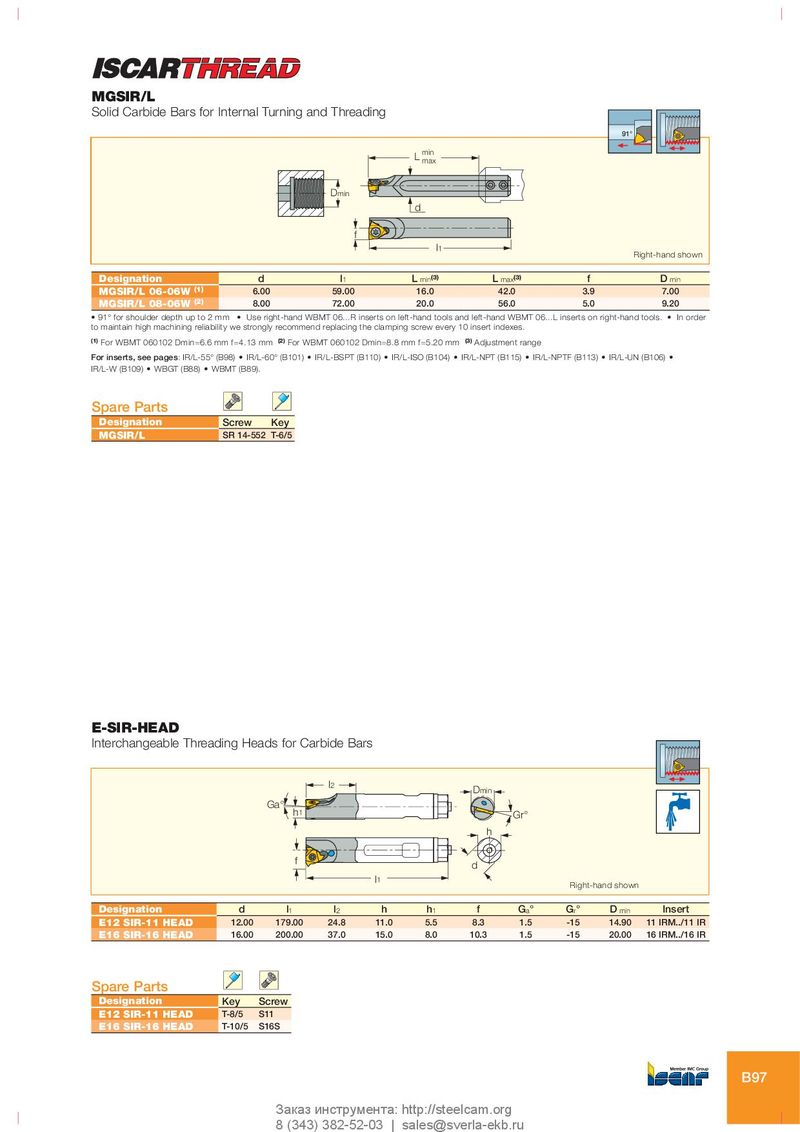
MGSIR/L
Solid Carbide Bars for Internal Turning and Threading
91° L min max
Dmin d
f l1 Right-hand shown
| Designation | d | l1 | L min(3) | L max(3) | f | D min |
| MGSIR/L 06-06W (1) | 6.00 | 59.00 | 16.0 | 42.0 | 3.9 | 7.00 |
| MGSIR/L 08-06W (2) | 8.00 | 72.00 | 20.0 | 56.0 | 5.0 | 9.20 |
- 91° for shoulder depth up to 2 mm
- Use right-hand WBMT 06...R inserts on left-hand tools and left-hand WBMT 06...L inserts on right-hand tools.
- In order
to maintain high machining reliability we strongly recommend replacing the clamping screw every 10 insert indexes. (1) For WBMT 060102 Dmin=6.6 mm f=4.13 mm (2) For WBMT 060102 Dmin=8.8 mm f=5.20 mm (3) Adjustment range For inserts, see pages: IR/L-55° (B98) IR/L-60° (B101) IR/L-BSPT (B110) IR/L-ISO (B104) IR/L-NPT (B115) IR/L-NPTF (B113) IR/L-UN (B106) IR/L-W (B109) WBGT (B88) WBMT (B89).
Spare Parts
Designation Screw Key
MGSIR/L SR 14-552 T-6/5
E-SIR-HEAD
Interchangeable Threading Heads for Carbide Bars
l2 Dmin Ga° h1 Gr° h
f d l1 Right-hand shown
| Designation | d | l1 | l2 | h | h1 | f | Ga° | Gr° | D min | Insert | |
| E12 SIR-11 HEAD | 12.00 | 179.00 | 24.8 | 11.0 | 5.5 | 8.3 | 1.5 | -15 | 14.90 | 11 IRM../11 IR | |
| E16 SIR-16 HEAD | 16.00 | 200.00 | 37.0 | 15.0 | 8.0 | 10.3 | 1.5 | -15 | 20.00 | 16 IRM../16 IR |
Spare Parts
| Designation | Key | Screw |
| E12 SIR-11 HEAD | T-8/5 | S11 |
| E16 SIR-16 HEAD | T-10/5 | S16S |