Общий каталог Dijet 2018 - страница 62
Навигация
 Общий каталог Dijet 2012 на русском
Tooling by DIJET
Modular Head Series
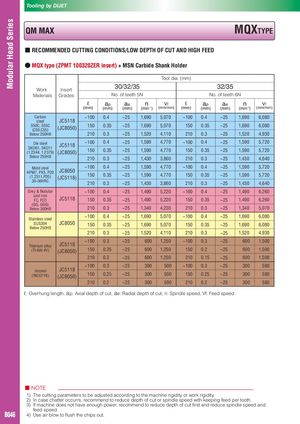
QM MAX MQXTYPE
■ RECOMMENDED CUTTING CONDITIONS/LOW DEPTH OF CUT AND HIGH FEED
● MQX type (ZPMT 100320ZER insert) + MSN Carbide Shank Holder
Tool dia. (mm)
Work Insert
30/32/35 32/35
Materials Grades No. of teeth 5N No. of teeth 6N
ℓ ap ae n Vf ℓ ap ae n Vf
(mm) (mm) (mm) (min-1) (mm/min) (mm) (mm) (mm) (min-1) (mm/min)
Carbon ~100 0.4 ~25 1,690 5,070 ~100 0.4 ~25 1,690 6,080
steel JC5118
S50C, S55C
(JC8050) 150 0.35 ~25 1,690 5,070 150 0.35 ~25 1,690 6,080
(C50,C55)
Below 250HB 210 0.3 ~25 1,520 4,110 210 0.3 ~25 1,520 4,930
Die steel ~100 0.4 ~25 1,590 4,770 ~100 0.4 ~25 1,590 5,720
SKD61, SKD11
JC5118
(1.2344, 1.2379) (JC8050) 150 0.35 ~25 1,590 4,770 150 0.35 ~25 1,590 5,720
Below 255HB
210 0.3 ~25 1,430 3,860 210 0.3 ~25 1,430 4,640
Mold steel ~100 0.4 ~25 1,590 4,770 ~100 0.4 ~25 1,590 5,720
HPM7, PX5, P20 JC8050
(1.2311,P20) 150 0.35 ~25 1,590 4,770 150 0.35 ~25 1,590 5,720
(JC5118)
30-36HRC
210 0.3 ~25 1,430 3,860 210 0.3 ~25 1,430 4,640
Grey & Nodular ~100 0.4 ~25 1,490 5,220 ~100 0.4 ~25 1,490 6,260
cast iron
FC, FCD JC5118 150 0.35 ~25 1,490 5,220 150 0.35 ~25 1,490 6,260
(GG, GGG)
Below 300HB 210 0.3 ~25 1,340 4,230 210 0.3 ~25 1,340 5,070
Stainless steel
~100 0.4 ~25 1,690 5,070 ~100 0.4 ~25 1,690 6,080
SUS304 JC8050 150 0.35 ~25 1,690 5,070 150 0.35 ~25 1,690 6,080
Below 250HB
210 0.3 ~25 1,520 4,110 210 0.3 ~25 1,520 4,930
~100 0.3 ~25 600 1,250 ~100 0.3 ~25 600 1,500
Titanium alloy JC5118
(Ti-6Al-4V) (JC8050) 150 0.25 ~25 600 1,250 150 0.2 ~25 600 1,500
210 0.2 ~25 600 1,250 210 0.15 ~25 600 1,500
~100 0.3 ~25 300 500 ~100 0.3 ~25 300 580
Inconel JC5118
(INCO718) 150 0.25 ~25 300 500 150 0.25 ~25 300 580
(JC8050)
210 0.2 ~25 300 500 210 0.2 ~25 300 580
ℓ: Overhung length, ap: Axial depth of cut, ae: Radial depth of cut, n: Spindle speed, Vf: Feed speed
■ NOTE
1) The cutting parameters to be adjusted according to the machine rigidity or work rigidity.
2) In case chatter occurrs, recommend to reduce depth of cut or spindle speed with keeping feed per tooth.
3) If machine does not have enough power, recommend to reduce depth of cut first and reduce spindle speed and
feed speed.
B046 4) Use air blow to flush the chips out.