Общий каталог Dijet 2018 - страница 56
Навигация
 Общий каталог Dijet 2012 на русском
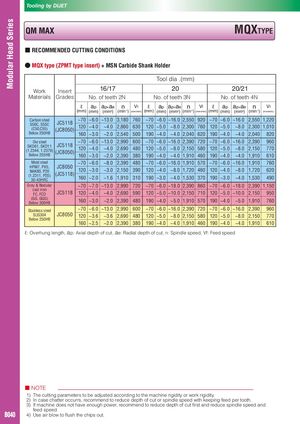
■ RECOMMENDED CUTTING CONDITIONS
- MQX type (ZPMT type insert) + MSN Carbide Shank Holder
| Tool | dia . | (mm) | ||||||||||||||
| Work | Insert | 16/17 | 20 | 20/2 | 1 | |||||||||||
| Materials | Grades | No. | of teet | h2N | No. o | f teeth | 3N | No. | of teet | h4N | ||||||
| ℓ (mm) | ap (mm) | ap×ae (mm2) | n (min-1) | Vf (mm/min) | ℓ (mm) | ap (mm) | ap×ae (mm2) | n (min-1) | Vf (mm/min) | ℓ (mm) | ap (mm) | ap×ae (mm2) | n (min-1) | Vf (mm/min) | ||
| Carbon steel | JC5118 | ~70 | ~6.0 | ~13.0 | 3,180 | 760 | ~70 | ~6.0 | ~16.0 | 2,550 | 920 | ~70 | ~6.0 | ~16.0 | 2,550 | 1,220 |
| S50C, S55C (C50,C55) | (JC8050) | 120 | ~4.0 | ~4.0 | 2,860 | 630 | 120 | ~5.0 | ~8.0 | 2,300 | 760 | 120 | ~5.0 | ~8.0 | 2,300 | 1,010 |
| Below 250HB | 160 | ~3.0 | ~2.0 | 2,540 | 500 | 190 | ~4.0 | ~4.0 | 2,040 | 620 | 190 | ~4.0 | ~4.0 | 2,040 | 820 | |
| Die steel | ~70 | ~6.0 | ~13.0 | 2,990 | 600 | ~70 | ~6.0 | ~16.0 | 2,390 | 720 | ~70 | ~6.0 | ~16.0 | 2,390 | 960 | |
| SKD61, SKD11 (1.2344 1.2379) | JC5118 | 120 | ~4.0 | ~4.0 | 2,690 | 480 | 120 | ~5.0 | ~8.0 | 2,150 | 580 | 120 | ~5.0 | ~8.0 | 2,150 | 770 |
| , Below 255HB | (JC8050) | 160 | ~3.0 | ~2.0 | 2,390 | 380 | 190 | ~4.0 | ~4.0 | 1,910 | 460 | 190 | ~4.0 | ~4.0 | 1,910 | 610 |
| Mold steel | ~70 | ~6.0 | ~8.0 | 2,390 | 480 | ~70 | ~6.0 | ~16.0 | 1,910 | 570 | ~70 | ~6.0 | ~16.0 | 1,910 | 760 | |
| HPM7, PX5, NAK80, P20 | JC8050 | 120 | ~3.0 | ~3.0 | 2,150 | 390 | 120 | ~4.0 | ~8.0 | 1,720 | 460 | 120 | ~4.0 | ~8.0 | 1,720 | 620 |
| (1.2311, P20) 30-43HRC | (JC5118) | 160 | ~2.0 | ~1.6 | 1,910 | 310 | 190 | ~3.0 | ~4.0 | 1,530 | 370 | 190 | ~3.0 | ~4.0 | 1,530 | 490 |
| Grey & Nodular | ~70 | ~7.0 | ~13.0 | 2,990 | 720 | ~70 | ~6.0 | ~18.0 | 2,390 | 860 | ~70 | ~6.0 | ~18.0 | 2,390 | 1,150 | |
| cast iron FC, FCD | JC5118 | 120 | ~4.0 | ~4.0 | 2,690 | 590 | 120 | ~5.0 | ~10.0 | 2,150 | 710 | 120 | ~5.0 | ~10.0 | 2,150 | 950 |
| (GG, GGG) Below 300HB | 160 | ~3.0 | ~2.0 | 2,390 | 480 | 190 | ~4.0 | ~5.0 | 1,910 | 570 | 190 | ~4.0 | ~5.0 | 1,910 | 760 | |
| Stainless steel | ~70 | ~6.0 | ~13.0 | 2,990 | 600 | ~70 | ~6.0 | ~16.0 | 2,390 | 720 | ~70 | ~6.0 | ~16.0 | 2,390 | 960 | |
| SUS304 Bl 250HB | JC8050 | 120 | ~3.6 | ~3.6 | 2,690 | 480 | 120 | ~5.0 | ~8.0 | 2,150 | 580 | 120 | ~5.0 | ~8.0 | 2,150 | 770 |
| eow | 160 | ~2.5 | ~2.0 | 2,390 | 380 | 190 | ~4.0 | ~4.0 | 1,910 | 460 | 190 | ~4.0 | ~4.0 | 1,910 | 610 |