Общий каталог Dijet 2018 - страница 55
Навигация
 Общий каталог Dijet 2012 на русском
Tooling by DIJET
Modular Head Series
QM MAX MQXTYPE
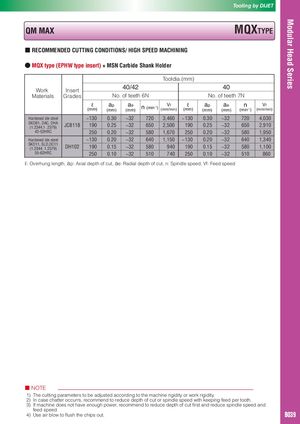
■ RECOMMENDED CUTTING CONDITIONS/ HIGH SPEED MACHINING
● MQX type (EPHW type insert) + MSN Carbide Shank Holder
Tooldia.(mm)
Work Insert
40/42 40
Materials Grades No. of teeth 6N No. of teeth 7N
ℓ ap ae Vf
n (min ) (mm/min)
-1
ℓ ap ae n Vf
(mm) (mm) (mm) (mm) (mm) (mm) (min-1) (mm/min)
Hardened die steel ~130 0.30 ~32 720 3,460 ~130 0.30 ~32 720 4,030
SKD61, DAC, DHA
(1.2344,1 .2379) JC8118 190 0.25 ~32 650 2,500 190 0.25 ~32 650 2,910
42-52HRC 250 0.20 ~32 580 1,670 250 0.20 ~32 580 1,950
Hardened die steel ~130 0.20 ~32 640 1,150 ~130 0.20 ~32 640 1,340
SKD11, SLD,DC11
(1.2344, 1.2379) DH102 190 0.15 ~32 580 940 190 0.15 ~32 580 1,100
55-62HRC 250 0.10 ~32 510 740 250 0.10 ~32 510 860
ℓ: Overhung length, ap: Axial depth of cut, ae: Radial depth of cut, n: Spindle speed, Vf: Feed speed
■ NOTE
1) The cutting parameters to be adjusted according to the machine rigidity or work rigidity.
2) In case chatter occurrs, recommend to reduce depth of cut or spindle speed with keeping feed per tooth.
3) If machine does not have enough power, recommend to reduce depth of cut first and reduce spindle speed and
feed speed.
4) Use air blow to flush the chips out. B039
Modular Head Series
QM MAX MQXTYPE
■ RECOMMENDED CUTTING CONDITIONS/ HIGH SPEED MACHINING
● MQX type (EPHW type insert) + MSN Carbide Shank Holder
Tooldia.(mm)
Work Insert
40/42 40
Materials Grades No. of teeth 6N No. of teeth 7N
ℓ ap ae Vf
n (min ) (mm/min)
-1
ℓ ap ae n Vf
(mm) (mm) (mm) (mm) (mm) (mm) (min-1) (mm/min)
Hardened die steel ~130 0.30 ~32 720 3,460 ~130 0.30 ~32 720 4,030
SKD61, DAC, DHA
(1.2344,1 .2379) JC8118 190 0.25 ~32 650 2,500 190 0.25 ~32 650 2,910
42-52HRC 250 0.20 ~32 580 1,670 250 0.20 ~32 580 1,950
Hardened die steel ~130 0.20 ~32 640 1,150 ~130 0.20 ~32 640 1,340
SKD11, SLD,DC11
(1.2344, 1.2379) DH102 190 0.15 ~32 580 940 190 0.15 ~32 580 1,100
55-62HRC 250 0.10 ~32 510 740 250 0.10 ~32 510 860
ℓ: Overhung length, ap: Axial depth of cut, ae: Radial depth of cut, n: Spindle speed, Vf: Feed speed
■ NOTE
1) The cutting parameters to be adjusted according to the machine rigidity or work rigidity.
2) In case chatter occurrs, recommend to reduce depth of cut or spindle speed with keeping feed per tooth.
3) If machine does not have enough power, recommend to reduce depth of cut first and reduce spindle speed and
feed speed.
4) Use air blow to flush the chips out. B039