Общий каталог Yamawa 2021 - страница 705
Навигация
 Обший каталог Yamawa 2016 - 2017
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2022 - 2023
 Каталоги Yamawa твердосплавные метчики для закаленной стали
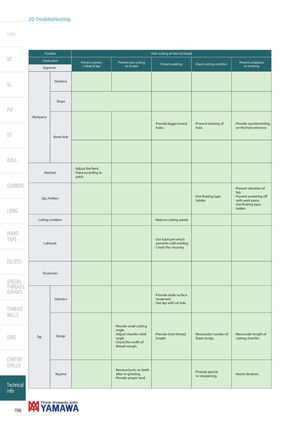
| Troubles Check point Segments | Prevent uneven in feed of tap | O Prevent over cutting on thread | ver-cutting of internal thread Prevent welding | Check cutting condition | Prevent unbalance on entering |
| Hardness | |||||
| Shape | |||||
| Workpiece Bored hole | ∙ Provide bigger bored holes. | ∙ Provent slanting of hole. | ∙ Provide countersinking on the hole entrance. | ||
| Machine | ∙ Adjust the feed. ∙ Feed according to pitch. | ||||
| Jigs, Holders | ∙ Use fl oating type holder. | ∙ Prevent vibration of tap. ∙ Provent centering-off with work piece. ∙ Use fl oating type holder. | |||
| Cutting condition | ∙ Reduce cutting speed. | ||||
| Lubricant | ∙ Use lubricant which prevents cold welding. ∙ Check the viscosity. | ||||
| On process | |||||
| Selection | ∙ Provide oxide surface treatment. ∙ Use tap with oil hole. | ||||
| Tap Design | ∙ Provide small cutting angle. ∙ Adjust chamfer relief angle. ∙ Check the width of thread margin. | ∙ Provide short thread length. | ∙ Reconsider number of fl utes to tap. | ∙ Reconsider length of cutting chamfer. | |
| Regrind | ∙ Remove burrs on teeth after re-grinding. ∙ Provide proper land. | ∙ Provide precise re-sharpening. | ∙ Avoid vibration. |
SP
PO
ST
ROLL
CARBIDE
HAND
EG (STI)
SPECIAL
THREADS,