Каталог SGS инструмент для сверления - страница 5
Навигация
 Каталог SGS высокопроизводительные черновые фрезы
 Каталог SGS высокопроизводительные фрезы для чистовой обработки Multi-carb
 Каталог SGS микроинструмент
 Каталог SGS микро инструмент 2021
 Каталог SGS монолитный инструмент из композитных материалов
 Каталог SGS фрезы для алюминия S-carb
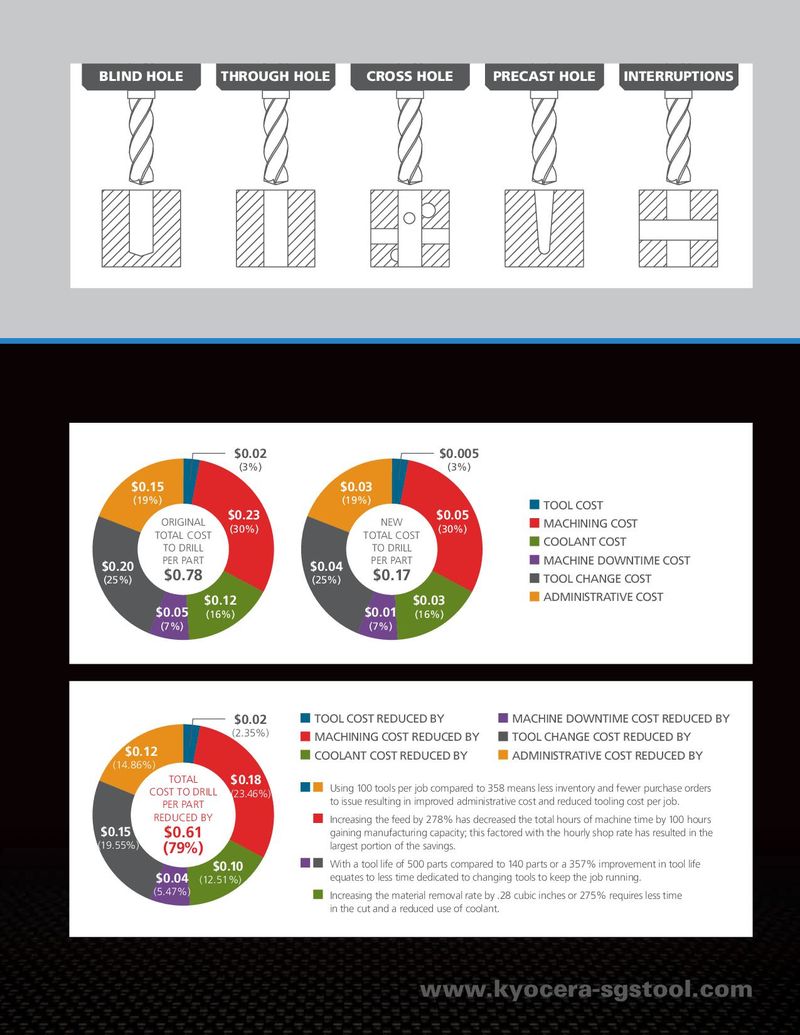
BLIND HOLE THROUGH HOLE CROSS HOLE PRECAST HOLE INTERRUPTIONS
PRECISION. The stability of the double margin design and penetration capability of the point geometry allow the Hi-PerCarb Series 135 Drill to address demanding applications that would normally require reduced operating parameters or a two step process.
PASSION.
| The secondary flute provides a channel for cooling capabilities normally not found in external coolant drills, this | $0.02 | $0.005 | ||
| combined with the Ti-NAMITE A tool coating and the high strength edge design results in increased operating | (3%) | (3%) | ||
| $0.15 | $0.03 | |||
| parameters with additional tool life. |
| (19%) | (19%) | TOOL COST | ||
| $0.23 | $0.05 |
| ORIGINAL | NEW | MACHINING COST | |||
| (30%) | (30%) | ||||
| TOTAL COST | TOTAL COST | ||||
| COOLANT COST | |||||
| ACTUAL CUSTOMER APPLICATION USING A 6MM DRILL IN 17-4 PH STAINLESS STEEL | TO DRILL | TO DRILL | |||
| $0.20 | PER PART | $0.04 | PER PART | MACHINE DOWNTIME COST | |
| HI-PERCARB | $0.78 | $0.17 | |||
| (25%) | (25%) | TOOL CHANGE COST | |||
| COMPETITOR SERIES 135 |
$0.12 $0.03 ADMINISTRATIVE COST
| NUMBER OF PARTS TO PRODUCE | 50000 | 50000 | $0.05 | (16%) $0.01 (16%) |
| SURFACE FEET PER MINUTE (SFM) | 74 | 124 | (7%) | (7%) |
| SPEED IN REVOLUTIONS PER MINUTE (RPM) | 1200 | 2000 | ||
| FEED IN INCHES PER MINUTE (IPM) | 3.6 | 10 | ||
| NUMBER OF PARTS PRODUCED PER TOOL | 140 | 500 | ||
| DEPTH OF HOLE | 0.6800 | 0.6800 | $0.02 | |
| MACHINE DOWNTIME COST REDUCED BY TOOL COST REDUCED BY | ||||
| NUMBER OF NEW TOOLS REQUIRED TO COMPLETE JOB | 358 | 100 | TOOL CHANGE COST REDUCED BY MACHINING COST REDUCED BY (2.35%) | |
| TOTAL HOURS OF MACHINING TIME | 157 | 57 | $0.12 | ADMINISTRATIVE COST REDUCED BY COOLANT COST REDUCED BY |
| (14.86%) | ||||
| TOTAL MACHINING COST | $10,231.48 $3,683.33 | $0.18 | ||
| TOTAL | ||||
| TOOL CHANGE COST | $1,939.17 $541.67 | COST TO DRILL (23.46%) | Using 100 tools per job compared to 358 means less inventory and fewer purchase orders | |
| PER PART | to issue resulting in improved administrative cost and reduced tooling cost per job. | |||
| TOTAL COST | $39,017.07 $8,460.00 | REDUCED BY | Increasing the feed by 278% has decreased the total hours of machine time by 100 hours | |
| COST PER PART | $0.78 | $0.17 | $0.15 $0.61 | gaining manufacturing capacity; this factored with the hourly shop rate has resulted in the |
| (19.55%) (79%) | largest portion of the savings. | |||
| MATERIAL REMOVAL RATE (IN3 / MIN) – DRILLING | 0.16 | 0.44 | ||
| $0.10 With a tool life of 500 parts compared to 140 parts or a 357% improvement in tool life | ||||
| CUTTING TIME PER PART – MINUTES | 0.19 0.07 | $0.04 | (12.51%) equates to less time dedicated to changing tools to keep the job running. | |
| SAVINGS PER PART – DOLLARS | 0 | $0.61 | (5.47%) | Increasing the material removal rate by .28 cubic inches or 275% requires less time |
| in the cut and a reduced use of coolant. | ||||
| TOTAL COST SAVINGS / JOB – PERCENTAGE | 0 | 78.32% | ||
| TOTAL COST SAVINGS / JOB – DOLLARS | 0 | $30,557.07 |