Общий каталог Yamawa 2021 - страница 720
Навигация
 Обший каталог Yamawa 2016 - 2017
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2022 - 2023
 Каталоги Yamawa твердосплавные метчики для закаленной стали
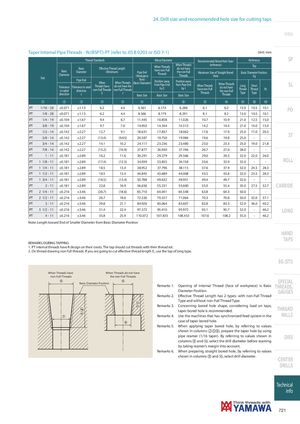
Taper Internal Pipe Threads - Rc(BSPT)-PT (refer to JIS B 0203 or ISO 7-1) Unit: mm
SP
| Size | Basic Diameter | Threa Basic Diameter Pipe End | d Standards Eff ective Thr (Mini When | f ead Length mum) ( When Threads | Pipe End (Workpiece Face) Basic Diamater) | Minor Diameter When Threads have non-Full Threads Position away from Pipe End | When Threads do not have the non-Full Threads Position away from Pipe End | Recommended B (refer Maximum Size o Ho When Threads | ored Hole Sizes ence) f Straight Bored le When Threads | Basic D Lon | Reference Tap iameter P ℓg Short | osition. | |
| Tolerance in radial T | olerance in axial direction | Threads have non-Full Threads | do not have the non-Full Threads | by ℓ | by t | have non-Full | do not have the non-Full | g Thread | Thread | Rc | |||
| direction | c | ℓ | t | Basic Size | Basic Size | Basic Size | Threads | Threads | Type | Type | |||
| 1 | 2 | 3 | 4 | 5 | 6 | 7 | 8 | 9 | 0 | ! | " | £ | |
| PT | 1/16 - 28 | ±0.071 | ±1.13 | 6.2 | 4.4 | 6.561 | 6.174 | 6.286 | 6.1 | 6.2 | 13.0 | 10.5 | 10.1 |
| PT | 1/8 - 28 | ±0.071 | ±1.13 | 6.2 | 4.4 | 8.566 | 8.179 | 8.291 | 8.1 | 8.2 | 13.0 | 10.5 | 10.1 |
| PT | 1/4 - 19 | ±0.104 | ±1.67 | 9.4 | 6.7 | 11.445 | 10.858 | 11.026 | 10.7 | 10.9 | 21.0 | 12.5 | 15.0 |
| PT | 3/8 - 19 | ±0.104 | ±1.67 | 9.7 | 7.0 | 14.950 | 14.344 | 14.513 | 14.2 | 14.4 | 21.0 | 14.0 | 15.4 |
| PT | 1/2 - 14 | ±0.142 | ±2.27 | 12.7 | 9.1 | 18.631 | 17.837 | 18.062 | 17.6 | 17.9 | 25.0 | 17.0 | 20.5 |
| PT | 5/8 - 14 | ±0.142 | ±2.27 | (13.4) | (9.65) | 20.587 | 19.750 | 19.984 | 19.6 | 19.8 | 25.0 | - | - |
| PT | 3/4 - 14 | ±0.142 | ±2.27 | 14.1 | 10.2 | 24.117 | 23.236 | 23.480 | 23.0 | 23.3 | 25.0 | 19.0 | 21.8 |
| PT | 7/8 - 14 | ±0.142 | ±2.27 | (15.2) | (10.9) | 27.877 | 26.930 | 27.196 | 26.7 | 27.0 | 28.0 | - | - |
| PT | 1 - 11 | ±0.181 | ±2.89 | 16.2 | 11.6 | 30.291 | 29.279 | 29.566 | 29.0 | 29.3 | 32.0 | 22.0 | 26.0 |
| PT | 1 1/8 - 11 | ±0.181 | ±2.89 | (17.4) | (12.5) | 34.939 | 33.855 | 34.158 | 33.6 | 33.9 | 32.0 | - | - |
| PT | 1 1/4 - 11 | ±0.181 | ±2.89 | 18.5 | 13.4 | 38.952 | 37.796 | 38.115 | 37.6 | 37.9 | 32.0 | 24.5 | 28.3 |
| PT | 1 1/2 - 11 | ±0.181 | ±2.89 | 18.5 | 13.4 | 44.845 | 43.689 | 44.008 | 43.5 | 43.8 | 32.0 | 25.5 | 28.3 |
| PT | 1 3/4 - 11 | ±0.181 | ±2.89 | (18.5) | (13.4) | 50.788 | 49.632 | 49.951 | 49.4 | 49.7 | 32.0 | - | - |
| PT | 2 - 11 | ±0.181 | ±2.89 | 22.8 | 16.9 | 56.656 | 55.231 | 55.600 | 55.0 | 55.4 | 35.0 | 27.5 | 32.7 |
| PT | 2 1/4 - 11 | ±0.216 | ±3.46 | (26.7) | (18.6) | 65.710 | 64.041 | 64.548 | 63.8 | 64.3 | 50.0 | - | - |
| PT | 2 1/2 - 11 | ±0.216 | ±3.46 | 26.7 | 18.6 | 72.226 | 70.557 | 71.064 | 70.3 | 70.8 | 50.0 | 32.0 | 37.1 |
| PT | 3 - 11 | ±0.216 | ±3.46 | 29.8 | 21.1 | 84.926 | 83.064 | 83.607 | 82.8 | 83.3 | 52.0 | 36.0 | 40.2 |
| PT | 3 1/2 - 11 | ±0.216 | ±3.46 | 31.4 | 22.4 | 97.372 | 95.410 | 95.972 | 95.1 | 95.7 | 52.0 | - | 46.2 |
| PT | 4 - 11 | ±0.216 | ±3.46 | 35.8 | 25.9 | 110.072 | 107.835 | 108.453 | 107.6 | 108.2 | 55.0 | - | 46.2 |
ROLL
Note: Length toward End of Smaller Diameter from Basic Diameter Position
REMARKS DURING TAPPING 1. PT internal threads have R design on their crests. The tap should cut threads with their thread rot. 2. On thread drawing non-full threads. If you are going to cut effective thread length ℓ., use the tap of long type.
When Threads have When Threads do not have non-Full Threads the non-Full Threads Basic Diameter Position
HAND
TAPS
EG (STI)
SPECIAL
| Remarks 1. | Opening of Internal Thread (Face of workpiece) is Basic Diameter Position. |
| Remarks 2. | Effective Thread Length has 2 types: with non-Full Thread Type and without non-Full Thread Type. |
| Remarks 3. | Concerning bored hole shape, considering load on taps, taper bored hole is recommended. |
| Remarks 4. | Use the machines that has synchronized feed system in the case of taper bored hole. |
| Remarks 5. | When applying taper bored hole, by referring to values shown in columns258, prepare the taper hole by using pipe reamer (1/16 taper). By referring to values shown in columns9and0, select the drill diameter before reaming by taking reamer’s margin into account. |
| Remarks 6. | When preparing straight bored hole, by referring to values shown in columns9and0, select drill diameter. |