Общий каталог Yamawa 2021 - страница 639
Навигация
 Обший каталог Yamawa 2016 - 2017
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2022 - 2023
 Каталоги Yamawa твердосплавные метчики для закаленной стали
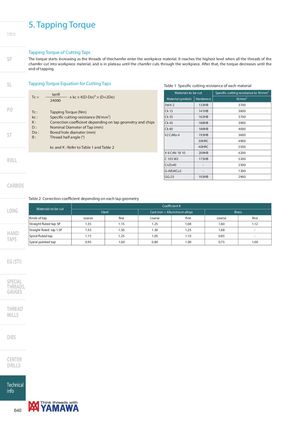
Tapping Torque of Cutting Taps
SP The torque starts increasing as the threads of thechamfer enter the workpiece material. It reaches the highest level when all the threads of the chamfer cut into workpiece material, and is in plateau until the chamfer cuts through the workpiece. After that, the torque decreases until the end of tapping.
SL Tapping Torque Equation for Cutting Taps
Table 1 Specifi c cutting resistance of each material
| tanθ ² | Materials to b | e cut | Specifi c cutting resistance kc N/mm 2 | |
| Tc = | . x kc × K(D-Do) × (D+2Do) 24000 | Material symbols | Hardeness | N/mm 2 |
| 5t44-2 | 133HB | 3700 | ||
| Tc : | Tapping Torque (Nm) | Ck 15 | 141HB | 3600 |
| kc : | Specifi c cutting resistance (N/mm 2) | Ck 35 | 162HB | 3700 |
| K : | Correction coeffi cient depending on tap geometry and chips | Ck 45 | 188HB | 3900 |
| D : | Nominal Diameter of Tap (mm) | Ck 60 | 188HB | 4000 |
| Do : θ : | Bored hole diameter (mm) Thread half anle (°) | 42 CrMo 4 | 193HB | 3600 |
| g | 30HRC | 4900 | ||
| kc and K : Refer to Table 1 and Table 2 | 40HRC | 5500 | ||
| X 6 CrNi 18 10 | 209HB | 4200 | ||
| C 105 W2 | 175HB | 5300 | ||
| CnZn40 | - | 2300 | ||
| G-AISi8Cu3 | - | 1300 | ||
| GG-25 | 193HB | 2900 |
PO
CARBIDE
Table 2 Correction coeffi cient depending on each tap geometry
| Materials to be cut | Ste | el | Coeffi c Cast iron + Allu | fi ient K minium alloys | Bra | ss |
| Kinds of tap | coarse | fi ne | coarse | fi ne | coarse | fi ne |
| Straight fl uted tap 5P | 1.35 | 1.15 | 1.25 | 1.08 | 1.60 | 1.12 |
| Straight fl uted tap 1.5P | 1.43 | 1.50 | 1.30 | 1.25 | 1.68 | - |
| Spiral fl uted tap | 1.15 | 1.25 | 1.05 | 1.10 | 0.85 | - |
| Spiral pointed tap | 0.95 | 1.00 | 0.80 | 1.00 | 0.75 | 1.00 |
EG (STI)
SPECIAL
THREADS,