Общий каталог Yamawa 2021 - страница 637
Навигация
 Обший каталог Yamawa 2016 - 2017
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2022 - 2023
 Каталоги Yamawa твердосплавные метчики для закаленной стали
3. Flutes
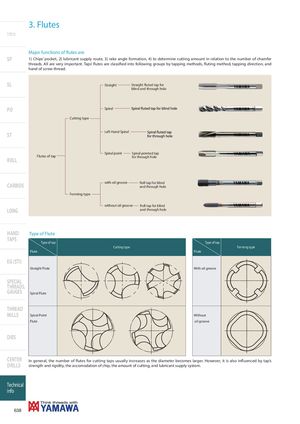
Major functions of flutes are
SP 1) Chips’ pocket, 2) lubricant supply route, 3) rake angle formation, 4) to determine cutting amount in relation to the number of chamfer threads. All are very important. Taps’ fl utes are classifi ed into following groups by tapping methods, fl uting method, tapping direction, and hand of screw thread.
SL Straight Straight fluted tap for
blind and through hole
PO Spiral Cutting type ST Left Hand Spiral
Spiral point Spiral pointed tap Flutes of tap for through hole
ROLL
CARBIDE with oil groove Roll tap for blind
and through hole Forming type
without oil groove Roll tap for blind LONG and through hole
HAND Type of Flute
TAPS
Type of tap Type of tap Cutting type Forming type Flute Flute
EG (STI)
Straight Flute With oil groove
SPECIAL
THREADS,
GAUGES
Spiral Flute
THREAD
MILLS Spiral Point Without
Flute oil groove
DIES
CENTER
In general, the number of fl utes for cutting taps usually increases as the diameter becomes larger. However, it is also infl uenced by tap’s DRILLS strength and rigidity, the accomodation of chip, the amount of cutting, and lubricant supply system.