Общий каталог Yamawa 2021 - страница 629
Навигация
 Обший каталог Yamawa 2016 - 2017
 Краткое руководство Yamawa по каталогам
 Общий каталог Yamawa 2022 - 2023
 Каталоги Yamawa твердосплавные метчики для закаленной стали
Intro AUPES
SP
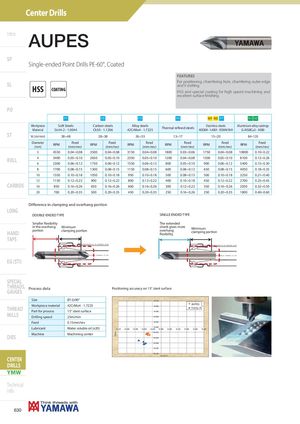
Single-ended Point Drills PE-60°, Coated
SL
HSS
COATING
PO
FEATURES
For positioning, chamfering hole, chamfering outer edge
and V slotting.
HSS and special coating for high speed machining and
excellent surface fi nishing.
| P1 | P2 | P3 | P4 | M1 | M2 P7 | N | 1 N2 | |||||
| Workpiece Material | Soft St.44-2 | Steels - 1.0044 | Carbo Ck50 | n steels - 1.1206 | Alloy 42CrMo | steels 4 - 1.7225 | Thermal ri | efi ned steels | Stainle AISI304 - 1.43 | ss steels 01 - X5XrNi18-9 | Aluminium G-AISi8 | alloy castings Cu3 - A380 |
| Vc (m/min) | 38 | ÷48 | 28 | ÷38 | 26 | ÷33 | 13 | ÷17 | 13 | ÷20 | 84 | ÷120 |
| Diameter (mm) | RPM | Feed (mm/rev) | RPM | Feed (mm/rev) | RPM | Feed (mm/rev) | RPM | Feed (mm/rev) | RPM | Feed (mm/rev) | RPM | Feed (mm/rev) |
| 3 | 4550 | 0.04÷0.08 | 3500 | 0.04÷0.08 | 3150 | 0.04÷0.08 | 1800 | 0.03÷0.06 | 1750 | 0.04÷0.08 | 10800 | 0.10÷0.22 |
| 4 | 3400 | 0.05÷0.10 | 2650 | 0.05÷0.10 | 2350 | 0.05÷0.10 | 1200 | 0.04÷0.08 | 1300 | 0.05÷0.10 | 8100 | 0.12÷0.26 |
| 6 | 2300 | 0.06÷0.12 | 1750 | 0.06÷0.12 | 1550 | 0.06÷0.12 | 800 | 0.05÷0.10 | 900 | 0.06÷0.12 | 5400 | 0.15÷0.30 |
| 8 | 1700 | 0.08÷0.15 | 1300 | 0.08÷0.15 | 1150 | 0.08÷0.15 | 600 | 0.06÷0.12 | 650 | 0.08÷0.15 | 4050 | YMW-AUPES 0.18÷0.35 |
| 10 | 1350 | 0.10÷0.18 | 1050 | 0.10÷0.18 | 950 | 0.10÷0.18 | 500 | 0.08÷0.15 | 500 | 0.10÷0.18 | 3250 | 0.21÷0.40 |
| 12 | 1150 | 0.12÷0.22 | 900 | 0.12÷0.22 | 800 | 0.12÷0.22 | 400 | 0.10÷0.18 | 450 | 0.12÷0.22 | 2700 | 0.25÷0.45 |
| 16 | 850 | 0.16÷0.26 | 650 | 0.16÷0.26 | 600 | 0.16÷0.26 | 300 | 0.12÷0.22 | 350 | 0.16÷0.26 | 2050 | 0.32÷0.50 |
| 20 | 700 | 0.20÷0.35 | 500 | 0.20÷0.35 | 450 | 0.20÷0.35 | 250 | 0.16÷0.26 | 250 | 0.20÷0.35 | 1800 | 0.40÷0.60 |
ST
CARBIDE
LONG
HAND
TAPS
Diff erence in clamping and overhang portion
DOUBLE-ENDED TYPE SINGLE-ENDED TYPE Smaller fl exibility The extended
| in the overhang | Minimum | shank gives more | Minimum |
| portion | clamping portion | overhang |
clamping portion fl exibility
EG (STI)
SPECIAL
THREADS,
| GAUGES | Process data | Positioning accuracy on 15° slant surface | |
| Size | Ø12x90° |
| Workpiece material | 42CrMo4 - 1.7225 | AUPEQ | |
| THREAD | Comp. A | ||
| Part for process | 15° slant surface | ||
| MILLS | |||
| Drilling speed | 25m/min | ||
| Feed | 0.15mm/rev | ||
| Lubricant | Water soluble oil (x20) | ||
| DIES | Machine | Machining center |