Каталог Winstar фрезерование - страница 234
Навигация
 Каталог Winstar монолитный инструмент 2020
 Каталог Winstar сверление
 Основной каталог Winstar 2021
 Каталог Carbidex сменные пластины 2020
 Каталог Winstar инструмент со сменными пластинами 2020
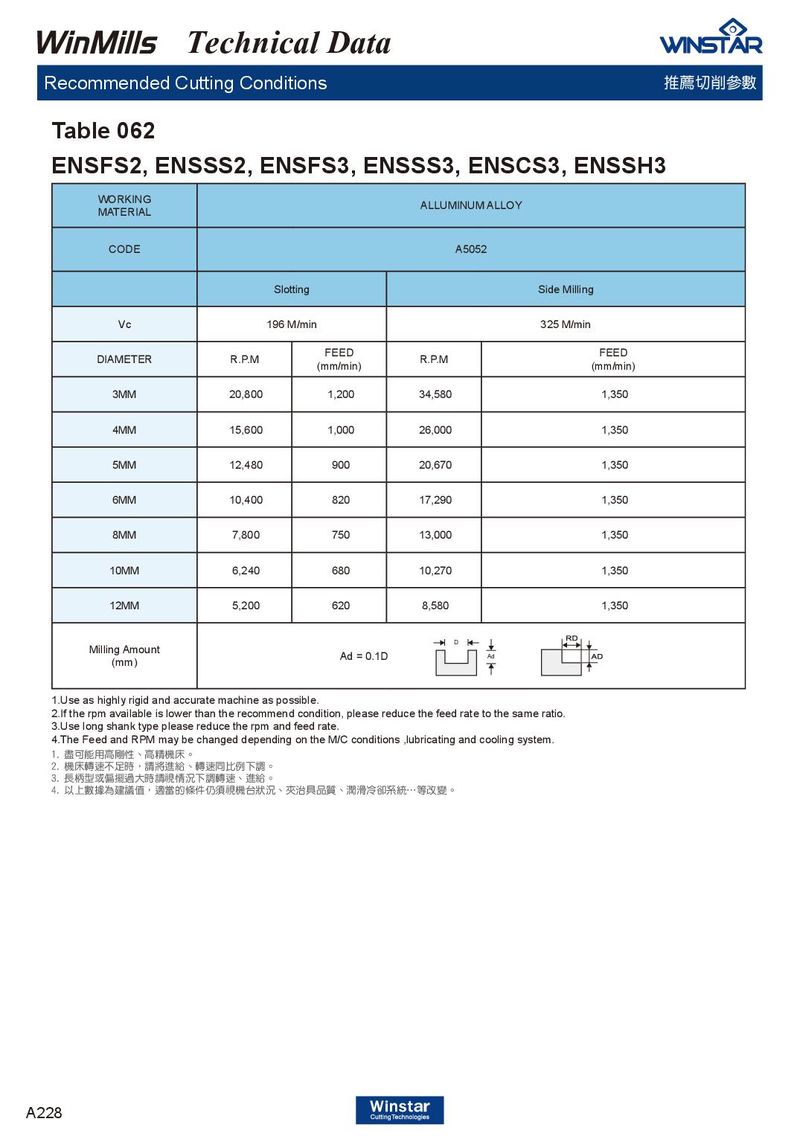
Table 062
ENSFS2, ENSSS2, ENSFS3, ENSSS3, ENSCS3, ENSSH3
| WORKING MATERIAL | ALLUMINUM | ALLOY | ||
| CODE | A505 | 2 | ||
| Slot | ting | Side Milling | ||
| Vc | 196 | M/min | 325 M/min | |
| DIAMETER | R.P.M | FEED (mm/min) | R.P.M | FEED (mm/min) |
| 3MM | 20,800 | 1,200 | 34,580 | 1,350 |
| 4MM | 15,600 | 1,000 | 26,000 | 1,350 |
| 5MM | 12,480 | 900 | 20,670 | 1,350 |
| 6MM | 10,400 | 820 | 17,290 | 1,350 |
| 8MM | 7,800 | 750 | 13,000 | 1,350 |
| 10MM | 6,240 | 680 | 10,270 | 1,350 |
| 12MM | 5,200 | 620 | 8,580 | 1,350 |
| Milling Amount (mm) | Ad = 0.1D | D | Ad |
1.Use as highly rigid and accurate machine as possible. 2.If the rpm available is lower than the recommend condition, please reduce the feed rate to the same ratio. 3.Use long shank type please reduce the rpm and feed rate. 4.The Feed and RPM may be changed depending on the M/C conditions ,lubricating and cooling system. 1. 盡可能用高剛性、高精機床。 2. 機床轉速不足時,請將進給、轉速同比例下調。 3. 長柄型或偏擺過大時請視情況下調轉速、進給。 4. 以上數據為建議值,適當的條件仍須視機台狀況、夾治具品質、潤滑冷卻系統…等改變。