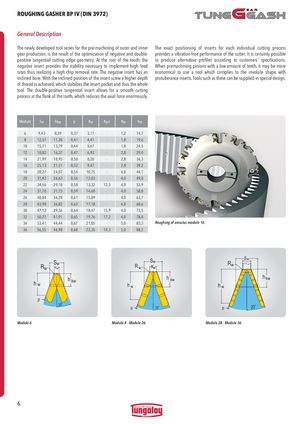
| The newly developed tool series for the pre-machining of outer and inner | The exact positioning of inserts for each individual cutting process |
| gear production, is the result of the optimization of negative and double- | provides a vibration-free performance of the cutter. It is certainly possible |
| positive tangential cutting edge geometry. At the root of the tooth, the | to produce alternative profiles according to customers' specifications. |
| negative insert provides the stability necessary to implement high feed | When premachining pinions with a low amount of teeth, it may be more |
| rates thus realizing a high chip removal rate. The negative insert has an | economical to use a tool which complies to the involute shape with |
| inclined bore. With the inclined position of the insert screw a higher depth | protuberance inserts. Tools such as these can be supplied in special design. |
of thread is achieved, which stabilzes the insert pocket and thus the whole tool. The double-positive tangential insert allows for a smooth cutting process at the flank of the tooth, which reduces the axial force enormously.
| Module | Sw | hkw | p | Kw | Kw1 | Rw | hw |
| 6 | 9,43 | 8,59 | 0,37 | 3,17 | - | 1,2 | 14,7 |
| 8 | 12,57 | 11,20 | 0,41 | 4,41 | - | 1,8 | 19,6 |
| 10 | 15,71 | 13,79 | 0,44 | 5,67 | - | 1,8 | 24,5 |
| 12 | 18,82 | 16,37 | 0,47 | 6,93 | - | 2,8 | 29,4 |
| 14 | 21,99 | 18,95 | 0,50 | 8,20 | - | 2,8 | 34,3 |
| 16 | 25,13 | 21,51 | 0,52 | 9,47 | - | 2,8 | 39,2 |
| 18 | 28,27 | 24,07 | 0,54 | 10,75 | - | 4,0 | 44,1 |
| 20 | 31,42 | 26,63 | 0,56 | 12,03 | - | 4,0 | 49,0 |
| 22 | 34,56 | 29,18 | 0,58 | 13,32 | 12,3 | 4,0 | 53,9 |
| 24 | 37,70 | 31,73 | 0,59 | 14,60 | - | 4,0 | 58,8 |
| 26 | 40,84 | 34,28 | 0,61 | 15,89 | - | 4,0 | 63,7 |
| 28 | 43,98 | 36,82 | 0,62 | 17,18 | - | 4,0 | 68,6 |
| 30 | 47,12 | 39,36 | 0,64 | 18,47 | 15,9 | 4,0 | 73,5 |
| 32 | 50,27 | 41,91 | 0,65 | 19,76 | 17,2 | 4,0 | 78,4 |
| 34 | 53,41 | 44,44 | 0,67 | 21,05 | - | 5,0 | 83,3 |
| 36 | 56,55 | 46,98 | 0,68 | 22,35 | 19,3 | 5,0 | 88,2 |
S Sw
Module 6 Module 8 - Module 26 Module 28 - Module 36
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy инструмент для автоматов швейцарского типа
 Каталог Tungaloy глубокое сверление 2
 Каталог Tungaloy глубокое сверление 1
 Брошюра Tungaloy новая продукция