Каталог Tungaloy глубокое сверление 2 - страница 21
Навигация
 Каталог Tungaloy инструмент для автоматов швейцарского типа
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy зубофрезерование
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy глубокое сверление 1
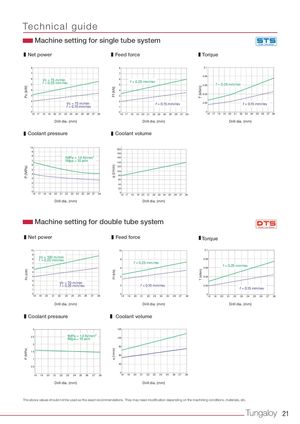
Technical guide
Machine setting for single tube system
| Net power | Feed force | Torque |
| 8 | 8 | 0.1 |
| 7 | 7 | |
| 0.08 | ||
| 6 | Vc = 75 m/min 6 | f |
| f = 0.25 mm/rev | f = 0.25 mm/rev | |
| 5 | 5 | = 0.25 mm/rev |
| 0.06 | ||
| 4 | 4 | |
| 0.04 | ||
| 3 | 3 | |
| 2 | V 2 | f |
| c = 75 m/min | f = 0.15 mm/rev = 0.15 mm/rev 0.02 | |
| f = 0.15 mm/rev | ||
| 1 | 1 | |
| 0 | 0 | 0 |
16 17 18 19 20 21 22 23 24 25 26 27 28 16 17 18 19 20 21 22 23 24 25 26 27 28 16 17 18 19 20 21 22 23 24 25 26 27 28
Drill dia. (mm) Drill dia. (mm) Drill dia. (mm)
Coolant pressure Coolant volume
10 200 9 180 8 1MPa = 1.0 N/mm2 160 7 1Mpa ≈ 10 atm 140 6 120 5 100 4 80 3 60 2 40 1 20 0 0 16 17 18 19 20 21 22 23 24 25 26 27 28 16 17 18 19 20 21 22 23 24 25 26 27 28
Drill dia. (mm) Drill dia. (mm)
Machine setting for double tube system
| Net power | Feed force | Torque |
| 10 | 10 | 0.1 |
| 9 | V | |
| f c = 100 m/min | ||
| 8 | = 0.25 mm/rev 8 | 0.08 |
| f = 0.25 mm/rev | ||
| 7 | f | |
| = 0.25 mm/rev | ||
| 6 | 6 | 0.06 |
| 5 | ||
| 4 | 4 | 0.04 |
| 3 | V | |
| f c = 70 m/min | f | |
| 2 | = 0.25 mm/rev 2 | = 0.15 mm/rev 0.02 |
| f = 0.15 mm/rev | ||
| 1 | ||
| 0 | 0 | 0 |
| 18 19 20 21 22 23 24 25 26 27 28 | 18 19 20 21 22 23 24 25 26 27 28 | 18 19 20 21 22 23 24 25 26 27 28 |
| Drill dia. (mm) | Drill dia. (mm) | Drill dia. (mm) | ||||
| Coolant pressure | Coolant volume | |||||
| 3 | 120 | |||||
| 1MPa = 1.0 N/mm 2 | ||||||
| 2.5 | 100 |
1Mpa ≈ 10 atm 2 80 1.5
60 1 40 0.5 0
18 19 20 21 22 23 24 25 26 27 28 18 19 20 21 22 23 24 25 26 27 28
Drill dia. (mm) Drill dia. (mm)
The above values should not be used as the exact recommendations. They may need modification depending on the machining conditions, materials, etc.