Каталог Tungaloy глубокое сверление 1 - страница 57
Навигация
 Брошюра Tungaloy новая продукция
 Каталог Tungaloy инструмент для автоматов швейцарского типа
 Каталог Tungaloy глубокое сверление 2
 Общий каталог Tungaloy 2020 - 2021
 Каталог Tungaloy зубофрезерование
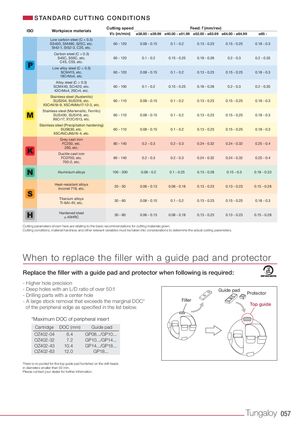
| ISO | Workpiece materials | Vc (m/min) Cutting speed | ø38.00 - ø39.99 | ø40.00 - ø51.99 | ø52.00 - ø63.99 Feed:f (mm/rev | ø64.00 - ø84.99 ) | ø85 - |
| Low carbon steel (C < 0.3) SS400, SM490, S25C, etc. St42-1, St52-3, C25, etc. | 60 - 120 | 0.08 - 0.15 | 0.1 - 0.2 | 0.13 - 0.23 | 0.15 - 0.25 | 0.18 - 0.3 | |
| Carbon steel (C > 0.3) S45C, S55C, etc. C45, C55, etc. | 60 - 120 | 0.1 - 0.2 | 0.15 - 0.25 | 0.18 - 0.28 | 0.2 - 0.3 | 0.2 - 0.35 | |
| Low alloy steel (C < 0.3) SCM415, etc. 18CrMo4, etc. | 60 - 120 | 0.08 - 0.15 | 0.1 - 0.2 | 0.13 - 0.23 | 0.15 - 0.25 | 0.18 - 0.3 | |
| Alloy steel (C > 0.3) SCM440, SCr420, etc. 42CrMo4, 20Cr4, etc. | 60 - 100 | 0.1 - 0.2 | 0.15 - 0.25 | 0.18 - 0.28 | 0.2 - 0.3 | 0.2 - 0.35 | |
| Stainless steel (Austenitic) SUS304, SUS316, etc. X5CrNi18-9, X5CrNiMo17-12-3, etc. | 60 - 110 | 0.08 - 0.15 | 0.1 - 0.2 | 0.13 - 0.23 | 0.15 - 0.25 | 0.18 - 0.3 | |
| Stainless steel (Martensitic, Ferritic) SUS430, SUS416, etc. X6Cr17, X12CrS13, etc. | 60 - 110 | 0.08 - 0.15 | 0.1 - 0.2 | 0.13 - 0.23 | 0.15 - 0.25 | 0.18 - 0.3 | |
| Stainless steel (Precipitation hardening) SUS630, etc. X5CrNiCuNb16-4, etc. | 60 - 110 | 0.08 - 0.15 | 0.1 - 0.2 | 0.13 - 0.23 | 0.15 - 0.25 | 0.18 - 0.3 | |
| Grey cast iron FC250, etc. | 80 - 140 | 0.2 - 0.3 | 0.2 - 0.3 | 0.24 - 0.32 | 0.24 - 0.32 | 0.25 - 0.4 | |
| 250, etc. | |||||||
| Ductile cast iron FCD700, etc. 700-2, etc. | 80 - 140 | 0.2 - 0.3 | 0.2 - 0.3 | 0.24 - 0.32 | 0.24 - 0.32 | 0.25 - 0.4 | |
| Aluminium alloys | 100 - 200 | 0.08 - 0.2 | 0.1 - 0.25 | 0.13 - 0.28 | 0.15 - 0.3 | 0.18 - 0.33 | |
| Heat-resistant alloys Inconel 718, etc. | 20 - 50 | 0.06 - 0.13 | 0.08 - 0.18 | 0.13 - 0.23 | 0.13 - 0.23 | 0.15 - 0.28 | |
| Titanium alloys Ti-6Al-4V, etc. | 30 - 60 | 0.08 - 0.15 | 0.1 - 0.2 | 0.13 - 0.23 | 0.15 - 0.25 | 0.18 - 0.3 | |
| Hardened steel ≥ 40HRC | 30 - 80 | 0.06 - 0.13 | 0.08 - 0.18 | 0.13 - 0.23 | 0.13 - 0.23 | 0.15 - 0.28 |
Cutting parameters shown here are relating to the basic recommendations for cutting materials given. Cutting conditions, material hardness and other relevant variables must be taken into considerations to determine the actual cutting parameters.
When to replace the filler with a guide pad and protector
Replace the fi ller with a guide pad and protector when following is required:
- Higher hole precision
- Deep holes with an L/D ratio of over 50:1 Guide pad
- Drilling parts with a center hole Protector
- A large stock removal that exceeds the marginal DOC* Filler
Top guide
of the peripheral edge as specified in the list below.
*Maximum DOC of peripheral insert
| Cartridge | DOC (mm) | Guide pad |
| OZ402-04 | 6.4 | GP08.../GP10... |
| OZ402-32 | 7.2 | GP10.../GP14... |
| OZ402-43 | 10.4 | GP14.../GP18... |
| OZ402-63 | 12.0 | GP18... |
There is no pocket for the top guide pad furnished on the drill heads in diameters smaller than 92 mm. Please contact your dealer for further information.